
PWR-330 · Lesson 10 of 12 · 23 min
Upset conditions and emergency response
▶ Video coming soon A video version of this lesson is on the way.
In the space of a few weeks that autumn, Cantwell had had a utility power failure, a flame failure, a drum level transmitter reading high from a leaking reference leg, and a furnace tube leak found by a careful engineer doing arithmetic at half past one in the morning. Each had been handled well, and each was written up. Grazyna put the four reports in front of Okonkwo and asked him to find what they had in common.
He found it in the second paragraph of each. Someone had noticed that something was not as it should be, had believed it rather than explaining it away, and had acted before the plant forced the decision. "That is the whole of emergency response," Grazyna said. "The trips protect the boiler. People protect the plant, by seeing early and acting in the right order. The order is what you learn now, so that you don't have to work it out at three in the morning."
This lesson covers the main upset conditions in boiler plants, how each is recognized, and the actions to take: low and high drum level, tube failures, flame failure and furnace explosions, loss of fans, feed pumps, fuel and power, safety valve problems, and steam and gas leaks. It closes with emergency procedures, drills and reporting.
Principles
Every emergency procedure in a boiler plant rests on the same order of priorities: protect people first, then prevent the situation from getting worse, then protect equipment, then restore service. In practice that means:
- Let the protection work. Trips and safety valves act faster than any person. An operator's first job in an upset is usually to confirm that they have acted, and to act by hand if they have not.
- Believe the indications, and check them. A reading that looks impossible may be an instrument fault, but it is treated as real until another independent indication shows otherwise.
- Act in the planned order, from the written emergency procedure, not from memory under stress.
- Communicate: tell the shift engineer or supervisor at once, call for help early, and keep the control room informed.
- Record what happened and when, while it is fresh.
Most serious boiler accidents have a history of earlier warnings that were noticed and not acted on: a low water cutoff that was slow on its last test, a gauge glass that was hard to read, a burner that puffed on light-off. Upsets are much easier to handle when they are small.
Low drum level
Low water is the most dangerous condition in a drum boiler. If the water falls below the top of the heated tubes, they overheat, lose strength and can rupture, and in a firetube boiler the furnace crown can collapse. Causes include: feed pump failure, a feedwater control valve failing closed, a level controller fault, a level transmitter reading falsely high (as boiler 1's did on September 27 when its reference leg leaked), a tube leak, a blowdown valve left open, or an operator misreading shrink after a load decrease.
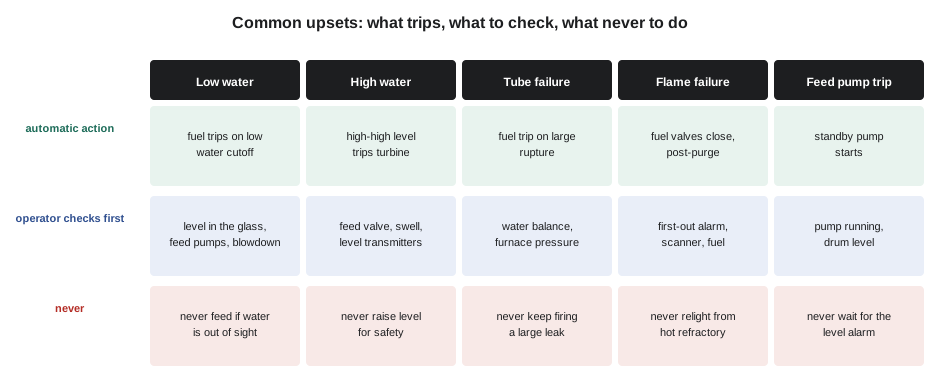
The low water cutoff and the drum level trip should shut off the fuel before the water reaches a dangerous level. The operator's actions on a low level alarm are to verify the level in the gauge glass or the independent level indicators, find and correct the cause if it is quickly found, such as starting the standby feed pump, opening the feed bypass or closing an open blowdown, and to trip the boiler if the level continues to fall or cannot be confirmed.
If the water has gone out of sight in the gauge glass, the rule is firm: shut off the fuel and do not add feedwater until the boiler has cooled and the extent of any overheating is known. Feeding cold water onto overheated tubes or a hot furnace crown can cause sudden thermal stresses and a violent generation of steam that ruptures the weakened metal. The fans may be kept running to cool the furnace, steam is taken off gradually to reduce pressure, and the boiler is inspected before it is refilled. The exception is when the water is known still to be in the drum, for example when the level has been seen falling in the glass and is still visible: then normal feeding is restored.
Worked problem
How long the water lasts
PWR-220 found that a Cantwell boiler holds about 42 ft³ of water between normal level and the low water cutoff, about 2,310 lb at drum conditions, giving about 5.6 minutes at 24,950 lb/h with no feed. A utility drum at 2,538 psia (saturated water density 34.6 lb/ft³) holds about 350 ft³ between normal level and its low level trip, and generates 3,170,000 lb/h of steam. How long would its water last with no feed?
Show solution
- \[m = 350 \times 34.6 = 12{,}100 \text{ lb}, \qquad t = \frac{12{,}100}{3{,}170{,}000 \div 3{,}600} = \frac{12{,}100}{881} = 14 \text{ s}\]
Answer: About 14 seconds. A large drum boiler relies entirely on automatic feedwater control and automatic trips: no operator could recognize and respond to a feed pump trip in that time. At Cantwell, an operator has a few minutes, which is why Cantwell's procedures expect the operator to start the standby pump by hand if it fails to start automatically, and a utility's procedures do not.
High drum level
High water is less spectacular but can be as damaging downstream. Water carried over from a flooded drum goes to the superheater, where it deposits its solids, and to the turbine, where slugs of water can break blades, damage thrust bearings and crack hot casings, the hazard called water induction. On a steam header, slugs of water cause water hammer, which can split pipes and blow out fittings. Causes are the mirror of low level: a feed valve failing open, a level transmitter reading falsely low, operator error, or swell after a sudden load increase.
The response is to reduce or stop the feed, open the continuous and, if necessary, intermittent blowdown to lower the level, and reduce the load change that caused the swell. A high-high level trip shuts off the turbine's steam supply, or trips the boiler, before water can reach the turbine. Steam line drains downstream are opened to clear any water that has passed.
Tube failures
A boiler tube failure releases water or steam into the furnace or gas passes. It is recognized by:
- A rising feedwater flow compared with steam flow, or an unexplained make-up increase: the water balance that Desmond Kirwan used to find boiler 3's leak on November 2, when 373 lb/h of feedwater was not accounted for.
- Furnace pressure rising or fluctuating, a hissing or roaring noise, and steam visible at casing leaks or observation ports.
- Drum level falling or hard to hold, and the feed valve opening further.
- A white plume at the stack, and on large boilers, alarms from an acoustic leak detection system that listens for the noise of escaping steam.
- Rising flue gas moisture and falling stack temperature as water evaporates in the gas stream.
The response depends on the size of the leak. A small leak, like boiler 3's pinhole, allows a planned shutdown: the load is transferred to other boilers, the boiler is shut down normally, cooled, and the leak located and repaired. A large rupture calls for a master fuel trip at once. The feed is usually maintained if the drum level can still be held, because the other tubes still need water, while the pressure is reduced by taking steam off. If the level cannot be held, feed is stopped as for low water. The boiler is then cooled, the furnace ventilated to clear the steam, and the failed tube examined before repair: the cause of a tube failure is always found, as PWR-220 lesson 12 explained, or it will happen again.
On a recovery boiler, as lesson 1 described, a suspected tube leak calls for an immediate stop of black liquor firing and an emergency drain, because water reaching the smelt bed can cause a smelt-water explosion; the general rule of maintaining feed does not apply.
Flame failure and furnace explosions
When a flame scanner loses its flame, the burner management system closes the fuel valves within a few seconds and the furnace is post-purged (lesson 2). The operator's job is to make sure the trip has done its work, read the first-out indication, and find the cause before a restart, within the plant's rule on the number of restart attempts. The boiler 1 lockout of October 20 followed exactly that pattern: the night shift confirmed the safe shutdown, the instrument technician found the cracked scanner lens, it was replaced, the furnace was purged and the burner relit.
A furnace explosion follows when fuel collects without burning and is then ignited: by a delayed ignition on light-off, by relighting from hot refractory or a neighboring burner after a partial flameout, by fuel leaking past a closed safety shutoff valve into an idle furnace, or by a fuel-rich condition that suddenly gets air. Small explosions, called puffs, blow out observation port covers and dust; large ones split casings and kill people. After any puff or explosion, the boiler is shut down, the fuel isolated, and the furnace and casing inspected before it is restarted, and the event is investigated and reported as the jurisdiction requires.
The rules that prevent explosions are all in the burner management system and the procedures: purge before every light-off, light at low fire, keep trials short, never bypass a flame scanner, and never try to relight a burner from the heat of the furnace or a neighboring flame.
Loss of auxiliaries
Boilers depend on auxiliaries that can fail:
- Loss of a forced draft or induced draft fan. On a single-fan boiler, the boiler trips. On a large boiler with two FD and two ID fans, the loss of one fan triggers a runback: the firing rate is reduced automatically to the capacity of the remaining fans, and, on balanced draft, the opposite fan of the pair is often tripped too to keep the furnace pressure balanced.
- Loss of a feed pump. The standby pump should start automatically on low discharge pressure or on the running pump's trip. If it does not, the operator starts it at once. At Cantwell, the backup feed pump driven by the 75 hp steam turbine can supply the drums even during a power failure, as it did on September 20.
- Loss of fuel. A drop in gas supply pressure trips the burners on low gas pressure. Cantwell can switch to fuel oil from its backup tank; the switchover is made by procedure, burner by burner, with the oil system warmed and proved, not in haste on a falling header pressure.
- Loss of electrical power. Fans, pumps and controls stop together. The standby generator and automatic transfer switch restore the essential bus, as they did on September 20, and the boilers are relit in order once power is stable. A utility unit losing its station service power trips, and its turbine is protected by DC emergency oil pumps.
- Loss of instrument air, which can drive control valves and dampers to their failure positions; plants with air-operated controls have standby compressors and receivers sized to give time to respond.
For each of these, the plant's procedures say what happens automatically, what the operator must check, and how service is restored. Grazyna's rule for the Cantwell procedures is that each one begins with the automatic actions, so the operator knows what to expect to see in the first minute, and ends with the reports to make.
Safety valves, steam leaks and gas leaks
A safety valve lifting is not itself an emergency: it is the boiler being protected from overpressure. The operator reduces the firing rate, finds why the pressure rose, a header valve closed or a load lost or a control failure, and watches that the valve reseats at its blowdown pressure. A safety valve that will not reseat keeps venting steam: the boiler is brought down in load and pressure until it seats, and the valve is repaired before the boiler returns to full service. A safety valve that fails to lift when the pressure exceeds its set pressure is a dangerous failure: the firing is cut back at once by hand, the boiler taken off line, and the valve removed for repair and testing. A gagged or isolated safety valve on a boiler in service is never acceptable.
A steam leak in the plant is dangerous because high-pressure steam is invisible near the leak and can cut and scald. A large leak is approached only from a safe distance and isolated by valves remote from it, with the area cleared and barricaded; it is not investigated by walking toward the noise. Superheated steam leaks are the worst, because the steam does not condense into a visible cloud until it is well away from the leak.
A gas leak in the boiler house, recognized by the odorant's smell or a gas detector alarm, calls for an evacuation without operating any electrical switches, shutting off the gas at the emergency shutoff outside the building, calling the gas utility and the fire department, and ventilating only when it is safe. Cantwell's boiler room has gas detectors that alarm in the control room, and the emergency shutdown switch outside the boiler room door that PWR-120 described.
Emergency procedures and drills
Every plant keeps written emergency operating procedures for its credible upsets, posted where they are needed and reviewed after every event and every change to the plant. Good procedures are short and specific: the conditions that call for the procedure, the immediate actions, the follow-up actions, the notifications and the restoration. They are written so that a competent operator new to the plant could follow them, because in an emergency that may be who is on shift.
Procedures are practiced. Plants run drills for their main emergencies, including power failure, flame failure, low water, a steam leak and a gas leak, and for fire, chemical spill and medical emergency, often with the local fire department. Cantwell's fall emergency exercise on October 14, which PWR-110 described, was one; its findings went to the safety committee. Large plants also train on simulators, which can run a whole unit through a tube rupture or a fan trip without risk.
Reporting
Boiler incidents must be reported to the regulator and the insurer. Ohio law requires the owner or user of a boiler to notify the superintendent of industrial compliance immediately when a defect affecting its safety is found, and an accident, explosion or rupture is reported at once to the state's boiler section and to the insurer's inspector, who may need to examine the boiler before it is repaired or operated. Injuries and deaths at work are also reported under OSHA's rules. The scene of a serious accident is left undisturbed except to save life or prevent further harm, and the plant's own investigation follows its incident procedure.
Near misses are reported internally too, because the warnings that precede serious accidents are usually near misses that nobody wrote down.
Okonkwo's answer to Grazyna's question went into his notebook as four words: notice, believe, act, write. She added a fifth under it, in the margin: drill.
Common mistakes
MistakeFeeding water into a boiler whose water has gone out of sight in the glass.
InsteadShut off the fuel, do not feed, let it cool and inspect; cold water on overheated metal can cause a rupture.
MistakeRaising the drum level for safety before a load increase.
InsteadSwell can carry water to the superheater and turbine; keep the level at its normal band.
MistakeRelighting a burner from the heat of the furnace after a flameout.
InsteadPurge and relight through the normal sequence; hot refractory ignition causes explosions.
MistakeWalking toward a steam leak to find it.
InsteadClear the area and isolate it from a safe distance; high-pressure steam is invisible near the leak.
MistakeDismissing an unexplained water imbalance as meter error.
InsteadCheck it: a feedwater flow higher than steam and blowdown together can be a tube leak.
Summary and key terms
- Emergency response protects people first, lets the protection work, believes and checks indications, follows the written order and records events.
- On low water out of sight in the glass, shut off the fuel and do not feed until the boiler has cooled and been inspected.
- High water causes carryover, water hammer and turbine water induction; reduce feed, blow down and trip on high-high level.
- Tube failures show in the water balance, furnace pressure, noise and plume; trip on large ruptures, maintain feed if the level can be held, except on recovery boilers.
- Flame failures trip through the BMS; explosions come from unburned fuel ignited late; purge, light at low fire and never relight from hot refractory.
- Loss of fans, feed, fuel or power has automatic responses and written procedures; defects and accidents are reported to the state and insurer at once.
- Low water cutoff
- A device that shuts off the fuel when the boiler water falls to a set low level.
- Shrink
- A temporary fall in drum level when steam demand falls and bubbles in the risers collapse.
- Swell
- A temporary rise in drum level when steam demand rises or pressure falls and bubbles expand.
- Water induction
- Water entering a steam turbine from the boiler or steam lines, damaging blades, bearings and casings.
- Acoustic leak detection
- Sensors that detect the noise of steam or water escaping from boiler tubes.
- Furnace puff
- A small explosion in a furnace from delayed ignition of accumulated fuel.
- Runback
- An automatic reduction in firing rate to match the capacity of the auxiliaries still in service.
- Emergency operating procedure
- A written procedure giving the immediate and follow-up actions for a specific upset.
Practice problems
Work each problem on paper first, then reveal the answer to check.
A drum holds 2,000 lb of water between normal level and the low water cutoff, and the boiler makes 20,000 lb/h of steam. How long does the water last with no feed?
Show answer
2,000 ÷ 333 lb/min = 6 min.
Steam flow is 22,000 lb/h, blowdown 1,100 lb/h and feedwater flow 23,500 lb/h. What is unaccounted for?
Show answer
23,500 − 23,100 = 400 lb/h, a possible leak.
What should be done if a safety valve fails to lift above its set pressure?
Show answer
Reduce the firing at once, take the boiler off line and remove the valve for repair.
Why are the opposite fans often tripped when one fan trips on a balanced-draft boiler?
Show answer
To keep the forced and induced draft balanced and the furnace pressure under control during the runback.
Lesson quiz · 5 questions
Score 60% or more to complete this lesson.
Create a free account to save your progress, take quizzes and earn a certificate.