
IRW-230 · Lesson 5 of 12 · 21 min
Fastening deck: welds, screws and pins
▶ Video coming soon A video version of this lesson is on the way.
Deck that is laid but not fastened is just a pile of sheets. Fastened, it becomes a floor that carries people and concrete and a roof that holds against wind uplift and ties the whole building together as a diaphragm. On the fourth deck night, Tuesday, November 3, Ilona put three fasteners on the bench in front of the apprentices: a sheet of deck with a round weld burned through it into a scrap of angle, a self-drilling screw, and a powder-actuated pin with its washer. "Every one of these is in the design," she said. "The engineer counted them. If the drawing says four per sheet at every support, it means four, in the right ribs, the right size. A missing fastener is a missing piece of the roof."
This lesson covers how deck is fastened to its supports and to itself: arc spot welds, screws and powder-actuated pins, side-lap fasteners, fastening patterns, edge and perimeter fastening, and the qualifications and safety rules for welding and powder-actuated tools.
What the fasteners do
Deck fasteners have three jobs. Support fasteners hold each sheet down to the joists or beams against wind uplift and keep it from sliding. Side-lap fasteners join the edges of neighbouring sheets so that they act together rather than as separate strips. Perimeter fasteners tie the deck to the edge members and walls so that the deck can pass the diaphragm forces into the frame. The designer works out how many of each are needed from the wind, snow and earthquake loads and the deck manufacturer's diaphragm tables, and the deck layout drawing gives the pattern.
Fastening patterns
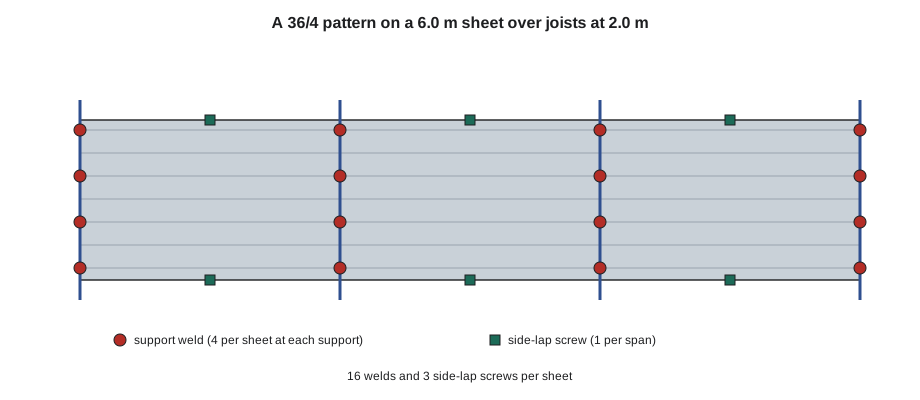
Support fastening is usually shown as a pattern: the number of fasteners in each sheet at each support, and which ribs they go in. A common shorthand, used on many drawings in North America, gives the sheet width and the number of fasteners across it. For a sheet about 914 mm (36 in) wide, a pattern of 36/4 means four fasteners across the sheet at each support, in the ribs the detail shows, and 36/7 means seven, one in every rib. Where sheets lap, one fastener may go through both sheets. Side-lap fastening is given as a spacing along the lap, or a number per span.
Worked problem
Counting fasteners on a roof
Airpark's roof deck sheets are 6.0 m long and cross joists at 2.0 m, so each sheet rests on four supports. The layout calls for a 36/4 weld pattern at every support and one side-lap screw at the middle of each span. There are 1,320 sheets. How many welds and screws are needed?
Show solution
- Welds per sheet = 4 supports × 4 = 16.
- Side-lap screws per sheet = 3 spans × 1 = 3.
- Total welds = 1,320 × 16 = 21,120.
- Total screws = 1,320 × 3 = 3,960.
Answer: About 21,000 welds and 4,000 screws, before perimeter and edge fasteners. At about 60 welds an hour each, four welders need about 21,120 ÷ (4 × 60 × 8) = 11 eight-hour days, which is why the deck crew planned the welding before the first bundle landed.
Arc spot welds
The traditional deck fastener is the arc spot weld, often called a puddle weld. The welder holds a stick electrode against the deck in the bottom of a rib, burns a hole through the deck and fills it, fusing the deck to the steel below. The result is a round button of weld. The drawings give the weld size as a visible or effective diameter, commonly about 16 mm (5/8 in) effective for roof deck, and the welding procedure gives the electrode, current and technique.
- The deck must be tight to the support. A gap between the deck and the steel below gives a weak weld or a hole with no fusion. Workers stand on the deck beside the weld to hold it down.
- The weld must be the right size and fully fused at its edges. An undersized weld, or one that only sits on top of the deck, does not hold.
- Burn-through, where the weld burns a large ragged hole through the deck without fusing it, is a defect; the weld is repaired as the procedure says.
- For the thinnest decks, the deck standard and layout may call for weld washers, small steel washers welded through, so that the thin sheet does not burn away. The layout says when washers are needed.
Arc spot welds are strong and need no special tools, but they are slow, they need a welding power source on the deck, and their quality depends heavily on the welder.
Who may weld deck
In Canada, a company that welds structural steel, including deck, must be certified by the Canadian Welding Bureau to CSA W47.1, with approved welding procedures and qualified welders, and the welding follows CSA W59. Crossbeam holds that certification, and only its welders qualified for the process and position weld deck. Galvanized and primed deck give off fumes when welded; welders work upwind with ventilation or respiratory protection, and hot work rules apply where the deck is near anything that can burn.
Screws
Self-drilling screws are now common for both support and side-lap fastening. A support screw drills through the deck into the steel below and taps its own thread; a side-lap screw joins two layers of deck. Screws are quick, need only a screw gun and batteries, and give a consistent connection. They must be the type, size and length the layout calls for, driven with a screw gun set so that the screw seats without stripping or overdriving, and they must go into steel thick enough for their thread, which the screw maker states. Side laps may also be joined by button punching, a crimp made with a special tool, or by welds on heavier decks, as the layout shows.
Powder-actuated pins
Powder-actuated fasteners, often called pins, are hardened steel nails driven through the deck into the steel below by a tool that fires a small explosive load. Deck pins have a washer under the head to hold the thin sheet. They are very fast and give a consistent connection, but they work only into steel within the range of thickness the pin maker allows: too thin and the pin will not hold, too thick and it will not penetrate. The load colour, the tool's power setting and the pin are chosen from the maker's guide for the support steel, and test shots are made at the start.
Ontario's construction regulation requires that explosive actuated fastening tools be used only by workers trained in their safe use, and the tools themselves are made and used to CSA Z166. Workers using them wear eye and hearing protection, never point a tool at anyone, load it only just before use, and follow the maker's instructions for misfires.
Ilona's crew kept the powder loads in a locked box, logged every box in and out, and returned unused loads at the end of the day. A spent load found on a deck is a sign that someone was careless, and a live load found on a deck is a serious incident.
Edges, perimeters and openings
The deck layout usually calls for more fasteners at the edges of the roof or floor, along the perimeter members and walls, and at the ends of sheets, because the diaphragm forces are greatest there and wind uplift is highest at roof edges and corners. Edge pattern, perimeter spacing and the fasteners at openings are shown separately from the field pattern, and they are easy to miss when a crew is working fast. At Airpark, the layout called for the field pattern of 36/4, a 36/7 pattern at the first two joists in from each wall, and perimeter welds at 300 mm (12 in) to the wall angles.
Quality while fastening
The crew checks its own fastening as it goes. Welders look at each weld for size and fusion; screw and pin crews check that each fastener is seated, in the right rib and on a support. The foreperson walks behind the crew, counts fasteners in sample sheets, and looks for missed supports, especially at end laps, where a sheet has two supports close together, and at the edges. Lesson 11 covers inspection of decking in detail.
Fastening a floor at Ashcroft
At Ashcroft, the third-floor composite deck was fastened to the beams with arc spot welds, two of Ilona's welders working behind the spreading crew on October 14 and 15. Side laps were screwed. Shay ran the screw gun on the side laps for most of the second day and found that a screw driven at a slight angle wobbles and strips; driven straight down, with the gun set right, it seats every time. By the end of the day he had driven about 400 screws and had his work checked by Ilona at every tenth sheet.
Choosing the fastener
The fastener type is the designer's choice, but the erector often proposes one. Welds suit heavy steel and are needed where the specification requires them or where screws and pins are not permitted. Screws suit most roof deck and side laps and need no hot work permit, which matters over occupied buildings and near combustible insulation. Pins are the fastest on steel of the right thickness and leave no fumes. A change of fastener is a change to the design: the erector submits it through the general contractor, and the engineer must approve it before the crew uses it, because each fastener type has its own strength in the deck manufacturer's diaphragm tables.
Setting up for welding on deck
Welding deck means running welding leads across the steel and the deck. The welding machine stays on the ground or on a solid platform, its leads are run so that they do not hang over open edges, cross ladders or lie where they can be cut by deck edges, and the ground clamp is fastened to the steel close to the work. A poor ground, clamped to deck far from the weld, gives poor welds and can send current through bearings, bolts or other trades' equipment. Leads are inspected daily for cuts and burns.
Welding on a roof deck is hot work. Sparks and slag fall through openings and side laps, and deck near combustible insulation, roofing or stored materials can start fires. Hot work permits are issued as the general contractor's program requires, a fire watch stays after welding, and fire extinguishers are kept within reach. At Airpark, the deck was bare steel when it was welded, but the warehouse floor below had pallets of the general contractor's material stored in two bays, and Ilona had them moved before welding started over them.
Screw guns and screws
Screw guns for deck are often stand-up tools, with a long extension so the worker can drive screws while standing, which saves the back on a large roof. The gun's depth or clutch setting is adjusted on a scrap of the job's deck and steel so that each screw seats its washer firmly without crushing it or stripping its thread. A screw that spins without tightening is removed and replaced with a new screw in a fresh hole beside it. Screws that hit the edge of a rib, or that drill into the support at an angle, are also replaced. Batteries are charged and rotated through the day so the crew does not end up driving screws with a weak tool, which strips more of them.
Pins and test shots
Before pinning deck on a job, the crew makes test shots on the job's support steel with the chosen pin and load, and checks that the pin head stands at the height the maker's gauge shows. A pin that sits too high is underdriven and may not hold; one that sits too low may have damaged the deck washer or punched through. The load colour and the tool's power setting are adjusted until the test shots are right, and the result is noted. If the steel thickness changes, from a joist chord to a heavier beam flange for example, the test is repeated.
Fastening near joist seats and girders
Where deck crosses a joist girder or a beam at the end of a joist bay, it lands on a support with a joist seat close by. Fasteners at those supports must go into the girder's top chord or the beam flange, not into the joist seat or the gap between, and they must clear the bolts at the joist seat. The deck layout often shows extra fasteners at girder lines, because that is where diaphragm forces pass from one bay to the next. Ilona's crew marked the girder lines on the deck with paint before fastening so that no welder could mistake a girder line for an ordinary joist.
Common mistakes
MistakeLeaving out the extra fasteners at edges and perimeters.
InsteadFollow the edge and perimeter patterns, which are shown separately from the field.
MistakeWelding deck that is not tight to the support.
InsteadHold the deck down tight before welding so that the weld fuses.
MistakeDriving pins into steel outside the maker's thickness range.
InsteadChoose pins and loads from the maker's guide and make test shots.
MistakeUsing a powder-actuated tool without training.
InsteadOnly trained workers use the tools, with eye and hearing protection.
MistakeSubstituting screws for welds to save time.
InsteadChange a fastener type only with the engineer's approval.
Summary and key terms
- Support, side-lap and perimeter fasteners hold deck down, tie sheets together and carry diaphragm forces.
- Patterns such as 36/4 give the number of fasteners across each sheet at each support.
- Arc spot welds must be the right size and fused, with the deck tight to the support; weld washers are used where the layout calls for them.
- Deck welding in Canada is done by a CWB-certified company to CSA W47.1 and CSA W59.
- Screws and powder-actuated pins must match the layout and the support steel; pins are used only by trained workers.
- Edges, perimeters and openings get extra fasteners, and any change of fastener needs the engineer's approval.
- Arc spot weld
- A round weld burned through deck into the support below; also called a puddle weld.
- Weld washer
- A steel washer welded through thin deck so the sheet does not burn away.
- Self-drilling screw
- A screw that drills and taps its own hole through deck into steel.
- Powder-actuated fastener
- A pin driven by a tool that fires an explosive load.
- Side-lap fastener
- A screw, crimp or weld that joins the edges of neighbouring sheets.
- Fastening pattern
- The number and position of fasteners in each sheet at each support.
- Burn-through
- A weld defect where the deck is burned away without fusing.
Practice problems
Work each problem on paper first, then reveal the answer to check.
Sheets 4.0 m long cross joists at 2.0 m. With a 36/4 pattern, how many welds per sheet?
Show answer
3 supports × 4 = 12 welds.
How many side-lap screws per sheet at one per span?
Show answer
2 spans × 1 = 2 screws.
A roof has 900 sheets at 12 welds each. How many welds?
Show answer
10,800 welds.
Who may weld structural steel deck in Canada?
Show answer
A company certified by the CWB to CSA W47.1, using qualified welders.
What protection is worn with a powder-actuated tool?
Show answer
Eye and hearing protection, by a trained worker.
Lesson quiz · 5 questions
Score 60% or more to complete this lesson.
Create a free account to save your progress, take quizzes and earn a certificate.