
HSE-310 · Lesson 9 of 12 · 27 min
Chemical and process hazards: an overview
Many plants use chemicals that can burn, explode, poison or corrode: refrigerants such as ammonia, cleaning and sanitizing chemicals, acids and caustics, solvents, compressed gases, fuels, resins and the materials being processed. Some plants run processes with large inventories of highly hazardous chemicals at high temperatures and pressures. When those processes fail, the result can be a major accident that kills workers and harms people far outside the fence. This lesson gives an overview of chemical and process hazards so that everyone in a plant understands what is at stake. HSE-311 covers process safety management, HSE-312 covers chemical handling and storage, HSE-313 covers combustible dust, and HSE-102 covers hazard communication.
Personal safety and process safety
Occupational or personal safety deals with hazards to individual workers: slips, cuts, strains, falls and contact with machinery. Process safety deals with the prevention of fires, explosions and toxic releases from the loss of containment of hazardous materials or energy. The two need different measures. A plant can have an excellent personal injury record and still be heading for a major accident, because the indicators it watches, such as lost-time injuries, say little about the condition of its relief valves, alarms, inspections and operating procedures. The 2005 explosion at the BP Texas City refinery, which killed 15 workers, happened at a site that had been proud of its low injury rate.
| Aspect | Personal safety | Process safety |
|---|---|---|
| Typical events | Slips, cuts, strains, falls, caught-in injuries | Fires, explosions, toxic releases |
| Frequency and severity | Frequent, usually low to moderate severity | Rare, potentially catastrophic |
| Who is affected | Usually the individual worker | Many workers and the public |
| Key controls | Guarding, PPE, procedures, training | Design, containment, instrumentation, relief, integrity, management of change |
| Indicators | Injury rates | Loss of containment events, safety system demands, overdue inspections |
Lessons from major accidents
Major accidents are rare in any one plant, so most people never experience one. That is why industries study them closely. The same causes appear again and again: hazards that were not understood, safeguards that had been bypassed or allowed to deteriorate, changes made without review, alarms ignored or overwhelmed, and warning signs that were missed or normalized. HSE-311 examines these cases in depth; the short summaries below give the flavour.
| Event | What happened | Key lessons |
|---|---|---|
| Bhopal, India, 1984 | Water entered a tank of methyl isocyanate; a toxic cloud killed thousands in the surrounding community | Safety systems out of service, inventory too large, poor community planning |
| Piper Alpha, North Sea, 1988 | A pump was restarted while its relief valve was removed under another permit; fire and explosions killed 167 | Permit-to-work and handover failures |
| BP Texas City, United States, 2005 | A tower was overfilled during start-up; vapour ignited, killing 15 | Process safety not measured by injury rates; trailers sited near the unit |
| Lac-Mégantic, Canada, 2013 | A runaway train of crude oil tank cars derailed and exploded in a town, killing 47 | Inadequate securement, regulatory gaps, crude properties understated |
| West Fertilizer, United States, 2013 | Ammonium nitrate detonated during a fire, killing 15, mostly first responders | Hazard not recognized; storage in combustible building; land use |
| Beirut, Lebanon, 2020 | Ammonium nitrate stored for years in a port warehouse exploded, killing more than 200 | Long-term unsafe storage, ignored warnings |
Common chemical hazards in ordinary plants
You do not need to work in a refinery to face serious chemical hazards. Ordinary plants have plenty of them, and some of the most common are easy to underestimate because they are familiar.
| Chemical or system | Where found | Main hazards |
|---|---|---|
| Anhydrous ammonia refrigeration | Food and beverage processing, cold storage, ice rinks | Toxic and corrosive release; flammable in a narrow range |
| Chlorine and sanitizers | Water treatment, food plants, pools | Toxic gas; mixing bleach with acids releases chlorine |
| Acids and caustics | Cleaning in place (CIP), metal finishing, batteries | Severe burns, eye damage, violent reactions with each other |
| Solvents | Painting, degreasing, printing, adhesives | Flammable vapours, health effects from breathing them |
| Compressed and liquefied gases | Welding gases, nitrogen, carbon dioxide, propane | Pressure release, asphyxiation, fire |
| Combustible dusts | Food, wood, plastics, metals, pharmaceuticals | Dust explosions and flash fires (HSE-313) |
| Carbon monoxide | Propane forklifts, furnaces, gas heaters | Toxic, odourless; accumulates indoors |
Worked problem
Mixing cleaners
A sanitation worker in a food plant runs out of the usual acid cleaner and decides to use some chlorinated cleaner from another area in the same drain, where acid residue remains. Why is this dangerous, and what controls should exist?
Show solution
- Chlorinated cleaners contain hypochlorite. Mixing them with acids releases chlorine gas, which is toxic and can be deadly in an enclosed area.
- The worker did not know the reaction hazard, or the labels and training did not make it clear.
- Controls: compatibility rules on labels and charts at sanitation stations, separate storage of acid and chlorinated products, dedicated dispensing systems that prevent mixing, and training on the safety data sheet sections on incompatibilities.
- The plant should also make sure substitutes are approved before use, and that workers can get the right product rather than improvise.
Answer: Mixing hypochlorite and acid releases chlorine gas. Segregation, clear labelling, dispensing systems and training on incompatibilities prevent it.
Ammonia refrigeration
Anhydrous ammonia is the refrigerant in many food plants, cold storage warehouses and arenas, because it is efficient and has little effect on climate. It is also toxic and corrosive. A large leak can produce a cloud that injures people inside and outside the plant. Most people can smell ammonia at concentrations well below dangerous levels, which gives some warning, but the smell also causes panic. Ammonia systems need trained operators, leak detection, ventilation, emergency shut-offs, relief systems discharging to safe locations, and an emergency response plan coordinated with the local fire department.
In Canada, ammonia systems are governed by provincial boiler and pressure vessel and refrigeration rules (for example, the Technical Standards and Safety Authority in Ontario), CSA B52 Mechanical refrigeration code, and the Environmental Emergency Regulations under the Canadian Environmental Protection Act for facilities storing ammonia above the regulated threshold. The 2017 Fernie arena release in British Columbia, which killed three workers, led to tighter oversight of ammonia refrigeration across the country.
How hazardous a release could be
Process safety specialists estimate how far a release could spread and at what concentration, to plan emergency response and site buildings. The full methods are complex, but a simple calculation shows why even a modest leak inside a closed room can quickly reach dangerous levels.
# How quickly could an ammonia leak reach a dangerous level in a closed room? (simplified, illustrative)
# Assumes perfect mixing and no ventilation, at about 20 C and 1 atm.
room_m3 = 15 * 10 * 5           # a 750 m3 machinery room
leak_g_per_min = 300            # a small leak at a valve packing
mol_mass = 17.03                # g/mol for ammonia
molar_volume = 24.1             # L per mol at 20 C
def ppm_after(minutes):
    gas_l = leak_g_per_min * minutes / mol_mass * molar_volume
    return gas_l / (room_m3 * 1000) * 1e6
for t in (5, 15, 30, 60):
    print(f"After {t:>2} min: about {ppm_after(t):6.0f} ppm")
print("For comparison: smell threshold about 5 ppm; IDLH 300 ppm (NIOSH)")After 5 min: about 2830 ppm After 15 min: about 8491 ppm After 30 min: about 16982 ppm After 60 min: about 33964 ppm For comparison: smell threshold about 5 ppm; IDLH 300 ppm (NIOSH)
Layers of protection
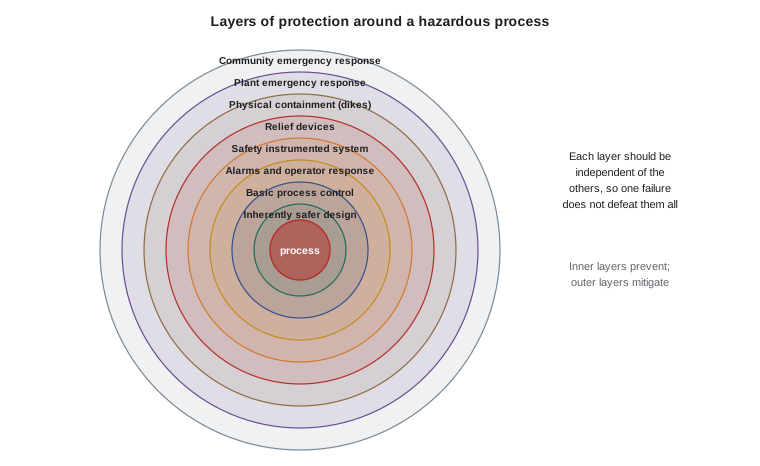
Process safety relies on several independent layers of protection, so that if one fails another stops the accident. The layers start with inherently safer design, such as using less of a hazardous material or a less hazardous one, and continue through the basic control system, alarms and operator response, safety instrumented systems that shut the process down automatically, relief devices, physical containment such as dikes, and finally emergency response. The image of several slices of Swiss cheese, each with holes, is often used: an accident happens only when the holes in every layer line up. Each layer must be maintained and tested, because a layer that has quietly failed gives no protection.
# Independent layers multiply: how often might an initiating event become a release? (illustrative)
initiating_per_year = 0.1          # e.g. a control valve failure once in 10 years
layers = {"alarm and operator response": 0.1,
          "safety instrumented shutdown": 0.01,
          "relief valve": 0.01}
f = initiating_per_year
for name, pfd in layers.items():
    f *= pfd
    print(f"after {name:<30} {f:.1e} per year")
print(f"About once in {1 / f:,.0f} years, if every layer is independent and maintained")
print("If the relief valve is out of service (probability 1), that becomes once in", f"{1 / (f / 0.01):,.0f} years")after alarm and operator response 1.0e-02 per year after safety instrumented shutdown 1.0e-04 per year after relief valve 1.0e-06 per year About once in 1,000,000 years, if every layer is independent and maintained If the relief valve is out of service (probability 1), that becomes once in 10,000 years
Management of change
Many major accidents followed changes that seemed harmless: a substituted chemical, a new bypass line, a modified procedure, a change in staffing, a temporary repair that became permanent. Management of change (MOC) is the process of reviewing changes for their safety effects before they are made, updating drawings, procedures and training, and checking the change before start-up. In ordinary plants, MOC applies to changes in equipment, chemicals, processes, procedures, software and organization, not just to large projects. HSE-103 introduced MOC; HSE-311 covers it for process safety.
Worked problem
A small change with large effects
To save money, a plant switches to a cheaper degreasing solvent from a new supplier. The purchasing department makes the change without telling anyone else. What could go wrong, and what would management of change have caught?
Show solution
- The new solvent may have a lower flash point, making it more flammable than the old one.
- It may be more toxic, or have a different exposure limit, needing different ventilation or PPE.
- It may be incompatible with materials in the degreasing tank, gaskets or storage containers.
- A management of change review would compare safety data sheets, check ventilation and fire controls, update procedures and labels, and train workers before the switch.
Answer: Changing a chemical can change fire, health and compatibility hazards. Management of change reviews these before the switch, not after an incident.
Carbon monoxide from fuel-burning equipment
Carbon monoxide is one of the most common toxic gas hazards in ordinary plants and one of the easiest to miss, because it has no colour or smell. Propane forklifts, gas-fired heaters, furnaces and generators produce it, and it can build up in closed buildings in winter or in trailers being loaded by forklifts. Controls include maintenance and emission testing of engines, ventilation, carbon monoxide detectors, electric forklifts where possible, and training to recognize headaches, dizziness and nausea as warning signs.
Common mistakes
MistakeJudging process safety by the lost-time injury rate.
InsteadTrack process safety indicators such as loss of containment events and overdue inspections.
MistakeAssuming major accidents happen only in refineries and chemical plants.
InsteadOrdinary plants have ammonia, chlorine, acids, solvents, gases and dusts that can cause serious events.
MistakeMixing cleaning chemicals to get a stronger effect.
InsteadCheck incompatibilities on safety data sheets; never mix chlorinated and acid products.
MistakeLeaving a safety layer out of service because the others are still there.
InsteadEach layer is needed; a failed layer gives no protection and must be restored or compensated.
MistakeTreating chemical substitutions as purchasing decisions.
InsteadReview chemical changes through management of change.
Summary and key terms
- Process safety prevents fires, explosions and toxic releases; it needs different controls and indicators from personal safety.
- Major accidents show repeated causes: poorly understood hazards, failed safeguards, unreviewed changes and missed warnings.
- Ordinary plants have serious chemical hazards: ammonia, chlorine, acids and caustics, solvents, gases, dusts and carbon monoxide.
- Incompatible chemicals, such as hypochlorite and acids, can release toxic gases when mixed.
- Ammonia refrigeration needs trained operators, leak detection, ventilation, relief and emergency planning.
- Independent layers of protection reduce the chance of a major accident only if each is maintained and tested.
- Management of change reviews equipment, chemical, procedure and organizational changes before they are made.
- Process safety
- Preventing fires, explosions and toxic releases from loss of containment of hazardous materials or energy.
- Loss of containment
- An unplanned release of material or energy from where it should be held.
- Major accident
- An event causing multiple deaths or serious harm to people, property or the environment.
- Incompatible chemicals
- Chemicals that react dangerously when mixed.
- Anhydrous ammonia
- Ammonia without water, used as a refrigerant; toxic and corrosive.
- IDLH
- Immediately dangerous to life or health: a concentration from which escape is needed without delay.
- Layer of protection
- An independent safeguard that can stop an initiating event from becoming an accident.
- Safety instrumented system
- An automatic system that takes a process to a safe state when limits are exceeded.
- Relief device
- A valve or rupture disc that releases pressure to protect equipment from bursting.
- Management of change
- The process of reviewing changes for safety effects before they are made.
Practice problems
Work each problem on paper first, then reveal the answer to check.
How does process safety differ from personal safety?
Show answer
It prevents fires, explosions and toxic releases affecting many people, using design, containment and integrity controls.
Why is a low injury rate not proof of process safety?
Show answer
Injury rates do not measure the condition of process safeguards; Texas City had a low injury rate.
Name three repeated causes of major accidents.
Show answer
Poorly understood hazards, bypassed or deteriorated safeguards, unreviewed changes, ignored alarms, missed warnings.
What happens if hypochlorite cleaner is mixed with acid?
Show answer
Chlorine gas is released.
List four controls for an ammonia refrigeration system.
Show answer
Trained operators, leak detection, ventilation, emergency shut-offs, relief to safe locations, emergency plan.
What is the NIOSH IDLH for ammonia?
Show answer
300 ppm.
Explain the Swiss cheese image of layers of protection.
Show answer
Each layer has weaknesses; an accident happens only when the holes in every layer line up.
Why must each layer of protection be tested?
Show answer
A layer that has failed quietly gives no protection, and the overall risk rises sharply.
Give three kinds of change that need management of change.
Show answer
Equipment, chemicals, procedures, software, staffing or organization.
Which course covers process safety management in depth?
Show answer
HSE-311.
Lesson quiz · 5 questions
Score 60% or more to complete this lesson.
Create a free account to save your progress, take quizzes and earn a certificate.