
GAS-330 · Lesson 12 of 12 · 26 min
Case study: a new industrial gas service
▶ Video coming soon A video version of this lesson is on the way.
This lesson follows the Keystone Coatings job from lesson 1 from start to gas-in: the site meeting on September 15, the load list and the utility's approval, the sizing in lesson 7, the welding of the main in October, the regulators and their overpressure protection, the pressure test on November 5, the utility's meter set on November 6 and the purge and start-up on November 10. It ends with what remained to be done after the case was written, all of it planned for late November and December. Each step uses something from an earlier lesson, and the point of the case is how they fit together on one job.
The plant and the decisions
Keystone's warehouse on Arvin Avenue was a 1990s steel building with a pipe rack along its north wall and a low roof over the office end. Teresa Lindqvist, the plant manager, had a firm date: the first customer order, for powder-coated shelving, was due to ship in mid-December, and the cure oven maker's technician was booked for the last week of November. Maureen's first decisions, made on the site walk on September 15 with Grant and Ayesha, set the rest of the job:
- Delivery pressure 35 kPa (5 psig), the lowest pressure that gave sensible pipe sizes and suited the cure oven's train, as lesson 1 described.
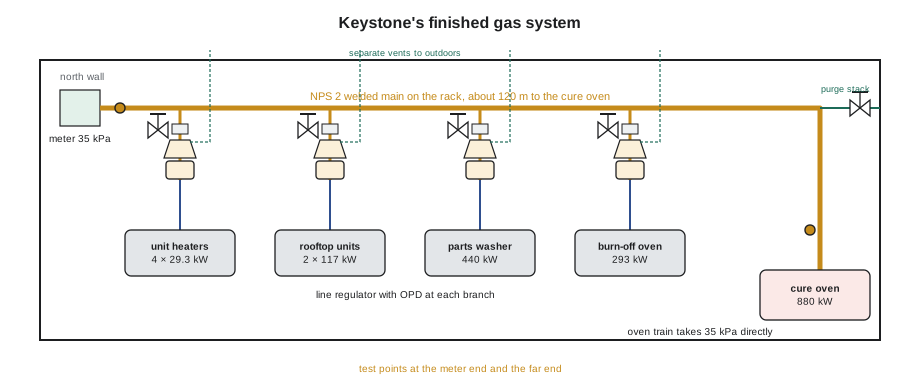
- One welded steel main along the rack, because it was long, at elevated pressure, in an industrial building and exposed to forklift traffic at one end, with flanged connections at valves and strainers.
- Line regulators with integral slam-shut OPDs for every appliance whose maximum inlet was 3.5 kPa: the burn-off oven, the parts washer heater, the rooftop units and the unit heaters. Only the cure oven's train, built for the delivery pressure, would take the main pressure directly.
- Strainers upstream of every line regulator, after the car wash in lesson 5.
- The utility's meter set on the north wall, away from the truck dock, with bollards.
Maureen's load list went to Enbridge on September 18, and the approval for a rotary meter at 35 kPa, with an electronic volume corrector, came back on September 29. Priya Nair handled the paperwork: the notifications and inspections TSSA requires for an installation of this size.
| Date | Step | Lesson |
|---|---|---|
| Tue Sept 15 | Site walk; delivery pressure and layout decided | 1 |
| Fri Sept 18 | Load list to the utility | 1 |
| Tue Sept 29 | Utility approval: rotary meter at 35 kPa | 6 |
| Thu Oct 1 | Sizing; main kept at NPS 2 for margin and a future oven | 7 |
| Tue Oct 13 to Fri Oct 16 | Main welded by Ironline; regulators and branches by Bayline | 3, 5, 8 |
| Thu Nov 5 | Pressure test, 345 kPa for 2 hours | 10 |
| Fri Nov 6 | Utility sets the meter and corrector | 6 |
| Tue Nov 10 | Outdoor purge, OPD tests, regulator settings, first appliances on | 2, 5, 11 |
| Late November (plan) | Cure oven start-up by its maker's technician | — |
| Mid-December (plan) | First production order ships | — |
Welding the main
Dario Russo and his helper from Ironline welded the NPS 2 main over the week of October 12, starting on the Tuesday after the Thanksgiving Monday. Grant and Ayesha worked with them on Tuesday, setting the rack supports at the spacing Maureen had marked and fitting the flanged inlet valve and strainer at the meter end, and Grant came back on Thursday to fit the branch valves and the strainers and line regulators at each branch. The main was hung on clamps that let it slide on the rack, with a fixed anchor at the midpoint and a gentle offset at the far end where it dropped to the cure oven, so that expansion in the unheated building would not push on the oven's train. Where the main crossed the forklift aisle at the burn-off oven, it was raised and guarded. Every weld was numbered on Ayesha's sketch.
The branches went to each appliance with a manual valve, a strainer and a line regulator in that order, set at the heights the maker's instructions allowed and where they could be reached from the floor or a platform. Each regulator's tag confirmed its maximum inlet of 35 kPa, its outlet class and its integral OPD, and each vent was piped outdoors on its own line, sized for its length as lesson 4 explained, because the regulators were not certified for vent limiters in that location. The rooftop units' regulator went on the roof at the top of the riser, with its vent turned down and screened.
The pressure test
The specification, written by Keystone's engineer, called for a test at 345 kPa (50 psig) for two hours with a data logger, above the code's minimum for this system. On Thursday, November 5, the line regulators and the oven's train were isolated: the regulators' inlet valves closed and their inlet unions opened to atmosphere, so that a passing valve would show and no regulator would see the test pressure. Grant filled the main with nitrogen from the meter end through a test rig with its own regulator and relief valve, in two stages, holding at 100 kPa (15 psig) while Ayesha brushed every weld and flange with solution. Then he brought it to the full test pressure and isolated the rig. Maureen made them wait thirty minutes for the temperature to settle in the unheated warehouse before the logger started.
Worked problem
Did the main pass?
At the start of the timed test the main read 345 kPa with the pipe at 9.0 °C. Two hours later it read 344 kPa with the pipe at 8.5 °C. Atmospheric pressure was 100 kPa. Does the change match the temperature change?
Show solution
- Predicted end pressure:
- \[445 \times \frac{273.15 + 8.5}{273.15 + 9.0} = 445 \times \frac{281.65}{282.15} = 444.2 \text{ kPa absolute}\]
- Gauge:
- \[444.2 - 100 = 344.2 \text{ kPa}\]
- Measured: 344 kPa.
Answer: The small drop is what the half-degree of cooling predicts, and the logger trace was flat apart from that slow drift. The main passed. Maureen signed the test record, the inspector reviewed the logger printout and the test tag, and the welds were painted the next day.
The meter set
On Friday, November 6, Enbridge set its rotary meter, service regulator and electronic volume corrector on the north wall, inside the bollards Bayline's sub had set the week before, and tested its own service. Grant met the utility crew and confirmed with them where Bayline's piping began: at the flange on the outlet of the meter set's outlet valve. The utility left the meter outlet valve closed and locked until Bayline was ready to purge.
Purge and gas-in
On Tuesday, November 10, the main went into service. With 35 kPa in the main, both codes required an outdoor purge. The purge point was at the far end of the main, by the cure oven, where a NPS 1 purge line ran out through the east wall to a short vertical purge stack, with a quarter-turn valve at its base, well clear of the dock doors, the rooftop units' air intakes and the street. The yard was coned off and the stack area signed. The main was still full of nitrogen at a low pressure from the test, so the purge into service was nitrogen to gas, with no air involved.
Worked problem
How much does the purge discharge?
The main holds about 0.28 m³, including its branches up to their closed valves. If the purge discharges about twice that before the indicator shows a steady gas reading, how much nitrogen and gas is released, and how long does it take at about 25 m³/h?
Show solution
- \[2 \times 0.28 = 0.56 \text{ m}^3\]
- \[\frac{0.56}{25} \times 3{,}600 = 81 \text{ s}\]
Answer: About a minute and a half of controlled discharge, with Ayesha at the valve and the indicator in the stream. A purge of this size released through an open pipe inside the warehouse would have filled part of the building with a flammable mixture.
Grant opened the utility's meter outlet valve slowly once the utility's technician unlocked it, and Ayesha cracked the purge valve. The indicator read zero combustible gas while the first nitrogen came out, rose through the LEL in about a minute, and held at a steady fuel gas reading at about eighty seconds. She closed the valve. Grant capped the purge fitting and leak-tested it.
Regulators and overpressure protection
Before any appliance ran, every line regulator and its OPD was checked, as lessons 3 and 5 required. At each branch, with the appliance valve closed, Grant applied nitrogen through the OPD's test port and raised it slowly until the slam-shut tripped: each one tripped within a small margin of its tagged setting. He reset each one, opened the regulator's inlet valve and, with one burner of each appliance lit to give some flow, set its outlet: 3.0 kPa (12 in. w.c.) for the washer heater and the burn-off oven, 2.5 kPa (10 in. w.c.) for the rooftop units and 2.0 kPa (8 in. w.c.) for the unit heaters. Then he read lockup with the appliances off and the full-load outlet with each appliance at high fire, and logged both. Every lockup rose a little and held steady, and no slam-shut tripped in normal operation.
| Branch | Set point | Lockup (held) | At full load | OPD trip test |
|---|---|---|---|---|
| Unit heaters | 2.0 kPa | 2.3 kPa | 1.8 kPa | Tripped at tag setting |
| Rooftop units | 2.5 kPa | 2.8 kPa | 2.2 kPa | Tripped at tag setting |
| Parts washer heater | 3.0 kPa | 3.3 kPa | 2.7 kPa | Tripped at tag setting |
| Burn-off oven | 3.0 kPa | 3.3 kPa | 2.8 kPa | Tripped at tag setting |
| Main at far end | 35 kPa delivery | — | About 31 kPa with all four branches firing | Utility service |
Starting the appliances
The unit heaters and the rooftop units were started first, each purged through its own ignition system as its maker's instructions describe, each new connection leak-tested at operating pressure, and each checked for manifold pressure, temperature rise and combustion, as GAS-320 covered for rooftop units. The burn-off oven was started next by Grant with the maker's start-up sheet. The parts washer heater was the largest appliance started that day, and Maureen had Ayesha check its input by clocking the new rotary meter, with every other appliance off, using the pressure and temperature correction from lesson 6.
Worked problem
Clocking the washer heater on Keystone's meter
The washer heater is rated 440 kW. The meter runs at 35 kPa gauge, atmospheric pressure is 100 kPa and the gas is at 8 °C. With only the washer heater firing, the meter's 1 m³ test dial turned once in 117 s. Use 37.5 MJ/m³. What is the heater's input?
Show solution
- Actual flow:
- \[\frac{1}{117} \times 3{,}600 = 30.77 \text{ m}^3/\text{h}\]
- Factors:
- \[\frac{100 + 35}{101.325} = 1.3323, \quad \frac{288.15}{281.15} = 1.0249\]
- Standard flow:
- \[30.77 \times 1.3323 \times 1.0249 = 42.02 \text{ m}^3/\text{h}\]
- Input:
- \[42.02 \times \frac{37.5}{3.6} = 437.7 \text{ kW}\]
Answer: The heater is firing at about 99.5 in 100 of its rating. Without the correction, the reading would have suggested 320 kW, and someone could have turned the heater up by more than a third trying to reach its rating.
The utility's corrector, read on its display with the utility's permission, showed a corrected flow within a fraction of Ayesha's figure, which was a satisfying check on her arithmetic. With the four branches running, Grant read the pressure at the far end of the main: about 31 kPa, close to what Ayesha's sizing had predicted for this load, and far above the cure oven train's minimum. The cure oven's own manual valve stayed closed and tagged, waiting for its maker's technician.
Handover
Before leaving, Maureen put together the handover package that Keystone and the inspector needed: the as-built drawing with the design note from lesson 7, giving the delivery pressure, the design drop, the method and the allowance for a second oven; the welding records, with Dario's qualification and the numbered weld map; the pressure test record and logger printout; the purge record; the regulator and OPD commissioning sheet; the appliance start-up sheets; and the regulator and OPD makers' maintenance instructions. She walked Teresa and her maintenance lead along the main, showing them the meter outlet valve, each branch valve, the OPD reset buttons and what a tripped OPD meant: call Bayline, do not just reset it. Bayline's annual service would check every regulator's lockup and full-load outlet and trip-test every OPD.
What is still to come
As this case was written, three things remained, all of them plans. The cure oven's maker's technician was booked for the week of November 23 to start the oven, with Maureen attending, and TSSA would inspect the oven installation as required. Keystone's first production order was due to ship in mid-December. And the possible second cure oven, two years away, was already allowed for in the main, and written on the drawing so that whoever installs it will know.
Grant summed the job up in the van on the way back from the purge. "Nothing we did was new," he said. "Pressures, regulators, vents, OPDs, meters, sizing, welding, testing, purging. It's just all of it at once." Maureen agreed. "That's what an industrial service is. Get every small thing right in the right order, and write it down."
Common mistakes
MistakeChoosing a higher delivery pressure than the equipment needs.
InsteadChoose the lowest pressure that gives sensible pipe and suits the largest burner.
MistakeFitting line regulators without strainers on a new welded main.
InsteadFit strainers upstream and blow the main clear before regulators go into service.
MistakeLeaving regulators connected during the pressure test.
InsteadIsolate them, with their inlets open to atmosphere, so a passing valve shows.
MistakeStarting appliances before OPDs are trip-tested.
InsteadTest every OPD and set every regulator first.
MistakeClocking an elevated-pressure meter without correction.
InsteadCorrect for pressure and temperature, and compare with the corrector if available.
MistakeHanding over a system with no record of its design.
InsteadLeave drawings, design notes, test, purge and commissioning records with the owner.
Summary and key terms
- Keystone's new service brought together the whole course.
- The delivery pressure, 35 kPa (5 psig), was the lowest that gave sensible pipe and suited the cure oven's train; a welded NPS 2 main, sized by the longest-length method and kept at one size for margin and a future oven, ran along the rack on sliding supports.
- Line regulators with integral slam-shut OPDs, strainers upstream and separate outdoor vents fed every appliance designed for 3.5 kPa or less.
- The main was pressure tested with nitrogen at 345 kPa (50 psig) for two hours, with regulators isolated, after stabilization and with a logger, and the small drop matched the temperature change.
- After the utility set its rotary meter and corrector, the main was purged outdoors from nitrogen to gas through an attended purge stack, the OPDs were trip-tested, the regulators set and checked at lockup and full load, and the appliances started one by one, with the washer heater's input confirmed by a corrected clock test.
- A complete handover package recorded the design and every test.
- Load list
- Every appliance with its input and pressure needs, sent to the utility to size the service.
- Weld map
- A sketch of a welded system with each weld numbered, recording who made it and when.
- Isolation for testing
- Closing and opening components so they are not exposed to the test pressure.
- Purge stack
- A short vertical pipe outdoors that carries a purge discharge up and away from people and openings.
- Commissioning sheet
- A record of the settings and readings taken when a system is put into service.
- Handover package
- The drawings, records and instructions left with the owner at the end of a job.
Practice problems
Work each problem on paper first, then reveal the answer to check.
Why did only the cure oven take the full main pressure?
Show answer
Its gas train was built for the delivery pressure; every other appliance was designed for 3.5 kPa or less.
How were the line regulators protected during the pressure test?
Show answer
Their inlet valves were closed and their inlet unions opened to atmosphere.
Why did Keystone's purge need no air-to-nitrogen step?
Show answer
The main was already full of nitrogen from the pressure test.
At 35 kPa gauge, 100 kPa atmosphere and 8 °C, what is the combined correction factor?
Show answer
1.3323 × 1.0249 = 1.3655.
What should Keystone's staff do if an OPD trips?
Show answer
Call Bayline rather than just resetting it, because a trip means a regulator problem.
Lesson quiz · 5 questions
Score 60% or more to complete this lesson.
Create a free account to save your progress, take quizzes and earn a certificate.