
PWR-120 · Lesson 12 of 12 · 21 min
Routine operation and boiler inspections
▶ Video coming soon A video version of this lesson is on the way.
On Tuesday, November 10, 2026, Tamar worked her first full day shift at Cantwell with nobody standing at her shoulder. Lorne was in the building, but Grazyna had told him to stay in the office unless Tamar called. The shift began with a handover at 7:00, went through four sets of rounds, a low water cutoff test, a bottom blowdown, a chemical delivery and a visit from the insurer's inspector to plan December's internal inspection of hot water boiler 1, and ended with a handover at 15:00. "Nothing exciting happened," Tamar said at the end of it. "That's the point," said Grazyna. "Routine operation is what keeps a plant boring."
This last lesson pulls the course together into the daily work of a plant operator: taking over a shift, making rounds and reading the log, recognising what has changed, carrying out routine tests, and preparing a boiler for the inspections that keep its certificate in force.
Taking over the shift
A shift starts with a handover, ideally face to face at the equipment or the control panel, not just a glance at the log. The outgoing operator tells the incoming one:
- Which boilers and auxiliaries are running, on standby or out of service, and why.
- Any alarms, trips or abnormal readings during the shift, and what was done.
- Equipment under lockout or work permit, and who holds the locks.
- Tests, blowdowns and chemical adjustments done, and any that are due.
- Anything planned: deliveries, contractors, inspections, start-ups or shutdowns.
The incoming operator reads the log, walks the plant and only then accepts the shift. Until the handover is complete the outgoing operator remains responsible. A handover is the moment when information is most easily lost, which is why it is done deliberately and recorded.
Rounds and the log
Rounds are planned walks through the plant at set intervals, usually every one to two hours on an attended plant, to look, listen, feel and record. The log records the readings and events of each round and of the shift. A good log has fixed columns so that one reading can be compared with the same reading on the last round, yesterday and last week.
| Item | Typical logged readings |
|---|---|
| Each boiler | Steam pressure or water temperature, water level, firing rate, stack temperature, flue gas oxygen |
| Feedwater | Deaerator pressure and temperature, tank level, feed pump discharge pressure |
| Condensate | Receiver level and temperature, condensate return conductivity if monitored |
| Fuel | Gas pressure at the train, gas meter reading, oil tank level if used |
| Water treatment | Softener hardness test, boiler water conductivity, chemical tank levels |
| Auxiliaries | Air pressure and dew point, pump pressures, unusual noise or temperature |
| Events | Tests, blowdowns, alarms, trips, work orders, visitors |
The log is a legal record in many jurisdictions and the first thing an inspector or an investigator asks for. Entries are made at the time, in ink or in the plant's electronic system, never filled in later from memory. A mistake is crossed out with a single line and initialed, not erased. Readings are entered as they are, even when they look wrong; then the operator investigates and notes what was found.
Reading trends
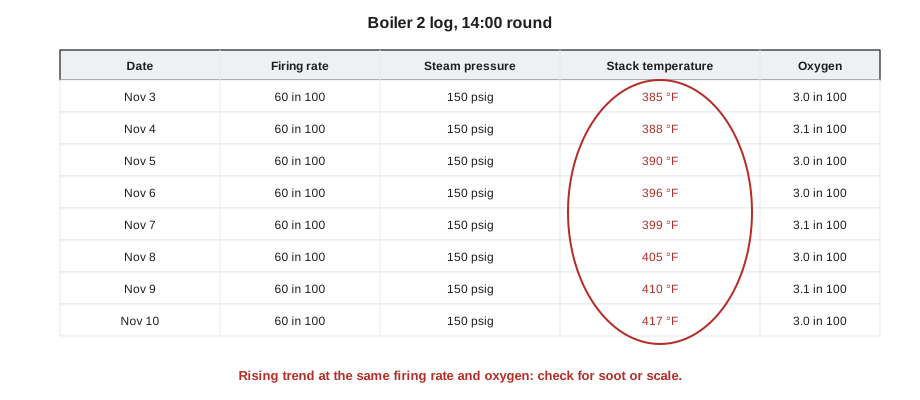
The value of a log is in its trends. A single stack temperature of 417 °F tells an operator little; the same stack temperature rising steadily from 370 °F over a few weeks at the same firing rate tells them that heat is not getting into the water, either because soot is building up on the fire side or scale on the water side (lessons 5 and 9). Other trends worth watching:
- Flue gas oxygen drifting up or down at the same firing rate: a burner or linkage change (lesson 5).
- Feedwater pump discharge pressure falling: a worn pump or a strainer clogging (lesson 4).
- Makeup water consumption rising: condensate being lost somewhere (lessons 4 and 10).
- Boiler water conductivity creeping up between blowdowns: blowdown not keeping pace (lesson 9).
- Air compressor run hours rising: a growing air leak (lesson 11).
When Tamar took her 14:00 readings she noticed that boiler 2's stack temperature was 417 °F against 385 °F at the same firing rate a week earlier. She logged it, compared it with the oxygen reading, which was normal, and wrote a note for Grazyna suggesting a fire-side inspection at the next opportunity. That kind of observation is exactly what rounds are for.
Worked problem
Is the stack temperature rise significant?
Boiler 2's stack temperature was 385 °F a week ago and 417 °F today, both at about 60 in 100 firing rate with 3 in 100 oxygen. A rough rule is that efficiency falls about 1 in 100 for every 40 °F rise in stack temperature. About how much efficiency has been lost, and what does that cost on gas use of 640 therms a day at a gas price of 0.90 dollars a therm?
Show solution
- Temperature rise:
- \[417 - 385 = 32 \text{ °F}\]
- Efficiency loss:
- \[32 \div 40 \times 1 = 0.8 \text{ in } 100\]
- Extra gas per day:
- \[640 \times 0.008 \approx 5.1 \text{ therms}\]
- Cost per day:
- \[5.1 \times 0.90 \approx 4.60 \text{ dollars}\]
Answer: About 0.8 in 100 efficiency, roughly 5 therms of gas or about 4.60 dollars a day, close to 1,700 dollars a year if left alone. Small daily losses add up, and the trend often keeps climbing, which is why it is worth catching early.
Routine tests and duties
Every plant has a schedule of routine duties, set by the manufacturer's instructions, the insurer, the regulations and the plant's own experience. A typical schedule for a low pressure or small high pressure plant:
| Frequency | Duty |
|---|---|
| Each shift or daily | Blow down the water column and gauge glass; check water level and flame; test softener hardness; record readings |
| Daily or as set by treatment program | Bottom blowdown as required; check chemical feed and tank levels |
| Weekly | Low water cutoff test by blowing down the float chamber or probe; check flame signal strength; rotate standby pumps |
| Monthly | Slow drain (evaporation) test of the low water cutoff where required; try-lever test of safety valves if the manufacturer and insurer allow it; check combustion readings |
| Yearly | Combustion tune-up and analysis by a qualified service technician; flame safeguard and fuel train safety tests; safety valve servicing or replacement on schedule; internal inspection |
Tamar's 10:00 low water cutoff test on boiler 1 went as it should: she opened the float chamber blowdown valve, the burner shut off and the low water alarm sounded, and when she closed the valve and the water returned, the burner did not restart until she pressed the manual reset. She logged the time, the result and her initials. A test that is not recorded, as far as an inspector is concerned, was not done.
Tests are carried out the way the procedure says, by an operator who is trained to do them, with the boiler in a safe condition. A test that fails, such as a low water cutoff that doesn't shut the burner off, is not something to note and walk away from: the boiler is taken off line or kept under constant attendance until the fault is fixed, and the chief engineer is told at once.
Inspections
Boilers are inspected by an authorized inspector on a regular schedule. The inspection confirms that the boiler is safe to operate and that its certificate can be renewed. There are two kinds:
- An external inspection is done with the boiler in service. The inspector looks at the boiler, its fittings, safety valves, controls, piping and boiler room, watches tests of the low water cutoff and other safety devices, and reviews the log.
- An internal inspection is done with the boiler shut down, cooled, drained, opened and cleaned. The inspector looks inside the shell, tubes, furnace and drums for scale, corrosion, cracking, bulging, overheating and pitting, and checks the waterside and fireside condition.
In Ohio, boilers are inspected by state inspectors of the Division of Industrial Compliance or by commissioned insurance company inspectors, under Ohio Revised Code Chapter 4104 and the Ohio Administrative Code, and the certificate of operation must be posted near the boiler. The interval depends on the type and use of the boiler; many power boilers are inspected internally every year, and heating boilers on a longer cycle. The plant's chief engineer arranges inspections and the operators prepare the boiler.
Grazyna and the insurer's inspector, Ottoline Brackwater, spent half an hour with Tamar at 13:00 planning December's internal inspection of hot water boiler 1. They agreed the date, the work the plant would do beforehand and the parts to have on hand, such as new handhole gaskets.
Preparing a boiler for internal inspection
Preparing a boiler for an internal inspection is a sequence that brings together much of this course:
- Plan the outage with the chief engineer so the remaining boilers can carry the load, and agree the date with the inspector.
- Shut down the boiler normally (lesson 7) and let it cool slowly, never rushing it with cold water.
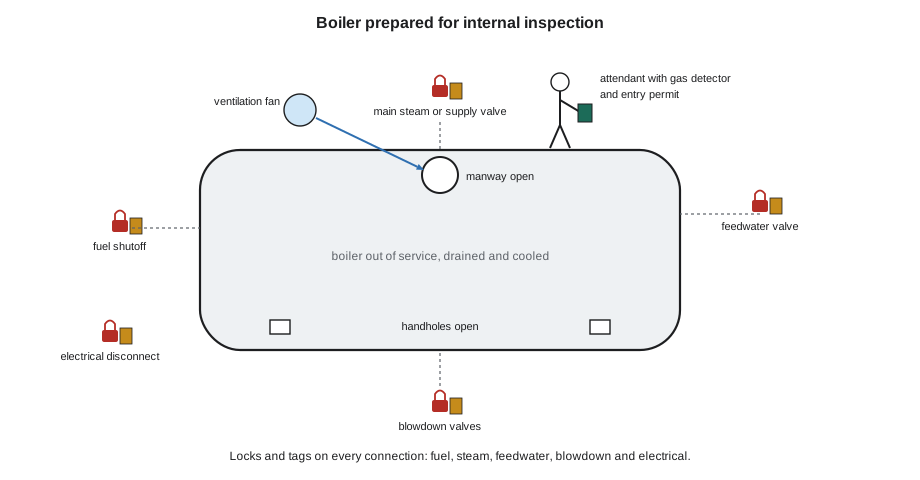
- Isolate it from every connected system: fuel, steam or hot water, feedwater, blowdown, chemical feed and electrical, using the lockout procedure, with two valves and an open drain between the boiler and any other boiler still in service where the design allows (PWR-110 lesson 5).
- Drain it and vent it, open the manholes and handholes, and ventilate it.
- Clean the waterside and fireside so the surfaces can be seen, keeping samples of any scale or deposit for the water treatment company.
- Treat it as a confined space: test the atmosphere, issue a permit and have an attendant outside before anyone enters (PWR-110 lesson 5).
- Have parts ready: new gaskets, and any gauge glasses, safety valves or controls due for replacement.
After the inspection, the boiler is closed up with new gaskets, filled with treated water, the lockouts are removed in the reverse order under the lockout procedure, and it is started up normally (lesson 7), checking all the handholes and manholes for leaks as it warms. The inspector issues a report and, if all is well, the certificate is renewed. Any repairs the inspector requires must be done, and many of them must be done by a certified repair organization.
When something isn't right
The best operators are not the ones who never see a problem; they are the ones who notice early, report clearly and act within their authority. If a reading is abnormal: check it with a second instrument if possible, look for the cause, take any immediate action the procedure calls for, log it and report it. If a situation is getting worse or is beyond your training, shut the boiler down safely and call the chief engineer. No production target is worth an explosion, and every regulation and procedure in this course is built on that rule.
At 15:00 Tamar handed over to the evening operator: both boilers firing, boiler 2's rising stack temperature noted with a suggested fire-side inspection, the chemical delivery received and logged, the low water cutoff tests done, and December's inspection planned. Grazyna read the log, signed it, and told Tamar she would be put forward for her own shifts from the next week.
Good log entries
Grazyna had a rule for the event column of the log: someone who was not there should be able to read the entry and understand what happened, what was done and what still needs doing. She showed Tamar some weak entries from old logs beside the way they should have been written.
| Weak entry | Good entry |
|---|---|
| B2 tripped. Reset. | 10:42 Boiler 2 tripped on flame failure at low fire. Flame signal had been low all morning. Checked scanner lens, found it dirty, cleaned it. Reset at 10:55, started normally, flame signal now normal. Work order raised to check scanner sight tube. |
| Chemicals OK. | 11:30 Chemical delivery received: 4 drums oxygen scavenger, 2 drums internal treatment. Stored in chemical room, labels and safety data sheets checked. |
| Stack temp high. | 14:00 Boiler 1 stack temperature higher than a week ago at the same firing rate; oxygen normal. Suggest fire-side inspection at next opportunity. Note left for chief engineer. |
A good entry gives the time, the equipment, what was observed, what was done, the result and what is still outstanding, followed by the operator's initials. It sticks to facts rather than opinions or blame. It also mentions anything handed on to someone else, such as a work order or a note for the chief engineer, so the next shift knows it has been dealt with and does not raise it a second time.
Plants that keep electronic logs follow the same rules: entries are made at the time, each one is tied to the operator who made it, and corrections are added as new entries rather than overwriting the old ones. Readings that a control system records automatically still need an operator's eyes on them, because a trend that nobody looks at prevents nothing.
Common mistakes
MistakeAccepting a shift after only reading the log.
InsteadTalk to the outgoing operator and walk the plant first.
MistakeFilling in log readings later from memory.
InsteadRecord them at the time, as they are.
MistakeLooking at a single reading instead of the trend.
InsteadCompare with the last round, yesterday and last week.
MistakeNoting a failed safety test and carrying on.
InsteadTake the boiler off line or keep it attended, and report at once.
MistakeCooling a boiler for inspection with cold water.
InsteadLet it cool slowly to avoid thermal stress.
MistakeEntering a boiler without a confined space permit.
InsteadTest, permit and attend every entry.
Summary and key terms
- A deliberate face-to-face handover passes the plant's condition from one operator to the next.
- Rounds record readings in a log; the trends show developing problems.
- Rising stack temperature at the same firing rate points to soot or scale.
- Routine tests follow a schedule, are done by procedure and are always logged.
- External inspections are in service; internal inspections need the boiler shut, isolated, drained, opened and cleaned.
- When in doubt, shut down safely and call the chief engineer.
- Handover
- The transfer of responsibility and information between shifts.
- Rounds
- Planned walks through the plant to check and record equipment condition.
- Log
- The written or electronic record of readings and events.
- Trend
- The direction a reading moves over time.
- External inspection
- An inspection of a boiler while it is in service.
- Internal inspection
- An inspection of a boiler opened up and out of service.
Practice problems
Work each problem on paper first, then reveal the answer to check.
What should a handover include?
Show answer
Equipment status, alarms and actions, lockouts, tests done and due, and planned work.
How is a mistake in the log corrected?
Show answer
Crossed out with a single line and initialed, never erased.
What might a rising stack temperature at the same firing rate mean?
Show answer
Soot on the fire side or scale on the water side.
What must happen if a low water cutoff fails its test?
Show answer
Take the boiler off line or keep it under constant attendance, and report at once.
Why is a boiler treated as a confined space during internal inspection?
Show answer
It is an enclosed space where the atmosphere may be hazardous.
Lesson quiz · 5 questions
Score 60% or more to complete this lesson.
Create a free account to save your progress, take quizzes and earn a certificate.