
WLD-340 · Lesson 10 of 12 · 18 min
Codes, inspection and qualification review
Lucia Ferreira, Hartwell's welding inspector, takes week eight. Codes and inspection run through every test Devon will take: the procedure he welds to on test day, the visual criteria the inspector applies to his coupon, and the bend acceptance limits that decide whether he passes. School finals give them a block of their own. Lucia counts the questions in the group's practice bank that need code knowledge to answer and finds about one in eight. She reviews WLD-330 with the group, not clause by clause, but by the kinds of decisions a journey-level welder makes with a code open on the bench.
Which document governs
The first decision on any job is which document applies. A code becomes law when a regulation or ordinance adopts it, or binding when a contract calls it up. For structural steel in the United States the welding code is AWS D1.1, called up by the AISC specification and the building code, with D1.5 for highway bridges; for pressure equipment the construction codes are the ASME Boiler and Pressure Vessel Code and the B31 piping codes, enforced by the states that adopt them; for pipelines the welding standard is API 1104 under federal pipeline safety rules. The edition matters: the contract or the regulation names it, and a newer edition does not apply to a job until it is adopted. When documents conflict, the project specification sets an order of precedence, and anything still unclear goes to the engineer as a written request for information.
Exam questions on this test words as much as rules. Shall means a requirement; should means a recommendation; may means a permission. A standard says how to do something; a code says what must be done and is written to be adopted; a specification is the owner's requirements for one project. Recommended practices guide but do not require. An inspector applies the acceptance criteria the code sets; an engineer can approve alternatives the code allows the engineer to approve. Questions that ask who decides are usually testing that difference.
Procedures and their records
A welding procedure tells the welder how to make a weld; a record of a test proves the procedure works. Under AWS D1.1, a WPS can be prequalified, if every variable is within the code's prequalification limits, or qualified by test, with a procedure qualification record behind it. Under ASME Section IX for pressure work, every WPS is supported by a PQR, which records the variables actually used in a test weld and the results of its tests. Essential variables are the ones that, if changed beyond the PQR's range, require a new qualification.
Worked problem
Is the procedure still valid?
A PQR for a carbon steel groove weld records a test coupon 1 in thick, welded with a heat input of 40 kJ/in, with impact tests at the required temperature. The WPS written from it allows base metal from 3/16 to 2 in and heat input up to 40 kJ/in. A welder on the Coldwater flanges is running 48 kJ/in on a 1 1/2 in flange. Is the weld inside the procedure?
Show solution
- Thickness: 1 1/2 in is inside the qualified range, so that is fine.
- Heat input: when impact tests are required, an increase in heat input above the PQR is an essential variable, because higher heat lowers HAZ toughness.
- 48 kJ/in is above the 40 kJ/in the PQR supports.
- Stop, report it, and have the welding engineer decide whether the welds made need evaluation; adjust travel speed or current to bring heat input back in range.
Answer: No. The heat input is outside the qualified range for an impact-tested procedure. This was the Coldwater flange issue in WLD-330 lesson 4.
Welder qualification and continuity
A welder's qualification is separate from the procedure's. It depends on the process, the position, the type of joint, backing, the filler group, deposited thickness and, for pipe, the diameter. Groove tests cover fillets in the positions they qualify; fillet tests cover only fillets. Plate tests in the vertical and overhead positions together qualify all plate positions; the 6G pipe test qualifies all positions on plate and pipe within its diameter range. A small-diameter test is needed for small pipe.
Qualifications must be kept up. Under D1.1 and Section IX, a qualification stays in force while the welder keeps using the process, and it lapses after six months without that process; AWS Certified Welder cards stay active through continuity reports. Every weld record names its welder so continuity can be proved. Kofi's case in WLD-330's capstone, welding vertical gussets with only flat and horizontal qualifications, is the kind of situation test questions describe: what should happen? Stop the work, assess the welds already made, qualify the welder or replace him, and fix the system that let it happen.
Visual inspection and acceptance
Visual inspection happens before, during and after welding. Before: the drawing, procedure, materials, joint preparation, fit-up, cleanliness, preheat and the welder's qualification. During: interpass temperature, cleaning, bead placement, consumables and heat input. After: size, length, profile, undercut, porosity, cracks and the finish. Good light, often 1,000 lux or 100 footcandles at the surface, and the eye close to the weld at a reasonable angle are part of the method. Gauges check fillet size, throat, reinforcement, undercut depth and misalignment.
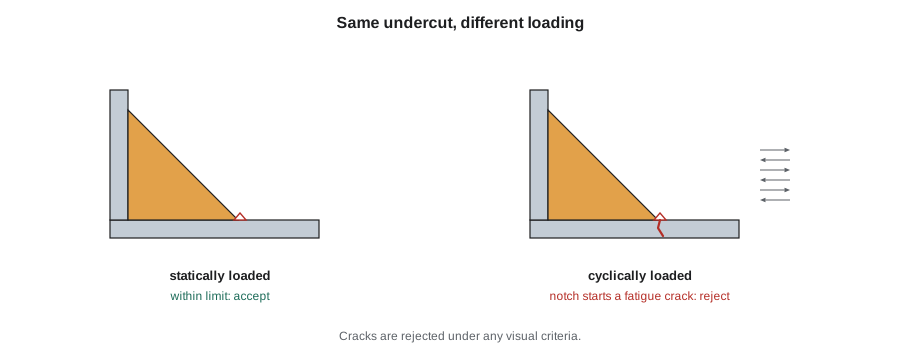
Acceptance criteria differ by code and by loading. Statically loaded structures accept some undercut and some porosity that cyclically loaded ones do not, because fatigue cracks start at small notches. Cracks are not acceptable under any visual criteria. Fillets may be undersize for a small part of their length within limits. Reinforcement on groove welds is limited, and on cyclically loaded joints it may need to be ground flush. The numbers come from the code's tables, and exam questions that give numbers usually provide the table, so the skill is reading it correctly. WLD-330 lessons 6 and 7 cover the criteria and the defects.
# Visual acceptance check, illustrative limits only (use the code's table for real work)
LIMITS = {'static': {'undercut': 0.03125, 'porosity': 0.375, 'undersize': 0.10}, 'cyclic': {'undercut': 0.01, 'porosity': 0, 'undersize': 0.10}}
welds = [('S-11', 'static', 0.02, 0.25, False, 0.05), ('S-12', 'static', 0.04, 0.125, False, 0.0), ('F-3', 'cyclic', 0.02, 0, False, 0.0), ('F-4', 'cyclic', 0.008, 0.0625, False, 0.0), ('G-7', 'static', 0.0, 0, True, 0.0)]
for name, loading, undercut, porosity_sum, crack, undersize_frac in welds:
    lim = LIMITS[loading]
    reasons = []
    if crack:
        reasons.append('crack')
    if undercut > lim['undercut']:
        reasons.append(f'undercut {undercut} > {lim["undercut"]}')
    if porosity_sum > lim['porosity']:
        reasons.append(f'porosity {porosity_sum} > {lim["porosity"]}')
    if undersize_frac > lim['undersize']:
        reasons.append(f'undersize over {lim["undersize"]:.0%} of length')
print(f"{name:<10} {loading:<8} {'REJECT: ' + ', '.join(reasons) if reasons else 'accept'}")S-11 static accept S-12 static REJECT: undercut 0.04 > 0.03125 F-3 cyclic REJECT: undercut 0.02 > 0.01 F-4 cyclic REJECT: porosity 0.0625 > 0 G-7 static REJECT: crack
The limits in the program are invented to show the logic, not taken from any code, in inches. The same 0.02 in of undercut is accepted on a statically loaded weld and rejected on a cyclically loaded one. Any crack rejects a weld whatever else it shows. And a small amount of porosity on a cyclically loaded weld fails where the static limit would have passed it.
Non-destructive examination
The four common methods each have a place. Visual testing comes first, always. Penetrant testing finds surface-breaking discontinuities on any non-porous material: clean, apply penetrant, wait the dwell time, remove the excess, apply developer, inspect. Magnetic particle testing finds surface and slightly subsurface discontinuities in ferromagnetic steel, best when the magnetic field crosses the indication, so it is done in two directions at right angles. Radiography shows the inside of the weld on film or a digital detector: porosity and slag show dark, tungsten shows light, and planar defects such as lack of fusion show only if they line up with the beam. Ultrasonic testing sends sound into the weld and reads echoes; it finds planar defects well, measures their depth, and needs a trained technician to interpret. Exam questions ask which method suits which defect and material.
| Method | Finds | Works on | Limits |
|---|---|---|---|
| Visual | Surface size, profile, undercut, visible cracks | All | Only what can be seen |
| Penetrant | Surface-breaking cracks and porosity | Non-porous metals including stainless and aluminum | Surface must be clean and open |
| Magnetic particle | Surface and near-surface cracks | Ferromagnetic steels only | Needs two directions; not for austenitic stainless or aluminum |
| Radiography | Volumetric defects: porosity, slag, tungsten | All | Radiation hazard; planar defects only if aligned with the beam |
| Ultrasonic | Planar defects: lack of fusion, cracks | Most metals, best on thicker sections | Needs skilled interpretation and coupling |
Personnel are certified for these methods. In the United States, NDT technicians are usually certified by their employers under ASNT's recommended practice SNT-TC-1A or under the CP-189 standard, and welding inspectors by AWS as Certified Welding Inspectors. A welder taking an AWS test does not need to know the certification steps in detail, but should know who signs what: the inspector accepts or rejects against the code; the NDT technician reports indications; the engineer decides on alternatives.
Lucia ends with a scenario each. Mateo gets a crater crack found by penetrant on a stainless weld: remove it by grinding, confirm it is gone with penetrant, reweld to the procedure and reinspect. Aisha gets a radiograph with a long dark line at the root: probably incomplete penetration or lack of root fusion, rejected, gouged out and repaired. Jun gets a welder who has not used gas tungsten arc for seven months: his Section IX qualification for that process has lapsed, so he retests before welding. Devon gets an RFI question: the drawing shows a fillet size below the code minimum for the plate thickness. Write it up and send it to the engineer; do not weld either size until the answer comes back. All four answers are right, and Lucia says that is the point of reviewing by decision rather than by clause.
Repairs and records
When a weld is rejected, the repair is part of the code's process, not an improvisation. The defect is located, removed by gouging or grinding, and the excavation is checked, often with magnetic particle or penetrant testing, to confirm it is gone. The repair is welded to a procedure, which may be the original procedure or a repair procedure, by a qualified welder, with the same preheat and interpass control. It is then re-examined by the method that found the defect. Codes limit the number of repairs at one location, and a second failure at the same spot usually needs the engineer's approval for anything more. Each step is recorded: what was found, how it was removed, how the removal was checked, who rewelded it and what the re-examination showed.
Records are the other half of inspection. A complete weld record links the weld number on the weld map to the procedure, the welder, the date, the inspection results and any repairs. Mill test reports tie the material to its heat number. Filler certificates tie the consumables to their classification. Calibration records show that gauges, meters and ovens were accurate. When Lucia audited Hartwell's own system in WLD-330, most of her findings were about records, not welds, and that is typical. Exam questions on documents usually ask which record answers which question, and the answer is almost always the one closest to the thing being asked about.
Lucia's final point is about responsibility. The welder is responsible for welding to the procedure and reporting problems; the inspector for checking against the code; the supervisor for assigning qualified welders; the engineer for design and approving alternatives. A good journey-level welder knows where each line falls and does not cross it either way: not accepting his own rejected weld, and not keeping quiet about a problem because it is someone else's job.
Common mistakes
MistakeTreating should as a requirement.
InsteadShall is required; should is recommended; may is permitted.
MistakeUsing the newest code edition on a job because it is newest.
InsteadUse the edition the contract or regulation names.
MistakeChanging heat input on an impact-tested procedure without checking the PQR.
InsteadHeat input above the PQR is an essential variable when toughness is required.
MistakeUsing magnetic particle testing on austenitic stainless steel.
InsteadIt is not ferromagnetic; use penetrant.
MistakeAccepting a small crack because it is short.
InsteadCracks are rejectable under visual criteria regardless of length.
Summary and key terms
- Codes gain force through adoption or contract; the named edition applies; conflicts go to the engineer in writing.
- Procedures are prequalified or qualified by PQR; essential variables limit their range.
- Welder qualifications depend on process, position, joint, backing, filler, thickness and diameter, and lapse without continuity.
- Visual inspection runs before, during and after welding with good light and gauges.
- Cyclically loaded welds have stricter limits than statically loaded ones; cracks always reject.
- Penetrant for surface defects on any metal, magnetic particle for ferritic steel, radiography and ultrasonics for internal defects.
- Order of precedence
- The ranking that decides which document governs when documents conflict.
- Essential variable
- A variable whose change beyond the qualified range requires a new qualification.
- PQR
- Procedure qualification record: the record of a test weld and its results.
- Continuity
- Evidence that a welder has kept using a process, which keeps a qualification in force.
- Dwell time
- The time penetrant stays on the surface before the excess is removed.
- RFI
- Request for information: a written question to the engineer about a drawing or specification.
Practice problems
Work each problem on paper first, then reveal the answer to check.
A welder passed a 3G groove test on plate. Can he weld a horizontal fillet?
Show answer
Usually yes: a groove test qualifies fillet welds in the positions it covers. Check the code's table for exactly which fillet positions a 3G test includes.
Which NDE method would you use to check a stainless steel crater for cracks?
Show answer
Liquid penetrant.
A drawing calls for a weld size the code does not allow. What do you do?
Show answer
Write an RFI to the engineer and wait for a written answer.
Lesson quiz · 5 questions
Score 60% or more to complete this lesson.
Create a free account to save your progress, take quizzes and earn a certificate.