
HSE-333 · Lesson 5 of 12 · 26 min
Hot work and gas testing in hydrocarbon and sour service
Hot work in an oil and gas facility brings an ignition source into a place built to contain flammable gas. HSE-216 covers hot work in general, including how hot work starts fires, protecting combustibles, gas testing near tanks and containers, and the fire watch. HSE-330 covered gas detectors: how sensors work, their limits, bump testing, calibration and alarm set points. This lesson puts the two together for the conditions of a battery, compressor station or sour gas plant, and shows how gas testing becomes a control within the permit rather than a box on the form.
First question: does it have to be hot work?
The safest hot work is the hot work that never happens. Before issuing a hot work permit in a process area, the planner should ask whether the job can be done another way. Many tasks that were once welded can now be done cold:
- cutting pipe with cold-cutting saws, abrasive water jets or pipe cutters instead of torches;
- joining with mechanical couplings, flanged connections or bolted clamps instead of welds, where the design and code allow;
- removing bolts with hydraulic tools or nut splitters instead of cutting them off;
- prefabricating spools and supports in a shop or outside the classified area and bringing them in for bolting;
- scheduling the work during a planned shutdown when the area can be cleared of hydrocarbons.
If hot work is still needed, the next question is whether it can be moved out of the classified area or whether the area around it can be made gas-free, isolated and kept that way for the whole job.
Where gas comes from during hot work
A gas test at the start of a job only shows conditions at that moment. In an operating facility, gas can arrive at the hot work site from many sources while the work is going on:
- equipment being worked on that was not fully drained, purged or cleaned, including scale, sludge and liners that release vapor when heated;
- passing valves, open drains and vents on nearby equipment;
- tank hatches, vapor recovery headers and connected tanks, as at Partridge-Raleigh;
- sewers, drain hubs, catch basins and trenches, where heavier-than-air vapor collects;
- relief and blowdown discharges and flare knockout drums;
- leaks from flanges, packing and seals that change with pressure and temperature;
- process upsets elsewhere in the plant, which can release gas with little warning.
Wind matters too. A light wind can carry gas from a leaking flange 65 ft (20 m) away onto the welding bench, and a calm, cold morning can let vapor settle in low spots that were clear at noon the day before.
Where and in what order to test
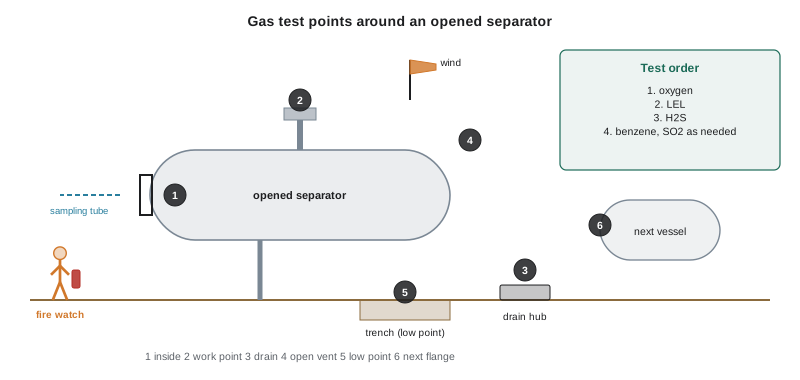
Gas tests for hot work are taken at the work point and at every place gas could come from: inside the equipment if it has been opened, at nearby drains and openings, at low points and inside any nearby enclosure or shelter. Tests inside equipment use a sampling pump and tube so the tester does not have to enter or lean in. The usual order is oxygen first, because a low oxygen reading means flammable and toxic readings may be wrong; then flammable gas as percent of the lower explosive limit (LEL); then hydrogen sulfide and any other toxic gas expected, such as benzene near condensate tanks or sulfur dioxide near the sulfur plant. The detector should be bump-tested before use, and the tester should allow enough sampling time for gas to reach the sensors through the tube.
Acceptance criteria
Each company sets its own acceptance criteria in its hot work and permit standards, usually stricter than the legal minimum. The table shows criteria of the kind many oil and gas companies use. They are illustrative only; always use the values in your site's standard.
| Reading | Illustrative criterion for hot work | Why |
|---|---|---|
| Oxygen | 19.5 to 23 percent | Low oxygen means displaced air and unreliable LEL readings; high oxygen makes fires far more intense |
| Flammable gas | 0 percent LEL at the work point and openings for open flame; low single digits for spark-producing work only where the standard allows | Any detectable flammable gas means a source nearby that could grow |
| Hydrogen sulfide | Below the site action level, often 5 to 10 ppm, with breathing apparatus required above it | Sour service can release H2S at the work point; welding fumes do not mask it from detectors but do from noses |
| Benzene | Below the site action level with a tube or photoionization detector | Condensate and tank work can release benzene, a carcinogen |
| Continuous monitoring | Personal and area monitors running for open-flame work, alarms set to stop work | Conditions change during the job |
How often to retest
Retesting is where many hot work permits break down. Company standards usually require a test immediately before work starts, a retest after any break longer than a set time, retesting at set intervals during the job, continuous monitoring for open-flame work in process areas, and an immediate retest when conditions change: a wind shift, a process upset, a new job starting nearby, or anyone smelling gas. The program below works through a day of readings from the hot work site at Kettle Creek and flags when a retest was missed or a reading failed.
# Check a day of hot work gas tests against illustrative criteria and a 2-hour retest rule.
LIMITS = {"O2_low": 19.5, "O2_high": 23.0, "LEL": 0.0, "H2S": 5.0}   # illustrative
MAX_GAP_MIN = 120
tests = [  # (time hh:mm, O2 %, LEL %, H2S ppm, note)
    ("07:40", 20.9, 0, 0, "pre-start, work point and drains"),
    ("09:35", 20.9, 0, 0, "after coffee break"),
    ("12:20", 20.9, 0, 1, "after lunch"),
    ("13:05", 20.8, 3, 2, "wind shifted to the south"),
    ("13:30", 20.9, 0, 0, "after leaking flange tightened"),
    ("15:20", 20.9, 0, 0, "mid-afternoon"),
    ("16:10", 20.9, 0, 0, "end of welding"),
]

def minutes(t):
    h, m = map(int, t.split(":"))
    return 60 * h + m

prev = None
for t, o2, lel, h2s, note in tests:
    problems = []
    if not LIMITS["O2_low"] <= o2 <= LIMITS["O2_high"]:
        problems.append("oxygen out of range")
    if lel > LIMITS["LEL"]:
        problems.append(f"LEL {lel} % - stop hot work")
    if h2s > LIMITS["H2S"]:
        problems.append("H2S above action level")
    if prev is not None and minutes(t) - prev > MAX_GAP_MIN:
        problems.append(f"gap of {minutes(t) - prev} min exceeds {MAX_GAP_MIN}")
    status = "; ".join(problems) if problems else "ok"
    print(f"{t}  O2 {o2:4.1f}  LEL {lel:>2}  H2S {h2s:>2}  {note:<36} {status}")
prev = minutes(t)07:40 O2 20.9 LEL 0 H2S 0 pre-start, work point and drains ok 09:35 O2 20.9 LEL 0 H2S 0 after coffee break ok 12:20 O2 20.9 LEL 0 H2S 1 after lunch gap of 165 min exceeds 120 13:05 O2 20.8 LEL 3 H2S 2 wind shifted to the south LEL 3 % - stop hot work 13:30 O2 20.9 LEL 0 H2S 0 after leaking flange tightened ok 15:20 O2 20.9 LEL 0 H2S 0 mid-afternoon ok 16:10 O2 20.9 LEL 0 H2S 0 end of welding ok
Two problems stand out. The gap between the after-lunch test at 12:20 and the 09:35 test was 165 minutes, longer than the two-hour rule, so either a test was missed or it was not recorded. And at 13:05 the wind shifted, the work point read 3 percent LEL and the crew had to stop welding until the source, a leaking flange upwind, was found and tightened. On a continuous monitor, that reading would have sounded an alarm without waiting for the tester. This is exactly the kind of change that a single pre-start test cannot catch.
Sour service and hot work
Hot work on equipment that has been in sour service has extra hazards. Iron sulfide scale inside piping and vessels can be pyrophoric, glowing or igniting when it dries out in air, and heating it can release sulfur dioxide. Scale, sludge and porous materials can hold H2S and release it when heated or disturbed, so a vessel that tested clear before welding can produce H2S once the arc starts. Welders working on or near sour equipment need personal H2S monitors, a plan for breathing apparatus, and in many companies a requirement that the equipment be steamed, water-washed or chemically cleaned before any hot work on it. HSE-332 covered pyrophoric iron sulfide and the chemicals of sour plants.
Hot work in live plants: habitats and in-service welding
Sometimes hot work must be done in an area that cannot be shut down, such as a tie-in beside a running compressor. Two specialized methods are used under strict procedures.
- Pressurized welding enclosures, often called habitats, are fire-resistant enclosures built around the work and kept at a slight positive pressure with air drawn from a safe location. Gas detectors at the air intake and inside the enclosure automatically shut off the welding power and alarm if gas is detected. They allow welding in a classified area, but only when designed, installed, tested and monitored by trained people.
- In-service welding and hot tapping weld onto pipe or vessels that are still under pressure and flowing. They require engineering of the weld procedure to avoid burn-through and cracking, verification of wall thickness, and specialist crews. As Lesson 2 noted, hot taps under documented procedures are excluded from OSHA's lockout standard in the US; in both countries they are a specialized activity, not ordinary hot work.
The fire watch in oil and gas
The fire watch's job does not change from HSE-216: watch for sparks and smoldering, keep extinguishing equipment ready, stop the work and raise the alarm if needed, and stay after the work ends. In oil and gas facilities, the fire watch also often carries a multi-gas monitor, watches for gas alarms and process changes, and knows how to activate the emergency shutdown or plant alarm. Fire watches should have no other task, and in many companies they must remain for at least 30 to 60 minutes after hot work ends, longer where insulation, sludge or scale could smolder.
Worked problem
Planning a weld on the Kettle Creek scrubber outlet
A support bracket on the outlet piping of the Kettle Creek inlet scrubber has cracked and must be rewelded. The scrubber is in sour gas service and the station will keep running on the second compressor. How should the hot work be planned?
Show solution
- Ask whether the bracket can be replaced with a bolted clamp; if not, whether the weld can wait for the next planned outage.
- If the weld must proceed now, confirm the bracket weld is on a non-pressure attachment, check wall thickness at the weld location and get engineering approval for welding near the pressure piping.
- Survey sources: nearby drains, the scrubber relief and drain lines, the running compressor's packing vents and the station flare knockout; cover drain hubs and confirm the leak survey is current.
- Test oxygen, LEL and H2S at the work point and each source, set up continuous area and personal monitors, and set the retest rule and stop criteria on the permit.
- Assign a dedicated fire watch with a multi-gas monitor and extinguisher who knows the station shutdown, and keep the watch in place after welding until the site standard's time has passed.
Answer: Look first for a way to avoid hot work, then control every gas source within reach, monitor continuously and keep a dedicated fire watch, because the station is live and sour.
Common mistakes
MistakeTesting once before work starts and relying on that result all day.
InsteadRetest at set intervals, after breaks and whenever conditions change, and use continuous monitoring for open-flame work.
MistakeTesting only at the work point.
InsteadTest at the work point and every nearby opening, drain, low point and connected vessel.
MistakeTesting LEL before oxygen.
InsteadTest oxygen first so you know whether the LEL reading is reliable.
MistakeWelding on sour equipment straight after it tested clear.
InsteadClean or neutralize sour scale first and monitor for H2S once heating starts.
MistakeGiving the fire watch other jobs.
InsteadKeep the fire watch dedicated, equipped with a gas monitor and ready to stop the work.
Summary and key terms
- Ask first whether the job can be done cold, outside the classified area or during a shutdown.
- Gas can reach hot work from the equipment, nearby openings, drains, connected tanks, leaks and upsets, carried by wind or settling in low spots.
- Test oxygen first, then LEL, then H2S and other toxics, at the work point and every source, using a bump-tested detector.
- Acceptance criteria are set by the company standard and are usually stricter than the law, often 0 percent LEL for open flame.
- Retest after breaks, at set intervals and whenever conditions change, and use continuous monitoring for open-flame work.
- Sour equipment adds pyrophoric scale and H2S release on heating, so it is cleaned and monitored before and during hot work.
- Habitats and in-service welding allow hot work in live plants only under specialist procedures, and the fire watch stays dedicated and stays after the work.
- Cold cutting
- Cutting metal without heat sufficient to ignite gas, such as with saws or water jets.
- Lower explosive limit
- The lowest concentration of a gas in air that can burn; gas tests report flammable gas as a percentage of it.
- Bump test
- A brief exposure of a detector to a known gas to confirm its sensors and alarms respond.
- Continuous monitoring
- Gas detection that runs throughout the work, with alarms to stop the job.
- Pressurized welding enclosure
- A habitat around hot work kept at positive pressure with gas detection that shuts off welding power.
- In-service welding
- Welding onto equipment that is still under pressure and flowing.
- Pyrophoric
- Able to ignite spontaneously in air, as iron sulfide scale can when it dries.
- Fire watch
- A dedicated person who watches for fire during and after hot work.
Practice problems
Work each problem on paper first, then reveal the answer to check.
Name three ways to avoid hot work on a pipe repair.
Show answer
Any three of: cold cutting, mechanical couplings or clamps, hydraulic bolt removal, shop prefabrication, waiting for a shutdown.
List four places gas can come from during hot work in a facility.
Show answer
Any four of: the equipment itself, passing valves, open drains and vents, tank hatches and headers, sewers and trenches, relief discharges, leaks, process upsets.
Why is oxygen tested first?
Show answer
Low oxygen means flammable and toxic readings may be unreliable.
What LEL criterion do many companies use for open-flame hot work?
Show answer
Zero percent LEL at the work point and openings.
In the program, which gap between tests broke the two-hour rule?
Show answer
The 165 minutes between 09:35 and 12:20.
What did the 13:05 reading show and what was done?
Show answer
Three percent LEL after a wind shift; welding stopped until a leaking flange was tightened.
Why can a sour vessel that tested clear release H2S during welding?
Show answer
Scale and sludge can hold H2S and release it when heated.
What does a pressurized welding enclosure do when it detects gas?
Show answer
It shuts off welding power and alarms.
Why is a hot tap not ordinary hot work?
Show answer
It welds onto live, pressurized equipment and needs engineered procedures and specialist crews.
Give two extra duties of a fire watch in an oil and gas facility.
Show answer
Any two of: carry a gas monitor, watch for gas alarms and process changes, know how to activate the shutdown or alarm.
Lesson quiz · 5 questions
Score 60% or more to complete this lesson.
Create a free account to save your progress, take quizzes and earn a certificate.