
HSE-311 · Lesson 10 of 12 · 25 min
Mechanical integrity and inspection
Most major process accidents end in a loss of containment: something that should have held the hazardous material inside failed. Vessels, piping, tanks, relief devices, pumps, instruments and emergency shutdown systems all deteriorate with time and use. Mechanical integrity is the part of process safety management that keeps this equipment fit for service through design, inspection, testing, maintenance and repair. This lesson explains common damage mechanisms, how inspection programs are planned, how remaining life and inspection intervals are estimated, and how deficiencies are handled. It draws on two accidents investigated by the US Chemical Safety Board, at Tesoro Anacortes in 2010 and at Chevron Richmond in 2012.
Which equipment is covered
A mechanical integrity program covers equipment whose failure could cause or fail to prevent a major accident. The list usually includes pressure vessels and storage tanks, piping systems and their components, relief and vent systems, emergency shutdown systems, controls including monitoring devices, sensors, alarms and interlocks, and pumps and compressors. Each item needs written procedures for inspection, testing and maintenance, trained people to do the work, and records of what was found.
In Canada, pressure equipment is regulated provincially under boilers and pressure vessels legislation, administered by bodies such as the Technical Standards and Safety Authority (TSSA) in Ontario, ABSA in Alberta and Technical Safety BC. These regulators adopt CSA B51, Boiler, pressure vessel, and pressure piping code, which in turn references ASME codes for design. Owners must register designs, hold certificates of inspection and in many provinces may operate an approved owner-user inspection program. CSA Z767 places mechanical integrity under its asset integrity element, and pipeline regulators such as the Canada Energy Regulator and the Alberta Energy Regulator have their own integrity management requirements for pipelines, typically referencing CSA Z662.
Damage mechanisms
Inspection is only useful if inspectors know what to look for and where. Damage mechanisms depend on the material, the fluid, the temperature, the pressure and the history of the equipment. API RP 571 describes more than 60 mechanisms affecting equipment in the refining and petrochemical industry. A few common ones are summarized below.
| Mechanism | What happens | Where it is common |
|---|---|---|
| General corrosion | Uniform metal loss over a large area | Carbon steel in water, acids or wet gases |
| Localized corrosion and pitting | Deep, narrow attack in small areas | Stagnant areas, under deposits, dead legs |
| Corrosion under insulation (CUI) | Corrosion of steel hidden beneath wet insulation | Lines and vessels operating between roughly −12 °C and 177 °C (carbon steel) |
| Sulfidation | Metal loss from sulfur compounds at high temperature; faster in low-silicon carbon steel | Refinery crude and hydroprocessing units |
| High temperature hydrogen attack (HTHA) | Hydrogen reacts with carbon in steel, forming methane and fissures | Hot hydrogen service in refinery units |
| Stress corrosion cracking | Cracks from combined tensile stress and a corrosive environment | Caustic, chloride or ammonia service |
| Fatigue | Cracks from repeated stress cycles | Vibrating small-bore piping, cycling vessels |
| Erosion | Metal loss from high-velocity flow or particles | Elbows, control valves, slurry service |
Two accidents
On 2 April 2010, a heat exchanger in the naphtha hydrotreater unit at the Tesoro refinery in Anacortes, Washington, ruptured during a startup step. The release of hydrogen and naphtha ignited and killed seven workers. The CSB found that the exchanger had been weakened by high temperature hydrogen attack. The carbon steel exchanger had been operating in conditions where HTHA was possible, and industry guidance for avoiding it, the Nelson curves in API RP 941, had been shown by incidents to be unreliable for carbon steel. The CSB also noted that the exchangers had a history of leaks during startup that workers had come to see as normal.
On 6 August 2012, a pipe carrying hot light gas oil in the crude unit at the Chevron refinery in Richmond, California, ruptured because of sulfidation corrosion. The pipe had thinned severely, particularly in sections of low-silicon carbon steel, which corrodes much faster in sulfidation service. The released oil formed a large vapour cloud that ignited; 19 workers escaped the cloud, and around 15,000 people from the surrounding community sought medical treatment. The CSB found that recommendations to inspect every component of the line, or to upgrade to more resistant alloy, had been made over the years but not acted on, and that inspection points had missed the thinnest components.
| Lesson from these accidents | Practical response |
|---|---|
| Damage can be invisible to normal inspection points | Choose inspection locations based on the damage mechanism, not convenience |
| Material differences matter | Verify materials (positive material identification) and inspect low-resistance components |
| Industry guidance can be wrong | Use inherently safer materials where the mechanism is severe and poorly predicted |
| Recurring leaks are warnings | Investigate repeated leaks rather than accepting them as normal |
| Recommendations need follow-through | Track integrity recommendations to completion with management oversight |
Planning inspections
Inspection programs used to be based on fixed time intervals. Modern programs increasingly use risk-based inspection (RBI), which ranks equipment by the probability of failure, from its damage mechanisms and condition, and the consequence of failure, from the fluid, inventory and location. High-risk items are inspected more often and with methods suited to the expected damage; low-risk items less often. API RP 580 sets out the principles of RBI, and API RP 581 gives a quantitative method. Inspection codes such as API 510 for pressure vessels, API 570 for piping and API 653 for aboveground storage tanks set rules for inspection, repair and alteration in the oil and petrochemical sectors.
| Inspection method | Detects | Notes |
|---|---|---|
| Visual inspection | External corrosion, leaks, damaged supports and insulation | Cheap and fast; misses internal damage |
| Ultrasonic thickness measurement | Wall thinning at a point | Only as good as the location chosen |
| Ultrasonic scanning and phased array | Thinning over an area, cracks | More coverage, needs skilled technicians |
| Radiography | Wall loss, deposits, weld defects | Radiation safety controls needed |
| Magnetic particle and dye penetrant | Surface cracks | Needs surface access and cleaning |
| Pulsed eddy current and guided wave | Wall loss through insulation or over long lengths | Screening methods; follow up with detailed checks |
Corrosion rate, remaining life and inspection interval
Thickness measurements taken at the same points over time give a corrosion rate. The minimum required thickness, from the design code and the operating pressure, sets the limit. The remaining life is the margin above minimum divided by the corrosion rate.
A common rule in inspection codes such as API 510 and API 570 is that the next inspection should take place at no more than half the remaining life, subject to maximum intervals. This leaves time for at least one more measurement before the limit is reached, so that an unexpected increase in corrosion rate can be caught.
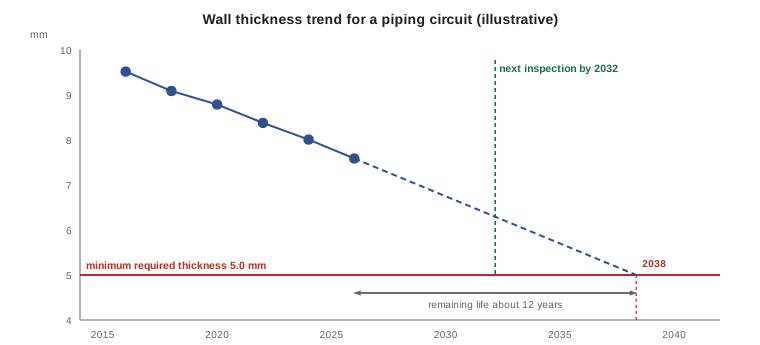
# Corrosion rate, remaining life and inspection interval for a piping circuit (seeded data).
import random
random.seed(311)
years = list(range(2016, 2027, 2))
true_rate = 0.19   # mm/yr
t0 = 9.5
readings = [round(t0 - true_rate * (y - years[0]) + random.gauss(0, 0.05), 2) for y in years]
for y, t in zip(years, readings):
    print(f"{y}: {t:.2f} mm")

# Long-term rate from first and last readings, short-term rate from the last two
lt_rate = (readings[0] - readings[-1]) / (years[-1] - years[0])
st_rate = (readings[-2] - readings[-1]) / (years[-1] - years[-2])
rate = max(lt_rate, st_rate)        # use the more conservative rate
t_min = 5.0
remaining = (readings[-1] - t_min) / rate
print(f"Long-term rate {lt_rate:.3f} mm/yr, short-term rate {st_rate:.3f} mm/yr")
print(f"Remaining life {remaining:.1f} years using {rate:.3f} mm/yr")
print(f"Next inspection no later than {years[-1] + remaining / 2:.1f}")2016: 9.52 mm 2018: 9.09 mm 2020: 8.79 mm 2022: 8.38 mm 2024: 8.01 mm 2026: 7.59 mm Long-term rate 0.193 mm/yr, short-term rate 0.210 mm/yr Remaining life 12.3 years using 0.210 mm/yr Next inspection no later than 2032.2
Using the higher of the long-term and short-term rates is a conservative choice that guards against an accelerating trend. The calculation is only as good as the inspection locations: if the thinnest point is never measured, as at Chevron Richmond, the remaining life will be overestimated.
Worked problem
Calculating remaining life
A pressure vessel shell was 12.0 mm thick when installed in 2012 and measured 10.6 mm in 2026. The minimum required thickness is 8.5 mm. Estimate the corrosion rate, remaining life and latest next inspection date using the half-life rule.
Show solution
- Corrosion rate = (12.0 − 10.6) / (2026 − 2012) = 1.4 / 14 = 0.10 mm per year.
- Remaining life = (10.6 − 8.5) / 0.10 = 21 years.
- Half the remaining life = 10.5 years.
- The next inspection should be no later than mid-2036, or earlier if the applicable code or the site's RBI plan sets a shorter maximum interval.
Answer: About 0.10 mm per year, 21 years of remaining life and an inspection no later than about 10 years from now, subject to code maximums.
Deficiencies, quality assurance and the integrity operating window
When an inspection finds equipment outside acceptable limits, the deficiency must be corrected before further use, or the equipment must be operated under documented temporary measures that keep it safe until repair, such as a lower pressure limit and more frequent monitoring. Quality assurance makes sure that new equipment, spare parts and repairs are suitable for the service: for example, positive material identification to catch a carbon steel fitting installed in an alloy line. Integrity operating windows (IOWs) set limits on process variables, such as temperature, pH or chloride content, beyond which damage accelerates. Exceeding an IOW should trigger an alert to the integrity engineer, not only to operations, because the damage may not be visible until much later.
# Flag integrity operating window excursions in a day of hourly readings (seeded data).
import random
random.seed(11)
limits = {"outlet temperature C": (None, 345.0), "wash water pH": (6.0, 8.5)}
temps = [random.gauss(341, 3) for _ in range(24)]
ph = [random.gauss(7.2, 0.7) for _ in range(24)]
for name, series in [("outlet temperature C", temps), ("wash water pH", ph)]:
    lo, hi = limits[name]
    bad = [(h, v) for h, v in enumerate(series)
           if (lo is not None and v < lo) or (hi is not None and v > hi)]
    print(f"{name}: {len(bad)} excursion hours")
    for h, v in bad:
print(f" hour {h:02d}: {v:.1f}")outlet temperature C: 2 excursion hours hour 12: 345.6 hour 16: 348.7 wash water pH: 2 excursion hours hour 04: 5.9 hour 12: 9.5
Who does mechanical integrity work
Mechanical integrity depends on several groups working together. Inspectors, often certified under schemes such as the API individual certification programs or provincial and state inspector licensing, plan and carry out inspections and judge fitness for service. Maintenance technicians repair and test equipment, and need training in the procedures for the equipment they work on. Integrity or corrosion engineers set inspection strategies, review damage mechanisms and integrity operating windows, and approve deferrals. Operators are often the first to notice leaks, vibration or abnormal conditions, and their observations should feed into the program. Clear roles, and a single system for recording findings and tracking actions, stop deficiencies falling between these groups.
Common mistakes
MistakeMeasuring thickness at the same convenient points every time.
InsteadChoose locations based on the damage mechanism, including components most likely to thin.
MistakeTreating repeated leaks during startup as normal.
InsteadInvestigate recurring leaks as signs of damage.
MistakeUsing only the long-term average corrosion rate.
InsteadUse the more conservative of long-term and short-term rates.
MistakeLeaving integrity recommendations open for years.
InsteadTrack them to completion with management oversight.
MistakeAssuming spare parts are the right material.
InsteadUse positive material identification and quality assurance.
Summary and key terms
- Mechanical integrity keeps containment equipment and safeguards fit for service through inspection, testing and maintenance.
- Damage mechanisms such as corrosion, sulfidation, HTHA, cracking and fatigue determine what to inspect for and where.
- Tesoro Anacortes (2010) and Chevron Richmond (2012) show the cost of missed damage and unfollowed recommendations.
- Risk-based inspection focuses effort on equipment with the highest probability and consequence of failure.
- Remaining life is the thickness margin divided by the corrosion rate; inspect at no more than half the remaining life.
- Deficiencies must be corrected or controlled, and integrity operating windows warn when damage may be accelerating.
- Mechanical integrity
- Keeping process equipment fit for service through its life.
- Damage mechanism
- A process, such as corrosion or fatigue, that degrades equipment.
- Sulfidation
- High-temperature corrosion caused by sulfur compounds.
- HTHA
- High temperature hydrogen attack, damage to steel from hot hydrogen.
- CUI
- Corrosion under insulation.
- Risk-based inspection
- Planning inspections by the probability and consequence of failure.
- Minimum required thickness
- The thinnest wall that still meets the design code for the service.
- Remaining life
- The time until the wall reaches minimum required thickness at the current corrosion rate.
- Positive material identification
- Testing that confirms the material of a component.
- Integrity operating window
- Limits on process conditions that protect equipment from accelerated damage.
Practice problems
Work each problem on paper first, then reveal the answer to check.
Name four types of equipment typically covered by a mechanical integrity program.
Show answer
Pressure vessels, piping, relief systems, emergency shutdown systems (also tanks, controls, pumps).
What damage mechanism caused the Tesoro Anacortes exchanger rupture?
Show answer
High temperature hydrogen attack.
Why did low-silicon carbon steel matter at Chevron Richmond?
Show answer
It corrodes much faster in sulfidation service, so those components thinned most.
What is corrosion under insulation and why is it dangerous?
Show answer
Corrosion hidden beneath wet insulation, which is hard to see.
What two factors does RBI combine?
Show answer
Probability of failure and consequence of failure.
A pipe is 7.0 mm, the minimum is 5.0 mm and the corrosion rate is 0.25 mm per year. What is the remaining life?
Show answer
8 years.
Using the half-life rule, when should that pipe next be inspected?
Show answer
Within 4 years, or sooner if the code maximum is shorter.
Why use the more conservative of the long-term and short-term corrosion rates?
Show answer
To catch an accelerating trend.
What is an integrity operating window?
Show answer
A limit on a process variable beyond which equipment damage accelerates.
What should happen when equipment is found below minimum thickness?
Show answer
Correct it before further use, or operate under documented temporary measures until repair.
Lesson quiz · 5 questions
Score 60% or more to complete this lesson.
Create a free account to save your progress, take quizzes and earn a certificate.