
DCE-450 · Lesson 2 of 12 · 26 min
Commissioning levels, test scripts and documentation
Commissioning a data centre involves thousands of individual tests, from checking the torque on a single busbar bolt to failing the utility supply to the whole building. To keep this manageable, the industry organizes testing into levels, each building on the one before: equipment is proven at the factory, then on delivery and installation, then as individual systems, and finally as an integrated facility. This lesson describes the commissioning levels, what happens at each, how test scripts are written and executed, how to test safely around equipment that is being energized for the first time, how many of a set of identical units must be tested, and the documentation that records it all and passes it to the operators.
The five levels
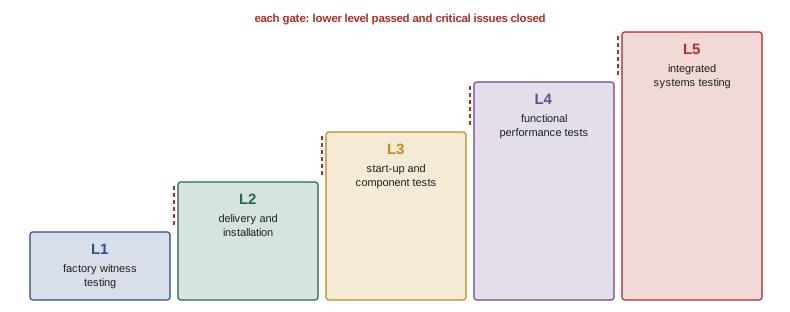
Most data centre projects use a five-level scheme. The exact names vary between owners and commissioning firms, but the progression is common:
| Level | Name | What is verified | Typical examples |
|---|---|---|---|
| L1 | Factory witness testing | Major equipment meets specification before shipping | UPS, switchgear, generators, chillers, transformers tested at the factory |
| L2 | Delivery and installation verification | Equipment arrives undamaged and is installed correctly | Receiving inspection, pre-functional checklists, torque checks, labelling |
| L3 | Start-up and component testing | Each piece of equipment starts and operates on its own | Vendor start-up, NETA acceptance tests, insulation resistance, relay settings |
| L4 | Functional performance testing | Each system performs all its functions, including failures, at design load | UPS on load bank with module failure, chiller plant staging, generator paralleling |
| L5 | Integrated systems testing | All systems work together through real failure scenarios | Utility failure with generator start, cooling recovery and BMS alarms |
Each level is a gate. Equipment that fails factory testing is not shipped; a system cannot be functionally tested until its components have passed start-up; integrated testing waits until every system has passed its functional tests and critical issues are closed (Lesson 1). This sequencing means that each level tests something new, rather than rediscovering problems a lower level should have caught.
Level 1: factory witness testing
Large, long-lead equipment is tested at the manufacturer's plant, witnessed by the owner's commissioning team, before it ships. Finding a problem at the factory is far cheaper than finding it on site, where repairs may need specialists flown in and equipment partly dismantled. Typical factory witness tests include running a UPS module at full load on the factory's load bank and through transfers to battery and bypass; testing switchgear wiring, interlocks and protective relays; load testing a generator set across its range; and running a chiller on a test stand at design conditions. The witness checks that the equipment matches the approved submittals (correct ratings, options and firmware), that tests follow the agreed procedure, and that results meet the specification.
Level 2: delivery and installation
On arrival, equipment is inspected for shipping damage (tilt and shock indicators on transformers and UPS cabinets are checked), compared with the order, and stored as the manufacturer requires, often in heated, dry space. After installation, pre-functional checklists verify that it was installed correctly: anchorage and seismic restraints, clearances for maintenance and arc-flash working space, cable sizes and terminations, torque marks on bolted connections, grounding and bonding, piping supports, valve orientation, labelling and access. Many problems that would otherwise surface during functional testing are caught here, such as a reversed flow sensor or a missing ground conductor.
Level 3: start-up and component testing
Level 3 brings each piece of equipment to life on its own. Electrical equipment receives acceptance tests to the NETA ATS standard (Lesson 3): insulation resistance, contact resistance, protective relay calibration, breaker trip tests and transformer turns ratio. Vendors start up their equipment according to their own procedures, and the commissioning team verifies controls point by point, confirming that each sensor reads correctly and each command moves the right device. Records of every result are kept, because they become the baseline for later maintenance testing.
Level 4: functional performance testing
Functional performance tests prove that each system performs all of its functions, at design load and under failure conditions, according to the sequences of operation. For a data centre this means testing systems with real heat and electrical load, usually provided by load banks before IT equipment is installed (Lesson 3). A UPS system is tested at full load with a module failed, on battery to verify runtime, and through bypass and maintenance transfers; a chiller plant is tested through staging up and down, failure of a chiller or pump, and restart after a power interruption (Lesson 4). Each test follows a script, and every deviation goes into the issues log.
Level 5: integrated systems testing
Integrated systems testing (IST) is the culmination: the whole facility, under simulated full IT load, is put through realistic failure scenarios, such as complete loss of utility power, to prove that electrical, mechanical, controls, monitoring and fire systems work together and that operators can respond. It is the subject of Lesson 5.
Writing test scripts
A test script (also called a test procedure or functional test) is a step-by-step procedure with expected results. A good script contains:
- Purpose and scope: what the test proves, and which requirement in the OPR it verifies.
- Prerequisites: lower-level tests completed, critical issues closed, documentation available, instruments calibrated.
- Safety: hazards, personal protective equipment, lockout points, arc-flash boundaries and emergency stops; and a statement that the test stops if any step creates an unsafe condition.
- Instruments and resources: load banks, power quality analysers, thermal cameras, data loggers, radios, and the people and roles needed.
- Initial conditions: the configuration of every relevant breaker, valve and control mode before the test begins.
- Steps: numbered actions, each with an expected result and space to record the actual result and pass or fail.
- Acceptance criteria: measurable limits, such as voltage within ±5 %, transfer time under 10 s, chilled water temperature recovered within 10 minutes.
- Restoration: steps to return the system to normal.
- Sign-off: names, dates and witness signatures.
Worked problem
A script step
Write two steps of a functional test that verifies a UPS module failure does not drop load, for a system of four 500 kW modules carrying 1,500 kW of load bank (N+1).
Show solution
- Step 12: Record initial load on each module (expected about 375 kW each), output voltage and frequency, and the load bank current. Start the power quality recorder on the critical bus.
- Step 13: Open the input and output breakers of module 2 using the vendor's procedure to simulate a module failure. Expected: load transfers to the remaining three modules with no interruption; each carries about 500 kW; output voltage remains within ±5 % and recovers within the manufacturer's transient specification; an alarm appears on the UPS display, the EPMS and the BMS within 10 s.
Answer: Each step names an action, the expected response and what to record. Acceptance is judged against numbers, not impressions, and the power quality recording provides objective evidence that the load saw no interruption. Note that the remaining modules now run at 100 % of rating, so the test also verifies that they can carry full load when the redundant module is lost.
Scripts are reviewed by the designers, vendors and operators before testing, and executed with a test director calling each step, a recorder writing results, and technicians performing actions. Steps that do not go as expected are stopped, recorded in the issues log, and resumed or rescheduled after the cause is understood. Deviations from the script are never improvised during a live test.
Testing safely
Commissioning is one of the most hazardous periods in a data centre's life: equipment is energized for the first time, construction workers are still present, labelling may be incomplete, and systems are deliberately pushed to failure. Safety controls include an energization plan that defines when each part of the system is live and how that is communicated (signs, barriers, daily briefings), strict lockout and tagging, arc-flash studies completed before energization with equipment labelled, qualified electrical workers wearing appropriate protective equipment, and permits for live work only where it cannot be avoided.
In Canada, electrical safety in the workplace follows CSA Z462 (workplace electrical safety, the Canadian counterpart of NFPA 70E) and provincial occupational health and safety regulations, with lockout under CSA Z460 and the provincial rules.
How many units to test
Large data centres contain hundreds of identical items: rack power distribution units, computer room air handlers, fan coil units, breakers and valves. Owners must decide whether to test every unit fully or a sample. Critical items whose failure could drop IT load are normally tested 100 %, while some functional tests of numerous identical items may be sampled, with the sample expanded if failures are found. Sampling has a statistical cost: small samples can easily miss defects.
from math import comb, ceil, log

def p_detect(N, D, n):
    """Probability that a random sample of n from N units includes at least one of D defective units."""
    return 1 - comb(N - D, n) / comb(N, n)

N = 120                      # identical rack power distribution units on a project
for D in (2, 6, 12):         # number of defective units actually present
    for n in (10, 24, 60, 120):
        print(f"D = {D:2d} defective, sample {n:3d}: P(find at least one) = {p_detect(N, D, n):.2f}")
    print()

# Sample size for 95 percent confidence of catching a defect rate p (large population)
for p in (0.01, 0.05, 0.10):
print(f"Defect rate {p:.0%}: sample at least {ceil(log(0.05) / log(1 - p))} units")D = 2 defective, sample 10: P(find at least one) = 0.16 D = 2 defective, sample 24: P(find at least one) = 0.36 D = 2 defective, sample 60: P(find at least one) = 0.75 D = 2 defective, sample 120: P(find at least one) = 1.00 D = 6 defective, sample 10: P(find at least one) = 0.41 D = 6 defective, sample 24: P(find at least one) = 0.75 D = 6 defective, sample 60: P(find at least one) = 0.99 D = 6 defective, sample 120: P(find at least one) = 1.00 D = 12 defective, sample 10: P(find at least one) = 0.67 D = 12 defective, sample 24: P(find at least one) = 0.94 D = 12 defective, sample 60: P(find at least one) = 1.00 D = 12 defective, sample 120: P(find at least one) = 1.00 Defect rate 1%: sample at least 299 units Defect rate 5%: sample at least 59 units Defect rate 10%: sample at least 29 units
The results are sobering. If 2 of 120 PDUs are defective, a 20 % sample (24 units) has only a 36 % chance of finding either of them. Even a 50 % sample finds one only 75 % of the time. Sampling works well when defects are systematic, such as a wrong firmware version or a design error affecting every unit, because then a few tests catch them; it works poorly for random installation defects such as a loose connection. That is why installation checks (Level 2) are usually done on every unit even when functional tests are sampled, and why thermal scanning under load, which checks every connection quickly, is a standard part of electrical commissioning (Lesson 3).
Documentation and turnover
The commissioning record must be complete enough that the operators, and auditors, can see exactly what was tested and how the facility should behave. It includes:
- Completed checklists and test scripts with recorded results, signatures and supporting data (power quality recordings, thermal images, trend logs).
- The issues log, with every item closed or formally accepted with a plan.
- As-built drawings and single-line diagrams that match the installed facility, and final protective device settings.
- Operation and maintenance manuals, warranty information and spare parts lists.
- Sequences of operation as finally implemented in the controls.
- Training records for the operations team.
- The commissioning report, summarizing the process, results, outstanding items and recommendations.
These are gathered into turnover packages, often by system, and handed to operations as part of acceptance. Incomplete documentation is one of the most common complaints of operators taking over new facilities; insist on it before accepting handover.
Common mistakes
MistakeSkipping factory witness tests to save travel.
InsteadWitness tests of long-lead critical equipment; factory fixes are cheaper.
MistakeStarting functional tests before installation checks are complete.
InsteadRespect the level gates and close critical issues first.
MistakeImprovising during a live test when something unexpected happens.
InsteadStop, record the issue and resume only with an understood plan.
MistakeRelying on small samples to find random installation defects.
InsteadInspect every unit and use thermal scanning; sample only where defects are systematic.
MistakeAccepting handover without complete documentation.
InsteadRequire test records, as-builts, settings, manuals and training first.
Summary and key terms
- Five levels: factory witness, delivery and installation, start-up, functional performance, integrated systems testing.
- Each level is a gate; critical issues must close before the next.
- Test scripts state purpose, prerequisites, safety, initial conditions, steps with expected results, acceptance criteria and sign-off.
- Commissioning is a high-risk period; follow an energization plan, lockout and arc-flash rules.
- Random defects are easily missed by sampling; inspect all units and sample only systematic risks.
- Turnover documentation includes test records, issues log, as-builts, settings, manuals and training.
- Complete documentation is a condition of acceptance.
- Factory witness test
- A test of equipment at the manufacturer, witnessed by the owner's team.
- Pre-functional checklist
- A list verifying that equipment is installed correctly before start-up.
- Start-up
- Bringing a piece of equipment into operation for the first time.
- Functional performance test
- A test proving a system performs its functions, including failures, at load.
- Integrated systems test
- A test of all systems together through realistic failure scenarios.
- Test script
- A step-by-step test procedure with expected results and acceptance criteria.
- Acceptance criteria
- Measurable limits a test result must meet.
- Energization plan
- A plan controlling when and how equipment becomes live.
- Turnover package
- The documentation handed to operations for a system.
- Sequence of operation
- The description of how a control system operates in each condition.
Practice problems
Work each problem on paper first, then reveal the answer to check.
At which level is a UPS first tested on a load bank with a module failed on site?
Show answer
Level 4, functional performance testing.
What is checked during Level 2?
Show answer
Delivery condition and correct installation: anchorage, clearances, terminations, torque, grounding, labelling.
Why are factory witness tests valuable?
Show answer
Problems are cheaper and quicker to fix at the factory than on site.
List five elements of a test script.
Show answer
For example: purpose, prerequisites, safety, initial conditions, steps with expected results, acceptance criteria, sign-off.
In the UPS example, what load does each remaining module carry after one fails?
Show answer
About 500 kW, 100 % of its rating.
What should happen if a test step produces an unexpected result?
Show answer
Stop, record it in the issues log, and resume only after the cause is understood.
Using the output, what sample of 120 PDUs gives a 99 % chance of catching one of 6 defective units?
Show answer
About 60 units.
How many units must be sampled to detect a 10 % defect rate with 95 % confidence?
Show answer
About 29.
Why does sampling work better for firmware errors than for loose connections?
Show answer
Firmware errors affect every unit; loose connections are random.
Name four items in a turnover package.
Show answer
For example: test records, issues log, as-built drawings, relay settings, O&M manuals, training records.
Lesson quiz · 5 questions
Score 60% or more to complete this lesson.
Create a free account to save your progress, take quizzes and earn a certificate.