
CON-410 · Lesson 2 of 12 · 26 min
Lean thinking: principles, value and waste
Lean thinking began on the factory floors of Toyota in the decades after the Second World War, where engineers such as Taiichi Ohno built a production system that made more cars with less labour, inventory and space than the mass-production plants of North America. BUS-230 lesson 11 describes the Toyota Production System in a manufacturing setting: just-in-time, kanban, set-up reduction, error-proofing and value stream mapping. This lesson does not repeat that material. It asks what the same ideas mean when the product is a building, the factory moves to the site and the workers belong to a dozen different companies.
From lean production to lean construction
The term lean production was popularized in 1990 by the book The Machine That Changed the World, based on MIT research comparing car plants. In 1992 the Finnish researcher Lauri Koskela published an influential report arguing that construction had been managed almost entirely as a series of conversions, in which inputs such as concrete and labour are turned into outputs such as walls, and that it had ignored the flows between conversions: moving, waiting, inspecting and reworking. He proposed a view of production as three things at once: transformation of inputs into outputs, flow of work and materials through time, and generation of value for the customer. Traditional project management, with its focus on activities and their costs, handles the first well and the other two badly. Lean construction was born from the attempt to manage all three.
| View of production | Main idea | Typical management tool | What it misses on its own |
|---|---|---|---|
| Transformation | Break the project into activities and execute each efficiently | Work breakdown structure, cost codes, CPM | Waiting, moving and rework between activities |
| Flow | Reduce waste and variability in the movement of work and materials | Pull planning, takt planning, Last Planner System | Whether the right product is being built |
| Value | Deliver what the customer actually needs | Target value design, requirements capture | How efficiently the work is done |
The five lean principles
James Womack and Daniel Jones summarized lean thinking in five principles in their 1996 book Lean Thinking. They translate well to construction, with some adjustment.
| Principle | In manufacturing | In construction |
|---|---|---|
| Specify value | Define what the customer will pay for | Understand the owner's and users' real needs, including operations and maintenance |
| Map the value stream | Identify every step from raw material to customer | Trace design, approvals, procurement, fabrication, delivery and installation for key systems |
| Make value flow | Eliminate stops and batches between steps | Sequence trades so each can work continuously through zones |
| Let the customer pull | Produce only what the next step needs, when it needs it | Release work, information and materials when the next trade is ready for them |
| Pursue perfection | Improve continuously | Learn from every missed commitment and every project |
The principles are deceptively simple. Specifying value sounds obvious, but many projects are built to a design that nobody checked against how the building will actually be used. Making value flow sounds easy, but construction schedules are full of batches: all the framing on all floors, then all the rough-in, then all the board. Pull sounds natural, but most sites push: materials arrive when the supplier can ship them, and trades start when their contracts say they should, whether or not the area is ready.
Value and waste
In lean terms, an activity adds value if it transforms the product in a way the customer cares about, is done right the first time and is something the customer would willingly pay for. Installing a window adds value. Carrying the window from the laydown area to the floor is necessary but adds no value: the customer would be just as happy if it appeared at the opening by magic. Re-installing the window because it was set at the wrong height adds negative value, since it consumes resources and delays the project.
| Category | Definition | Site example | Management aim |
|---|---|---|---|
| Value-adding | Changes the product in a way the customer wants, done right first time | Placing and finishing a slab | Make it efficient and safe |
| Necessary non-value-adding | Needed under current methods but adds no value | Moving material, setting up scaffold, inspections | Reduce it by better logistics and methods |
| Pure waste | Adds no value and is not needed | Waiting for another trade, searching for tools, rework | Eliminate it |
The middle category is important. Material handling, set-up, safety meetings and inspections cannot simply be eliminated. Lean asks whether they can be reduced: by delivering materials to the floor where they will be installed, by prefabricating so that fewer set-ups happen in the field, or by building quality in so that fewer inspections find defects. Safety work is never treated as waste to be cut; a lean site aims to make safe work the easy and normal way of working.
The eight wastes on a construction site
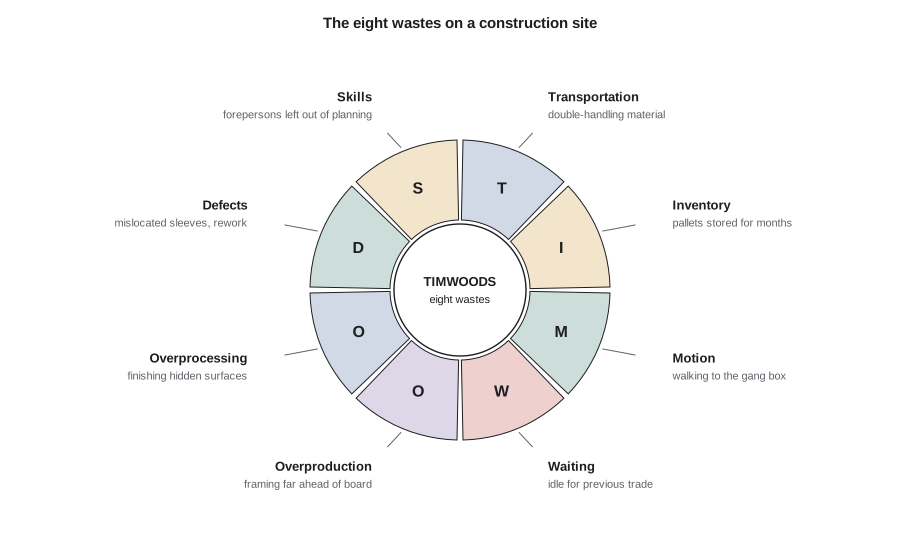
Toyota identified seven wastes, and an eighth, unused human potential, was added later. The acronym TIMWOODS is a common memory aid: transportation, inventory, motion, waiting, overproduction, overprocessing, defects and skills. Each has clear construction examples.
| Waste | Construction examples | Typical countermeasure |
|---|---|---|
| Transportation | Double-handling material between laydown, hoist and floor | Just-in-time delivery to the floor; kitting |
| Inventory | Months of stored material on floors, damaged or lost | Deliver to a short look-ahead; pull deliveries |
| Motion | Walking to the gang box, climbing ladders for tools | Mobile carts, point-of-use storage, good workface layout |
| Waiting | Crews idle because the previous trade or an inspection is late | Make-ready process; reliable commitments |
| Overproduction | Framing floors that drywall cannot reach for weeks | Balance trade flow; release work by takt |
| Overprocessing | Finishing surfaces that will be covered; excessive submittals | Clarify required quality; simplify approvals |
| Defects | Rework of mislocated sleeves, failed tests, deficiencies | First-run studies, checklists, built-in quality |
| Skills (unused potential) | Forepersons excluded from planning; ideas ignored | Involve the people doing the work in planning and improvement |
Overproduction deserves special attention because it looks like progress. A framing crew that races ahead of the board crew appears productive, but the extra framed area sits idle, gets damaged, blocks other trades and hides the fact that the downstream trade is the real constraint. In lean thinking, producing more than the next step can use is a waste even when every individual crew is busy. The goal is a steady, balanced flow, not maximum local output.
Worked problem
Counting waste in a material path
On Willowmere Residences, a pallet of drywall is unloaded by a boom truck to a laydown area (15 minutes of a crew of two), later moved by forklift to the hoist (10 minutes, one operator plus one helper), lifted (5 minutes of the hoist operator), and moved on the floor by hand to the work area (40 minutes for two people). Delivering directly to the floor with a crane-fed loading platform would take 20 minutes of a crew of three. How many worker-minutes does direct delivery save per pallet?
Show solution
- Current path: 15 × 2 + 10 × 2 + 5 × 1 + 40 × 2 = 30 + 20 + 5 + 80 = 135 worker-minutes.
- Direct delivery: 20 × 3 = 60 worker-minutes.
- Saving: 135 − 60 = 75 worker-minutes per pallet.
- At 140 pallets for the building, the saving is 140 × 75 = 10,500 worker-minutes, or 175 hours.
Answer: About 75 worker-minutes per pallet, or 175 hours for the job, before counting less damage and fewer lost boards. Figures are illustrative.
Value from the owner's point of view
Lean begins with value, and value is defined by the customer. On a construction project there are several customers: the owner who pays, the users who occupy the building, the operators who maintain it and the community around it. Their needs may conflict. A lean design process tries to understand them early, through user interviews, mock-ups and conditions of satisfaction, and to set a target cost and design to it, an approach called target value design that CON-340 introduced in the context of integrated project delivery. The construction team also has internal customers: each trade is the customer of the trade before it. A drywall finisher's customer is the painter, who needs a flat, clean, properly sanded surface ready on the day promised.
| Customer | What they value | Example of misalignment |
|---|---|---|
| Owner | Cost, schedule, return on investment | Upgrades chosen without operating cost analysis |
| Users | Function, comfort, accessibility | Suite layouts approved without user input |
| Operators | Maintainability, durable systems, access | Valves and dampers buried above inaccessible ceilings |
| Next trade | Area ready, clean, on the promised day | Mechanical trade leaves debris and incomplete hangers |
Respect for people
Toyota described its system as resting on two pillars: continuous improvement and respect for people. In construction, respect for people means more than politeness. It means asking the forepersons and tradespeople who do the work how it should be planned, because they know what their crews need. It means making safety a condition of work rather than a target to be traded off. It means stable relationships with trade partners rather than shopping every package to the lowest bidder. And it means that problems are treated as opportunities to improve the system, not as occasions to blame individuals. Lean tools used without respect for people, for example a percent-plan-complete chart used to punish trades, quickly turn into a new way of pushing harder and lose their value.
| Practice | Respectful version | Disrespectful version |
|---|---|---|
| Planning | Trade forepersons plan their own work and make commitments | Office issues a schedule and demands compliance |
| Metrics | Used to find and fix causes of failure | Used to rank and punish trades |
| Problems | Root causes in the system are investigated | The person nearest the problem is blamed |
| Ideas | Workers' suggestions are recorded and acted on | Suggestions are ignored |
Common misunderstandings of lean
Lean is often misunderstood. It is not a cost-cutting program, although it usually lowers cost. It is not about working faster, although work often gets done sooner. It is not a set of tools, although it uses many. It is not something that can be installed by a consultant in a week. And it is not only for large contractors: small firms often adopt lean planning more easily because their decision chains are short. The test of whether a site is lean is not whether it has sticky notes on the wall but whether work flows, promises are kept and the team gets better every week.
# Classifying observed activities into value-adding, necessary and waste
observations = [("hanging board", "VA"), ("cutting board", "VA"), ("carrying board", "NNVA"),
                ("waiting for hoist", "W"), ("taping joints", "VA"), ("searching for screws", "W"),
                ("setting up scaffold", "NNVA"), ("re-hanging damaged board", "W"),
                ("toolbox talk", "NNVA"), ("hanging board", "VA"), ("walking to gang box", "W"),
                ("hanging board", "VA")]
labels = {"VA": "value-adding", "NNVA": "necessary non-value-adding", "W": "waste"}
from collections import Counter
c = Counter(k for _, k in observations)
n = len(observations)
for k in ("VA", "NNVA", "W"):
print(f"{labels[k]:<28}{c[k]:>3} {c[k] / n:.0%}")value-adding 5 42% necessary non-value-adding 3 25% waste 4 33%
Even a small set of observations, sorted into the three categories, starts useful conversations: why are crews searching for screws, and why was board damaged? Lesson 10 shows how to run a proper work-sampling study with enough observations to draw conclusions.
Common mistakes
MistakeTreating every non-value-adding activity as waste to be eliminated.
InsteadDistinguish necessary non-value-adding work, which should be reduced, from pure waste, which should be eliminated.
MistakeCelebrating a crew that races far ahead of the next trade.
InsteadRecognize overproduction; aim for a balanced flow matched to the downstream trade.
MistakeDefining value only from the contractor's point of view.
InsteadStart with the owner, users, operators and the next trade as customers.
MistakeUsing lean metrics to blame and punish trades.
InsteadUse them to find and fix causes in the system, with respect for people.
MistakeEquating lean with cost cutting or working faster.
InsteadSee lean as managing value and flow; cost and time savings follow.
Summary and key terms
- Lean construction applies the ideas of the Toyota Production System to design and construction.
- Koskela argued that construction manages transformation well but neglects flow and value.
- The five lean principles are specify value, map the value stream, make value flow, let the customer pull and pursue perfection.
- Activities are value-adding, necessary but non-value-adding, or pure waste.
- The eight wastes (TIMWOODS) all have clear site examples; overproduction is especially deceptive.
- Value is defined by the owner, users, operators and the next trade as internal customer.
- Respect for people, including involving forepersons in planning, is a pillar of lean, not an add-on.
- Lean thinking
- A management approach focused on delivering value with minimal waste through flow and continuous improvement.
- Transformation view
- Seeing production as the conversion of inputs into outputs through activities.
- Flow view
- Seeing production as the movement of work and materials through time, including waiting and moving.
- Value-adding activity
- Work that changes the product in a way the customer wants, done right the first time.
- Necessary non-value-adding activity
- Work required under current methods that adds no value, such as material handling.
- Waste
- Any activity that consumes resources without adding value and is not necessary.
- TIMWOODS
- A memory aid for the eight wastes: transportation, inventory, motion, waiting, overproduction, overprocessing, defects and skills.
- Overproduction
- Producing more, or sooner, than the next step can use.
- Internal customer
- The next trade or team that receives a crew's work.
- Respect for people
- The lean pillar of involving and supporting the people who do the work.
Practice problems
Work each problem on paper first, then reveal the answer to check.
Name Koskela's three views of production.
Show answer
Transformation, flow and value.
Classify carrying conduit from the laydown area to the third floor.
Show answer
Necessary non-value-adding work: reduce it with better logistics.
Classify reinstalling a door frame set in the wrong location.
Show answer
Waste (a defect).
What does the S in TIMWOODS stand for?
Show answer
Skills, or unused human potential.
Why is a framing crew far ahead of drywall a problem?
Show answer
Overproduction: the extra work sits idle, gets damaged and hides the real constraint.
Who is the internal customer of the drywall taper?
Show answer
The painter, or whichever trade follows.
Give one countermeasure for the waste of inventory on floors.
Show answer
Deliver to a short look-ahead or pull deliveries to match installation.
A material path takes 4 people 30 minutes and an alternative takes 2 people 20 minutes. What is saved?
Show answer
120 − 40 = 80 worker-minutes per load.
What is target value design?
Show answer
Setting a target cost from the owner's value and designing to it.
Why can lean tools fail without respect for people?
Show answer
They become another way of pushing and blaming, so people stop reporting problems honestly.
Lesson quiz · 5 questions
Score 60% or more to complete this lesson.
Create a free account to save your progress, take quizzes and earn a certificate.