
CIV-331 · Lesson 10 of 12 · 21 min
Welded connections
Welding joins steel by melting the parts and a filler metal together so that they solidify as one piece. It makes compact, stiff connections with no holes, it can join members at any angle, and it is the natural way to attach stiffeners, base plates and connection plates in the shop. Field welding is slower and needs good conditions and inspection, so the usual practice in North America is to weld in the shop and bolt in the field. This lesson introduces welding processes and weld types, then designs fillet welds for the truss chord and for the monorail bracket.
Welding processes
All arc welding processes strike an electric arc between an electrode and the work, melting both, and shield the molten pool from the air, which would make the weld porous and brittle.
- Shielded metal arc welding (SMAW), or stick welding, uses a coated electrode whose coating produces the shielding gas and slag. It is simple and portable, and common for field work and repairs.
- Flux-cored arc welding (FCAW) feeds a tubular wire filled with flux continuously, with or without an external shielding gas. It is fast and is the most common process in structural fabrication shops and for field welding.
- Gas metal arc welding (GMAW) feeds a solid wire with a gas shield. It is clean and fast but sensitive to wind.
- Submerged arc welding (SAW) buries the arc under a granular flux and is used for long, heavy shop welds such as the flange-to-web welds of plate girders.
In Canada, welding of structural steel follows CSA W59, and companies that fabricate or erect welded steel must be certified by the Canadian Welding Bureau under CSA W47.1, with qualified welding procedures and welders. The filler metal is matched to the steel; E49XX electrodes, with a tensile strength \(X_u = 490\) MPa, match 350W and 345WM steel.
Types of welds
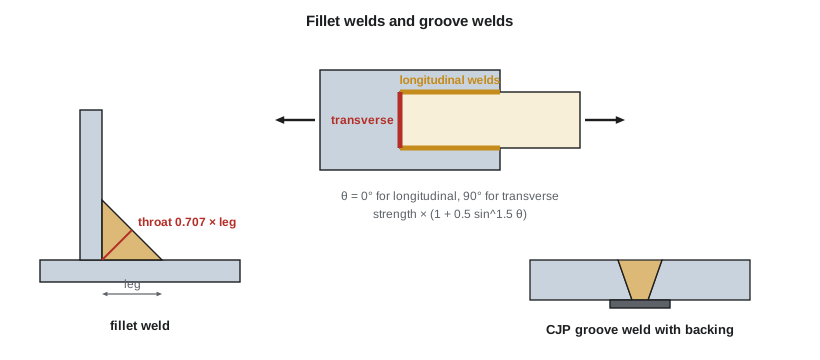
Fillet welds have a roughly triangular cross-section and join surfaces at an angle, usually 90 degrees, in lap, tee and corner joints. They need no edge preparation, so they are the cheapest and most common welds, perhaps 80 per cent of all structural welding. A fillet weld is specified by its leg size, and its strength comes from the throat, the shortest distance from the root to the face, which is 0.707 times the leg for an equal-leg weld.
Groove welds fill a gap or a bevelled groove between the parts. A complete-joint-penetration (CJP) groove weld fuses the full thickness and, with matching filler metal, is as strong as the base metal, so no calculation of weld strength is needed. Partial-joint-penetration (PJP) welds fuse only part of the thickness and are designed for their effective throat. Groove welds need edge preparation and often backing bars and ultrasonic testing, so they cost much more than fillet welds. Plug and slot welds fill holes in one part to join it to another and are used mainly to stitch plates together.
Welds are shown on drawings with standard welding symbols: an arrow to the joint, a reference line, a symbol for the weld type below the line for the arrow side or above it for the other side, and the size, length and pitch.
Strength of fillet welds
Tests show that fillet welds loaded transversely, with the load perpendicular to the weld axis, are about 50 per cent stronger than welds loaded longitudinally, along their axis, though less ductile. Both standards include this directional effect.
S16 gives the factored shear resistance of a fillet weld, per unit length, as the smaller of the weld metal and the base metal at the fusion face:
where \(A_w = 0.707D\) per millimetre of length for a weld of leg \(D\), \(A_m\) is the area of the fusion face, \(\theta\) is the angle between the load and the weld axis, and \(M_w\) reduces the strength when welds of different orientation share a load, because the stiffer transverse welds fracture before the longitudinal welds reach their strength. For a 6 mm fillet with E49XX electrodes loaded longitudinally, \(V_r = 0.67(0.67)(0.707 \times 6)(490) = 933\) N/mm, or about 0.155 kN/mm per millimetre of leg.
Size and length limits
A weld that is too small for thick parts cools too quickly and may crack, so CSA W59 sets minimum fillet sizes based on the thicker part joined: 5 mm for parts up to 12 mm, 6 mm up to 20 mm and 8 mm beyond. Along the edge of a plate, the maximum leg is the plate thickness less 2 mm for plates 6 mm or thicker, so the edge is not melted away. The effective length of a fillet weld should be at least four times its size, and end returns around corners help resist prying and fatigue.
The largest single-pass fillet weld is about 8 mm (5/16 in.). Larger welds need several passes and cost much more, so two small welds on both sides of a plate usually beat one large weld.
Welding the truss chord
In lesson 3 net fracture or block shear at the bolt holes governed the bottom chord. Owen asks the fabricator whether the chord angles could be shop-welded to the gussets, with the truss shipped in two halves and spliced with bolts at midspan. Welding removes the holes from most of the chord, so gross yielding would govern at the welded ends.
The weld along the heel of an angle and the weld along the toe are at different distances from the centroid of the angle. If the two welds have equal length, the connection is eccentric and the heel weld is overloaded. A balanced connection sizes each weld so that the resultant of the weld forces passes through the centroid of the angle: the heel weld takes the fraction \((b - \bar x)/b\) of the force and the toe weld takes \(\bar x/b\).
Worked problem
Balanced fillet welds for the chord angles
Each L102x102x9.5 of the bottom chord carries half of 705 kN. Design 6 mm E49XX fillet welds along the heel and toe of each angle, balanced about its centroid (\(\bar x = 29.0\) mm).
Show solution
- Weld metal, longitudinal: 0.933 kN/mm. Base metal on the 6 mm fusion face of the angle: \(0.67(0.67)(6)(450) = 1.21\) kN/mm. The weld metal governs.
- \[L = \frac{352.5}{0.933} = 378\ \text{mm per angle}\]
- \[L_{heel} = 378\,\frac{102 - 29}{102} = 270\ \text{mm} \qquad L_{toe} = 378\,\frac{29}{102} = 107\ \text{mm}\]
Answer: Use 6 mm fillets 275 mm long at the heel and 115 mm at the toe of each angle. With no holes, the chord resistance rises to the gross yielding value of 1166 kN, less a modest shear lag reduction for the welded end, which the standard relates to the weld length.
For single angles and tees in light trusses, many fabricators simply use equal welds and accept the small eccentricity; the standards allow this for statically loaded members. Balancing matters more for members under fatigue loading.
Eccentrically loaded weld groups
Weld groups loaded eccentrically are analysed like bolt groups. In the elastic method, the welds are treated as lines of unit width. The direct shear is spread uniformly over the total length, and the moment produces a force per unit length proportional to the distance from the centroid of the group, using the polar moment of inertia of the lines:
The instantaneous centre method, using measured load-deformation curves for welds at different angles, gives higher capacities, and handbook tables list coefficients for common weld shapes such as C-shapes and L-shapes.
Worked problem
Welded monorail bracket
An alternative monorail bracket is a plate welded to the column flange with two vertical fillet welds, each 250 mm long and 150 mm apart. The load is 60 kN at 300 mm from the centroid of the welds. Find the required weld size by the elastic method.
Show solution
- \[I_p = 2\Big[\frac{250^3}{12} + 250(75)^2\Big] = 2(1.302 + 1.406) \times 10^6 = 5.42 \times 10^6\ \text{mm}^3\]
- At the top of the weld nearest the load, \(x = 75\) mm and \(y = 125\) mm:
- \[f_x = \frac{60(300)(125)}{5.42 \times 10^6} = 0.415 \qquad f_y = \frac{60}{500} + \frac{60(300)(75)}{5.42 \times 10^6} = 0.120 + 0.249 = 0.369\ \text{kN/mm}\]
- \[f = \sqrt{0.415^2 + 0.369^2} = 0.556\ \text{kN/mm} \qquad D_{req} = \frac{0.556}{0.155} = 3.6\ \text{mm}\]
Answer: Strength needs only a 3.6 mm weld, so the minimum size for the 11 mm column flange, 5 mm, governs. The welded bracket is lighter-looking than the bolted one, but it requires field welding or a shop-welded column, which Priya rejects because the columns are already ordered.
The program reproduces both weld designs and confirms the directional increase for a transverse weld.
import math
# Fillet welds, CSA S16 clause 13.13: E49XX electrodes (Xu = 490 MPa), phiw = 0.67
phiw, Xu = 0.67, 490.0

def weld_per_mm(D, theta_deg=0.0):
    th = math.radians(theta_deg)
    Aw = 0.707 * D
    return 0.67 * phiw * Aw * Xu * (1.00 + 0.50 * math.sin(th)**1.5) / 1e3   # kN/mm

def base_per_mm(D, Fu):
    return 0.67 * phiw * D * Fu / 1e3

D = 6.0
qw, qb = weld_per_mm(D), base_per_mm(D, 450.0)
print(f"6 mm fillet, longitudinal: weld metal {qw:.3f} kN/mm, base metal {qb:.3f} kN/mm")
print(f"Transverse weld is {weld_per_mm(D, 90)/qw:.2f} times as strong")

# Truss chord: each L102x102x9.5 carries half of 705 kN, welded to the gusset along heel and toe
T = 705.0 / 2
x_bar, b = 29.0, 102.0
L_total = T / min(qw, qb)
L_heel = L_total * (b - x_bar) / b
L_toe = L_total * x_bar / b
print(f"Weld length per angle = {L_total:.0f} mm: heel {L_heel:.0f} mm, toe {L_toe:.0f} mm (balanced)")

# Eccentric weld group: bracket plate welded to a column flange with two vertical welds
P, e = 60.0, 300.0                  # kN, mm from the centroid of the welds
Lw, xg = 250.0, 75.0                # each weld 250 mm long, at x = +/- 75 mm
A = 2 * Lw
Ip = 2 * (Lw**3 / 12 + Lw * xg**2)
M = P * e
fy = P / A + M * xg / Ip            # at the top or bottom of the weld nearest the load
fx = M * (Lw / 2) / Ip
f = math.hypot(fx, fy)
print(f"Elastic method: Ip = {Ip/1e6:.2f} x 10^6 mm3, largest force = {f:.3f} kN/mm")
D_req = f / (qw / D)
print(f"Required fillet size = {D_req:.1f} mm -> use 5 mm, the minimum for the 11 mm column flange")6 mm fillet, longitudinal: weld metal 0.933 kN/mm, base metal 1.212 kN/mm Transverse weld is 1.50 times as strong Weld length per angle = 378 mm: heel 270 mm, toe 107 mm (balanced) Elastic method: Ip = 5.42 x 10^6 mm3, largest force = 0.556 kN/mm Required fillet size = 3.6 mm -> use 5 mm, the minimum for the 11 mm column flange
Quality, inspection and cost
Weld quality depends on the procedure, the welder and the conditions. Common defects include porosity, slag inclusions, lack of fusion, undercut at the toes, and cracks, especially hydrogen-induced cracking in thick or high-carbon steel welded without preheat. Visual inspection by a qualified inspector checks every weld; magnetic particle testing finds surface cracks; ultrasonic testing checks the interior of groove welds. CJP welds in tension in moment connections are usually tested ultrasonically.
Welding also distorts. Weld metal shrinks as it cools, pulling the parts toward the weld and leaving residual stresses. Good detailing balances welds on both sides of a member, limits weld size and sequence, and avoids heavy welds in the field. When choosing between bolting and welding, consider the whole cost: shop welding of small attachments is cheap, field welding is expensive, and a detail that lets the field crew bolt is usually preferred.
Common mistakes
MistakeSpecifying a fillet weld by its throat.
InsteadFillet welds are specified by leg size; the throat is 0.707 times the leg.
MistakeMaking welds larger than needed for safety.
InsteadOversized welds add heat, distortion and cost; use the minimum that satisfies strength and the size limits.
MistakeAdding the full directional increase to every weld in a mixed group.
InsteadWhen longitudinal and transverse welds share load, their strengths cannot simply be added at full value.
MistakeIgnoring the base metal check for thin connected parts.
InsteadThe base metal along the weld can govern when the connected plate is thin.
Summary and key terms
- Most structural welds are fillet welds made by SMAW or FCAW; CJP groove welds develop the full base metal strength.
- Fillet weld: \(V_r = 0.67\phi_wA_wX_u(1.00 + 0.50\sin^{1.5}\theta)M_w\), with \(\phi_w = 0.67\); about 0.155 kN/mm per mm of leg for E49XX loaded longitudinally.
- Transverse welds are 50 per cent stronger than longitudinal welds but less ductile.
- Minimum fillet sizes depend on plate thickness; maximum sizes along edges keep the edge intact.
- Balanced welds put the resultant of the weld forces through the centroid of an angle; eccentric weld groups are analysed by the elastic or IC method.
- Fillet weld
- A weld of roughly triangular cross-section joining two surfaces at an angle.
- Leg size
- The length of the side of the largest triangle inscribed in a fillet weld.
- Throat
- The shortest distance from the root of a weld to its face, 0.707 times the leg for an equal-leg fillet.
- Complete-joint-penetration weld
- A groove weld that fuses the full thickness of the joined parts.
- Fusion face
- The surface of the base metal that is melted during welding.
- Directional strength increase
- The higher strength of fillet welds loaded at an angle to their axis.
- Balanced connection
- A welded connection in which the resultant weld force passes through the member centroid.
- Preheat
- Heating the base metal before welding to slow cooling and avoid cracking.
Practice problems
Work each problem on paper first, then reveal the answer to check.
What is the factored resistance of an 8 mm E49XX fillet weld 200 mm long loaded longitudinally?
Show answer
\(0.155(8)(200) = 248\) kN.
Why are transverse fillet welds stronger than longitudinal ones?
Show answer
The load acts across a larger failure plane and the stress state is more favourable, but the weld deforms less before fracture.
What is the minimum fillet weld size for joining a 16 mm plate to a 10 mm plate?
Show answer
6 mm, based on the thicker part (over 12 and up to 20 mm).
Why are fillet welds preferred to groove welds when either would work?
Show answer
They need no edge preparation or backing and are easier to inspect, so they cost much less.
Lesson quiz · 5 questions
Score 60% or more to complete this lesson.
Create a free account to save your progress, take quizzes and earn a certificate.