
BLR-210 · Lesson 11 of 12 · 19 min
Weld quality, NDE and repair
Three weeks after Riverbend, Ironbridge sends Marcel, Kiera and four other welders to the Pinecrest Paper mill, where the recovery boiler is down for its annual outage. A recovery boiler burns the spent cooking liquor from the pulp process and recovers its chemicals as a molten smelt that pours from the furnace floor. If water reaches that smelt, from a leaking tube, the result can be a violent explosion, so recovery boiler owners treat every pressure weld in the lower furnace with particular care, and every floor tube weld on this job is radiographed. Six floor tube butt welds, made on the night shift by another crew, have come back from Annika Sorensen's darkroom with their films. This lesson is about how welds are examined, how results are judged, and how rejected welds are repaired.
What can go wrong in a weld
Weld discontinuities are named by what they are and where they lie. Some are on the surface and can be seen; others are inside and can only be found by examination that looks through the metal.
| Discontinuity | What it is | Usual cause |
|---|---|---|
| Crack | A fracture in the weld or heat-affected zone | Hydrogen, restraint, hard microstructure, wrong filler |
| Incomplete fusion | Weld metal not fused to the groove face or to a previous pass | Low heat, wrong angle, fast travel, cold lap |
| Incomplete penetration | The root not fused through the full joint | Small root opening, high-low, low current, large land |
| Slag inclusion | Non-metallic slag trapped in the weld | Poor cleaning between passes, undercut edges |
| Porosity | Gas pores in the weld | Moisture, contamination, wind, long arc |
| Undercut | A groove melted into the base metal at the toe | High current, wrong angle, fast travel |
| Root concavity or suck-back | A root that is concave on the inside | Too much heat or too little filler at the root |
| Excess penetration | Too much root bead inside the tube | Too large a gap, too much heat |
| Arc strike | A spot melted by an arc outside the weld | Careless striking or a bad lead |
Cracks, incomplete fusion and incomplete penetration are planar: they are thin and flat, like a sheet of paper inside the metal, and they concentrate stress at their edges. They are the most dangerous, and pressure codes usually reject them at any size. Slag and porosity are volumetric: they have size in all directions, they are less severe, and codes accept them up to limits.
The examination methods
Non-destructive examination, NDE, finds discontinuities without damaging the part. Each method finds some kinds well and others poorly, and the examination plan in the repair package names which methods apply to which welds.
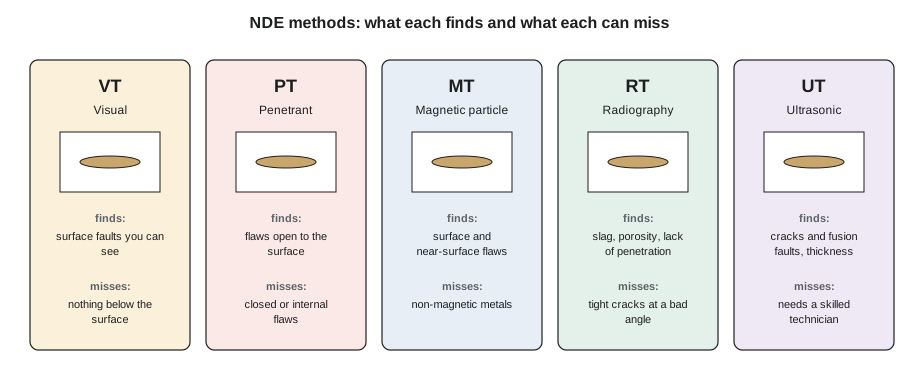
- Visual examination (VT). The first and cheapest method, done on every weld by the welder, the fitter and the inspector. It finds surface cracks, undercut, porosity, profile and dimension faults, arc strikes and spatter. A small light, a mirror, a magnifier and weld gauges are its tools.
- Liquid penetrant (PT). A colored or fluorescent liquid is applied to a clean surface, drawn into open surface flaws, wiped off, and drawn back out by a developer, showing the flaw as a line or dot. It works on any non-porous metal, including stainless, but finds only flaws open to the surface.
- Magnetic particle (MT). The part is magnetized and iron particles are applied; a surface or near-surface flaw disturbs the magnetic field and collects the particles. It works only on magnetic steels, finds flaws a little below the surface as well as at it, and is the usual check on back-gouges, ground areas and fillet welds on carbon steel.
- Radiography (RT). X-rays or gamma rays from a radioactive source pass through the weld onto film or a digital detector. Thicker or denser material shows lighter; voids, slag and lack of penetration show darker. It is the traditional method for tube butt welds and gives a permanent record.
- Ultrasonic testing (UT). High-frequency sound is sent into the metal by a probe, and reflections from flaws are displayed. Phased array UT uses many elements to sweep the beam and make an image. It finds planar flaws well, measures thickness, and needs no radiation exclusion zone, so it is increasingly used in place of RT.
Radiography on a job site
Field radiography of boiler tubes usually uses a gamma-ray source, a small sealed capsule of iridium-192 or selenium-75 in a shielded camera, wound out through a guide tube to the weld. The radiation is dangerous, and radiography is licensed work. In Canada, the Canadian Nuclear Safety Commission licenses the company and certifies the exposure device operators; in the US, the Nuclear Regulatory Commission or an agreement state does. The radiographers set up a controlled area with barriers, signs and radiation survey meters, and nobody else may be inside it during an exposure. On an outage, that usually means radiography is done at night or at shift change, when the boiler is cleared, which is why the night-shift welds come back with their films in the morning. Kiera's part is to leave the joints ready, cleaned, marked with their identification and location markers, and clear of tools, and to stay out of the barriers.
The film or image shows the weld with its identification, a location marker so a flaw can be found on the tube, and an image quality indicator, a set of wires or a small plate with holes, that proves the film shows fine enough detail. Annika reads each film under a viewer, records what she sees, and judges it against the acceptance standard in the examination plan.
Reading the results
The acceptance standard for the recovery boiler floor tubes is set by the code and the owner's specification. Illustrative rules of the kind used for tube butt welds are that any crack, incomplete fusion or incomplete penetration rejects the weld; that a slag line is accepted only up to a set length related to the wall thickness; and that porosity is accepted only up to a set size and number in a given length of weld. Kiera runs the six night-shift films through a review script using rules like these.
# Radiograph review and repair log for the recovery boiler floor tube welds (US units) - illustrative rules
t = 0.25                                   # tube wall
slag_max = 0.25                          # longest slag line allowed for this wall
never = {"crack", "incomplete fusion", "incomplete penetration"}
films = {
    "W1": [],
    "W2": [("porosity", 0.04, 2)],
    "W3": [("slag", 0.16, 1)],
    "W4": [("incomplete penetration", 0.4, 1)],
    "W5": [("slag", 0.35, 1)],
    "W6": [("porosity", 0.06, 9)],
}
repairs = []
for weld, inds in films.items():
    verdict = "accept"
    for kind, size, count in inds:
        if kind in never:
            verdict = f"reject: {kind}"
        elif kind == "slag" and size > slag_max:
            verdict = f"reject: slag {size} in over {slag_max}"
        elif kind == "porosity" and count > 6:
            verdict = f"reject: {count} pores in the film length"
    print(f"{weld}: {verdict}")
    if verdict != "accept":
        repairs.append((weld, verdict.split(": ")[1]))

print()
for n, (weld, why) in enumerate(repairs, 1):
print(f"repair {weld}-R{n}: excavate, PT the cavity, reweld to the WPS, re-radiograph ({why})")W1: accept W2: accept W3: accept W4: reject: incomplete penetration W5: reject: slag 0.35 in over 0.25 W6: reject: 9 pores in the film length repair W4-R1: excavate, PT the cavity, reweld to the WPS, re-radiograph (incomplete penetration) repair W5-R2: excavate, PT the cavity, reweld to the WPS, re-radiograph (slag 0.35 in over 0.25) repair W6-R3: excavate, PT the cavity, reweld to the WPS, re-radiograph (9 pores in the film length)
Three welds are accepted. W4 has incomplete penetration at the root, which no length of acceptance allows; W5 has a slag line 0.35 in long, longer than the 1/4 in limit for this wall; and W6 has more pores in the film length than the limit. All three must be repaired, and each repair gets a number so it can be followed on the traveler.
Making a weld repair
A weld repair is a small welding job of its own, done to a procedure, and it is examined again. The sequence is the same on every repair:
- Locate the flaw on the weld from the film's location markers, or by UT, and mark it.
- Excavate the flaw by grinding, with small burrs and discs on tube walls, until it is removed, checking as the cavity deepens. Gouging, as lesson 4 explained, is too aggressive for thin tube walls.
- Examine the cavity by PT or MT to confirm the flaw is gone, and measure the remaining wall.
- Shape the cavity so it can be welded: smooth, with sloped ends and no sharp corners.
- Reweld to the WPS, with the preheat and any PWHT it requires; a repair in an alloy weld usually means repeating the heat treatment.
- Re-examine the repair by the same method that rejected it, and by VT.
For W4, incomplete penetration at the root, the excavation has to go through the full wall, because the defect is at the root; Marcel grinds the root out over the length of the indication plus a little each end, and rewelds it with a new GTAW root and fill. For W5 and W6, the slag and porosity are in the fill, and the excavation stops when the cavity is clean. All three are re-radiographed the next night.
Owners usually limit how many times the same spot may be repaired, often to one or two, because each repair puts more heat into the same metal. If a repair fails, the weld may have to be cut out and the tube replaced with a new dutchman. Riverbend's specification allows two repairs on the same area of a tube weld; the mill's allows one.
Finding the cause
Three rejections out of six welds is too many, and Marcel wants to know why before his crew welds the next set. He looks at the films with Annika and talks to the night-shift welder. The incomplete penetration on W4 sits at the place where the root meets the tube on the side next to the floor's support, where the welder could not see the root and the gap was tight. The slag on W5 is at the edge of a fill pass, where a humped bead left a valley that was not ground. And the porosity on W6 lines up with a time when the floor's lower header access door was open and a draft came up through the furnace. The fixes are a mirror and a better fit-up check on the hidden side, grinding humped beads before the next pass, and a tarp across the access door.
This is the point of examination. A radiograph tells the crew not only which welds to fix, but what it is doing wrong.
Worked problem
Is the slag line acceptable?
A floor tube weld in a 1/4 in wall shows a slag line 5/32 in long. The rule in use rejects slag longer than 1/4 in for this wall. Is the weld accepted?
Show solution
- The slag line is 5/32 in, less than the 1/4 in limit.
- Slag is volumetric and is accepted within its limit; there are no planar indications on the film.
Answer: Yes, the weld is accepted for this indication, and the result is recorded on the traveler.
The welder's own inspection
Every examination method in this lesson comes after the welder has looked at the weld. A welder who checks each pass for undercut, slag at the toes and craters, grinds what needs grinding and checks the cap with gauges before calling for inspection catches most surface faults before anyone else sees them. Marcel's crew checks each completed tube weld with a light and mirror round the back, a fillet or cap gauge for reinforcement, and a straightedge along the tube for alignment, and writes the welder's own visual acceptance on the traveler before radiography. A weld that comes back from radiography rejected is a lesson for the welder; a weld that is rejected visually by the inspector, for a fault the welder could have seen, is a habit to break.
Common mistakes
MistakeTreating a small crack like a small slag line.
InsteadPlanar flaws, cracks, incomplete fusion and incomplete penetration, are rejected at any size.
MistakeGouging out a root defect in a thin tube wall.
InsteadGrind with burrs and discs and check as you go.
MistakeRewelding without confirming the flaw is gone.
InsteadExamine the cavity by PT or MT before rewelding.
MistakeWalking into a radiography area to fetch a tool.
InsteadStay outside the barriers until the radiographers clear the area.
MistakeFixing the rejected welds without asking why they failed.
InsteadFind the cause and change the practice before the next welds.
Summary and key terms
- Planar flaws, cracks, incomplete fusion and incomplete penetration, are the most dangerous and usually rejected at any size.
- VT, PT and MT find surface flaws; RT and UT find internal ones.
- Field radiography is licensed work behind barriers; leave the joints ready and stay clear.
- Acceptance standards come from the code and the owner's specification and are applied to every film.
- Repairs are excavated, confirmed clean, shaped, rewelded to the WPS and re-examined, within a repair limit.
- Every rejection should lead to a cause and a change in practice.
- NDE
- Non-destructive examination: finding flaws without damaging the part.
- Planar flaw
- A thin, flat discontinuity such as a crack or lack of fusion.
- Volumetric flaw
- A discontinuity with size in all directions, such as porosity or slag.
- Image quality indicator
- A device on a radiograph that shows the image can reveal fine enough detail.
- Phased array UT
- Ultrasonic testing with a multi-element probe that sweeps the beam and builds an image.
- Repair limit
- The number of times the same area of a weld may be repaired before it must be cut out.
Practice problems
Work each problem on paper first, then reveal the answer to check.
Which method would you use to check a back-gouge on carbon steel plate?
Show answer
Magnetic particle examination, after visual inspection.
A weld in 1/4 in wall shows incomplete fusion 1/8 in long. Is it accepted under the rules in this lesson?
Show answer
No; incomplete fusion is rejected at any size.
Why are recovery boiler floor tube welds examined so carefully?
Show answer
Water from a leak meeting the molten smelt can cause an explosion.
Name two flaws penetrant testing cannot find.
Show answer
Internal slag and internal porosity, or any flaw not open to the surface.
Lesson quiz · 5 questions
Score 60% or more to complete this lesson.
Create a free account to save your progress, take quizzes and earn a certificate.