
WLD-120 · Lesson 11 of 12 · 18 min
Fillet welds in the horizontal position
Most fillet welds in a fabrication shop are not made in the flat position. A stiffener on a girder web, a clip angle on a column, a bracket on a skid, a gusset on a frame too big to roll: in each the bottom plate lies flat and the other plate stands up from it, and the fillet runs along the corner, made from the side. This is the horizontal fillet, 2F, and it is the position in which a welder makes more fillets than any other. It is also harder than it looks. Gravity pulls the puddle down onto the bottom plate, so the top edge tends to undercut and the bottom edge tends to roll over without fusing, and the two legs come out unequal unless the welder corrects for it. This lesson covers horizontal fillet technique, single-pass and multi-pass horizontal fillets, the faults peculiar to the position and how to control them, and the stiffener welding on the Riverside girders, where Devon makes horizontal fillets on company work for the first time.
The horizontal fillet
In a 2F fillet, the weld axis is horizontal, one plate is horizontal and the other vertical, and the welder works from the side, with the electrode coming in roughly along the bisector of the corner. The puddle wants to sag. Molten metal and slag flow down and out onto the horizontal plate, so the bottom leg tends to grow and the vertical leg to shrink, the face tends to bulge toward the bottom, the bottom toe can overlap, and the top toe, where the arc melts into the vertical plate and the metal then drains away, tends to be left as a groove of undercut. Every element of horizontal technique is aimed at counteracting that sag.
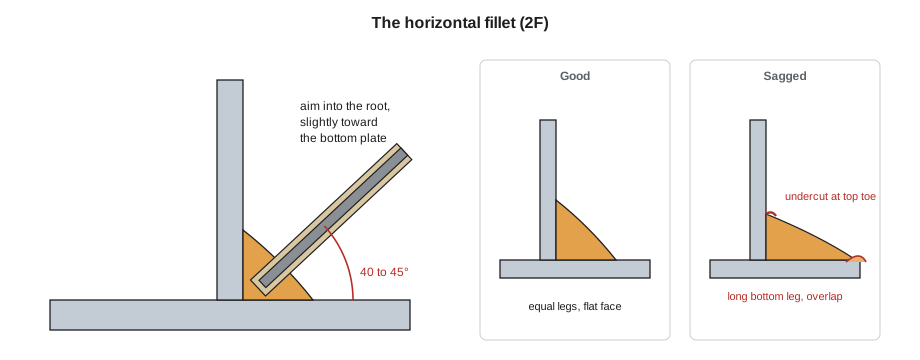
Technique for a single-pass horizontal fillet
- Work angle: about 40 to 45 degrees from the bottom plate, a few degrees lower than the 45 degrees of a flat fillet, so the arc favours the bottom plate slightly. The bottom plate is a bigger heat sink because the puddle sits on it, and pointing the arc slightly toward it also helps the upper leg by keeping the arc force off the vertical plate's toe.
- Aim point: into the root, or very slightly onto the bottom plate just ahead of the root, so the arc fuses the root and the puddle builds up on both plates.
- Travel angle: a drag of about 10 to 20 degrees, as in the flat position.
- Arc length: short. A long arc spreads heat onto the vertical plate and digs undercut there; with E7018 the covering cup almost touches.
- Current: a little lower than for the same fillet in the flat position, because the puddle must be kept small enough to stay up. For E7018 3.2 mm (1/8 in), about 110 to 135 A; for 4.0 mm (5/32 in), about 140 to 170 A.
- Travel speed: steady, fast enough that the puddle does not grow beyond the intended size and sag.
- Manipulation: a straight stringer is best for single passes. A very small motion that takes the arc up to the top toe and back down, pausing a moment at the top, can help fill the top edge, but wide weaving in the horizontal position nearly always makes the sag worse.
Watch the top toe. If a dark line or a groove appears along the vertical plate behind the puddle, the arc is too long, the current too high, the electrode aimed too high, or the travel too slow, letting metal drain away. If the bottom edge of the puddle rolls out over the plate in a shiny lip without wetting in, the current is too low, the travel too slow, or the electrode aimed too low.
The largest horizontal fillet one pass can hold is smaller than in the flat position. With SMAW, single-pass horizontal fillets are generally kept to about 8 mm (5/16 in) leg; above that, the puddle sags and the legs come out unequal. Larger horizontal fillets are made in multiple passes.
Multi-pass horizontal fillets
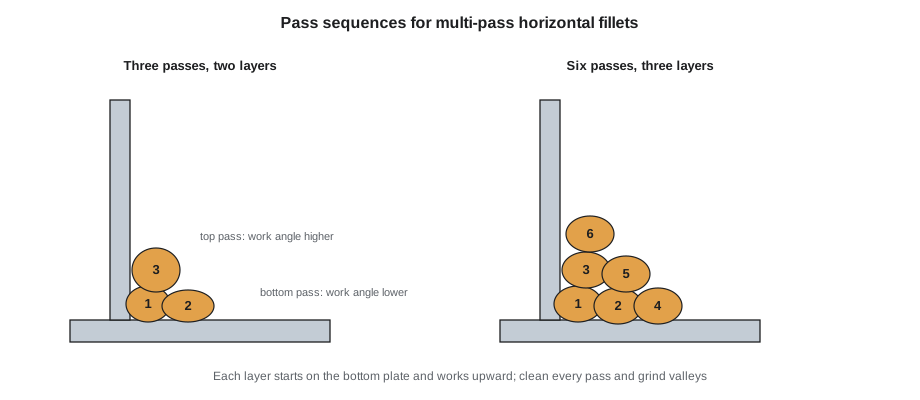
Multi-pass horizontal fillets are built from stringers, each placed so that it supports the next and the finished face is flat with equal legs. The usual sequence works upward from the bottom plate:
- Pass 1, the root: a stringer into the root, aimed as for a single pass.
- Pass 2: on the bottom plate, against the lower edge of pass 1, overlapping it by about half. The work angle drops, to roughly 30 degrees or lower, so the arc favours the bottom plate.
- Pass 3: above pass 2, against the vertical plate and overlapping the top of pass 2 and pass 1 by about half. The work angle rises, to about 50 to 60 degrees, so the arc favours the vertical plate and fills the top toe without undercut.
- Further layers: each layer starts on the bottom plate and works up, one pass more than the layer below, until the legs reach size.
Each pass sits on a shelf made by the one below it, which is why the sequence goes from the bottom up. Slag is removed after every pass, and any valley between passes is ground before it is welded over, because the horizontal position traps slag in the upper corner of each valley. The legs are checked with a fillet gauge after each layer, adjusting the next layer's passes to keep them equal.
# Plan the passes for a multi-pass horizontal fillet
import math
leg = 12                # specified fillet leg (mm)
max_single = 8          # largest leg one horizontal pass can hold (mm)
area = leg ** 2 / 2 * 1.10                 # cross-section with a little convexity (mm2)
area_pass = max_single ** 2 / 2            # metal one pass can lay (mm2)
passes = math.ceil(area / area_pass)
layers, total = 0, 0
while total < passes:                      # layer k holds k passes: 1, 3, 6, 10 ...
    layers += 1
    total += layers
print(f"fillet {leg} mm: {area:.1f} mm2, about {area / area_pass:.1f} single-pass volumes")
print(f"plan {total} passes in {layers} layers")
n = 0
for k in range(1, layers + 1):
    seq = []
    for j in range(k):
        n += 1
        where = "root" if k == 1 else ("bottom plate" if j == 0 else ("top toe" if j == k - 1 else "middle"))
        seq.append(f"{n}:{where}")
print(f" layer {k}: " + ", ".join(seq))fillet 12 mm: 79.2 mm2, about 2.5 single-pass volumes plan 3 passes in 2 layers layer 1: 1:root layer 2: 2:bottom plate, 3:top toe
The program rounds up to full layers, because a fillet with a partial last layer has unequal legs. For a 12 mm (1/2 in) horizontal fillet that comes to three passes in two layers, the classic root, bottom and top sequence; a 16 mm (5/8 in) fillet goes to six passes in three layers. Hartwell's procedures for the larger skid fillets show the same pattern in their sketches.
Faults peculiar to the horizontal position
| Fault | Cause in 2F | Fix |
|---|---|---|
| Undercut at the top toe | Arc long or aimed high; current high; travel slow, letting metal drain | Shorter arc; aim slightly lower; reduce current; brief pause at the top |
| Overlap at the bottom toe | Current low; aimed too low; travel slow; puddle too big | Raise current a little; aim into the root; travel faster |
| Unequal legs, bottom long | Puddle sagging; work angle too low on a single pass | Smaller puddle; correct work angle; use multiple passes |
| Convex, sagging face | Too much metal per pass; current low | Smaller passes; correct current; faster travel |
| Slag at the top of a valley | Valleys between passes not cleaned; pass placed too low | Grind valleys; place passes to overlap by half |
| Lack of root fusion | Arc aimed at the face, not the root; travel fast | Aim into the root; slower root pass |
Worked problem
Reading a test fillet
Devon's first horizontal test fillet on 10 mm plate, specified as 8 mm, measures 10 mm on the bottom leg and 6.5 mm on the vertical leg, with a fine line of undercut along the top. What happened, and what is the fix?
Show solution
- The puddle sagged: metal drained from the vertical plate to the bottom plate.
- The undercut confirms that the arc melted the top toe but did not leave metal there.
- Fixes, one at a time: shorten the arc, reduce current about 10 A, keep a steady faster travel, and aim slightly toward the bottom plate near the root rather than at the face.
Answer: The weld is undersized on the vertical leg and undercut at the top; it fails both checks. Shorter arc and smaller puddle first.
On the job: Riverside stiffeners
The Riverside girders each have transverse stiffeners, plates welded across the web at intervals to keep it from buckling, and bearing stiffeners over the supports. The girder lies on its side on stands, so the stiffener-to-web fillets are horizontal fillets, made from both sides of each stiffener, and the stiffener-to-flange fillets at the ends vary in position depending on the stiffener detail. The drawings call for 8 mm (5/16 in) fillets.
The work is to CSA W59 under Hartwell's CWB certification, and because Devon is not yet qualified, Marta has arranged that Devon makes the tack welds and the first layer of selected fillets only, with Marta completing them, inspecting every one, and signing the weld map. The procedure calls for E4918-H4 (E7018-H4) in 3.2 mm and 4.0 mm, DCEP, stringer beads, cleaned between passes, with the welding sequence alternating sides of each stiffener to keep the web flat.
Two details catch Devon out on the first stiffener. The stiffener ends are clipped at the corners where they meet the web-to-flange weld, leaving a gap the fillet must wrap around without leaving a crater at the clip, and the stiffener ends near the flange must be welded around the end, a wrap or boxing, so the fillet does not stop at the edge with a crater. Marta shows Devon how to carry the arc around the end of the stiffener and back a short distance before breaking it, so the crater is on the bead, not at the corner.
Fit-up is checked before every fillet: stiffener tight to the web, square to the flange, at the marked location, tacked at both ends and in the middle. Two stiffeners have gaps over the shop limit at one end, because the web has a slight bow; Glen has them pulled tight with a clamp and re-tacked rather than filling the gap with weld.
Practice to qualification
Devon's practice for 2F goes from single-pass fillets on 10 mm (3/8 in) plate to three-pass and six-pass fillets, each with a fillet gauge check and a cross-section cut, etched and checked for root fusion, equal legs and freedom from slag. Marta also has Devon weld horizontal fillets with the joint at the back of the booth, reaching around a column, because real joints are rarely in the comfortable spot. The aim, by the end of this course, is a horizontal test fillet that passes the visual and break tests in the capstone, the same tests that, in more formal versions, check new welders before they weld on code work.
Welding both sides of a stiffener
Most stiffeners and gussets carry fillets on both sides. Welding all of one side first pulls the stiffener toward that side; welding alternately balances the pull. A common sequence is to weld a short length on one side, then the matching length on the other side, working from the middle of the stiffener toward its ends, so shrinkage is free to move toward the ends rather than locking in. Where the stiffener meets a flange as well as the web, the web fillets are usually welded first and the flange fillets last, or as the procedure directs. The welder checks the stiffener for square partway through and adjusts the sequence if it is moving.
Common mistakes
MistakeAiming the electrode at the vertical plate on a horizontal fillet.
InsteadAim into the root or slightly toward the bottom plate; the vertical plate undercuts easily.
MistakeUsing the flat-position current for a horizontal fillet.
InsteadUse a little less current so the puddle stays small enough to hold up.
MistakeWeaving to make a large horizontal fillet in one pass.
InsteadUse stringers in a bottom-up sequence for fillets over about 8 mm (5/16 in).
MistakeStarting each layer with the top pass.
InsteadStart each layer on the bottom plate so each pass rests on the one below.
MistakeStopping a stiffener fillet at the end of the plate.
InsteadWrap the weld around the end and finish back on the bead.
Summary and key terms
- In 2F the puddle sags, so the top toe undercuts and the bottom toe overlaps unless technique corrects it.
- Use a work angle of about 40 to 45 degrees favouring the bottom plate slightly, a 10 to 20 degree drag, a short arc and slightly lower current than flat.
- Single-pass horizontal fillets are kept to about 8 mm (5/16 in); larger fillets use stringers built from the bottom plate up.
- Lower the work angle for bottom passes and raise it for top passes; clean and grind valleys between passes.
- Wrap fillets around the ends of stiffeners and check fit-up and legs as the weld grows.
- 2F
- A fillet weld in the horizontal position.
- Sag
- Downward flow of the puddle under gravity.
- Stiffener
- A plate welded to a girder web to stiffen it.
- Wrap (boxing)
- Continuing a fillet weld around the end of a member.
- Weld map
- A drawing or record showing each weld, who made it and its inspection.
- Bottom-up sequence
- Placing passes in each layer from the lower plate upward.
Practice problems
Work each problem on paper first, then reveal the answer to check.
A horizontal fillet of 10 mm is specified. Is one pass enough?
Show answer
No; single horizontal passes are kept to about 8 mm, so plan multiple passes.
A horizontal fillet shows undercut at the top toe. Name two fixes.
Show answer
Shorten the arc, lower the current, aim slightly lower, or pause briefly at the top.
In which order are the passes of a layer placed?
Show answer
From the bottom plate upward.
Lesson quiz · 5 questions
Score 60% or more to complete this lesson.
Create a free account to save your progress, take quizzes and earn a certificate.