
HSE-332 · Lesson 7 of 12 · 26 min
Process safety management for facility workers
Personal safety and process safety are different. Personal safety is about the hazards that hurt one person at a time: slips, cuts, falls, pinch points and strains. Process safety is about the hazards that can kill many people at once and destroy a facility: fires, explosions and toxic releases from loss of containment. A facility can go years without a recordable injury and still be one bypassed shutdown away from disaster. Process safety management (PSM) is the set of management system elements that companies use to prevent major accidents in hazardous processes. HSE-311 teaches PSM in depth, from hazard analysis methods to safety instrumented systems. This lesson focuses on what PSM means for the people who operate and maintain oil and gas facilities day to day, and on the elements where a field worker's actions matter most.
The elements of PSM
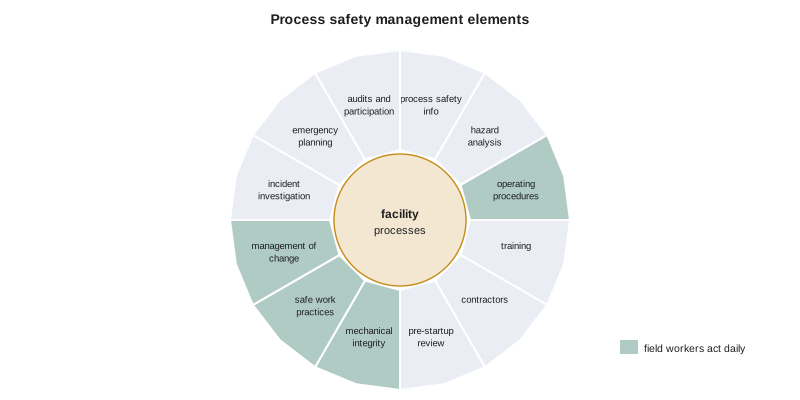
In the US, OSHA's PSM standard, 29 CFR 1910.119, and EPA's Risk Management Program list the elements that covered processes must have, and many companies apply the same elements to facilities that fall below the thresholds. In Canada, CSA Z767 sets out a similar framework. Whatever the source, the core elements are the same. They are summarized in the table below, with the part that facility workers play in each.
| Element | What it means | The worker's part |
|---|---|---|
| Process safety information | Accurate drawings, data sheets, limits and chemical hazards | Report drawings or tags that do not match the plant |
| Process hazard analysis | Systematic study of what can go wrong, such as HAZOP | Take part in studies and share field knowledge |
| Operating procedures | Written steps for start-up, normal operation, shutdown and emergencies | Follow them, and report steps that are wrong or unclear |
| Training | Initial and refresher training on procedures and hazards | Complete it and say when you are not ready for a task |
| Contractor management | Selecting, orienting and overseeing contractors | Share hazards with contractors and watch their work |
| Pre-startup safety review | Checking new or changed equipment before start-up | Walk down systems and raise anything incomplete |
| Mechanical integrity | Inspection, testing and maintenance of critical equipment | Carry out and record tests; report defects |
| Safe work practices | Permits for hot work, entry, opening and isolation | Use permits and stop when conditions change |
| Management of change | Reviewing changes before they are made | Recognize changes and raise them before acting |
| Incident investigation | Finding root causes of incidents and near misses | Report near misses and take part honestly |
| Emergency planning | Plans, drills and equipment for emergencies | Know your role and take part in drills |
| Audits and employee participation | Checking the system works and involving workers | Speak up in audits and safety meetings |
Safe operating limits
Every process has an operating envelope: the range of pressure, temperature, level, flow and composition within which equipment is designed to run safely. Process safety information documents these limits, and procedures say what to do when a variable approaches or crosses them. Typically there is a normal operating range, an alarm limit where the operator must act, and a safe operating limit or trip point beyond which the system shuts down or equipment may be damaged. Running outside the envelope, even when nothing goes wrong, uses up the safety margins that engineers built in. Operators should treat an excursion as a near miss, record it and ask why it happened.
Normalization of deviance is the process by which repeated small excursions come to feel normal. An alarm that sounds every shift is ignored; a level that runs above the high alarm becomes the new normal; a shutdown that trips often is bypassed to keep production going. Many major accidents, from refinery explosions to space shuttle losses, show this pattern. The antidote is to treat every recurring alarm, excursion and bypass as a problem to be solved rather than a nuisance to be lived with.
Management of change
Management of change (MOC) is the element field workers most often trigger, sometimes without realizing it. A change is anything other than a replacement in kind: a different valve, a new tie-in, a changed set point, a different chemical, a modified procedure, a temporary hose, a bypass, a new staffing arrangement or an extended run between inspections. Each change can introduce hazards that the original design and hazard analysis did not consider. The MOC process requires the change to be described, reviewed by people with the right expertise, approved, documented and communicated before it is made, and then checked before start-up.
A replacement in kind meets the original specification exactly: same material, rating, design and function. Anything else is a change. The table shows examples from oil and gas facilities.
| Situation | Replacement in kind or change? | Why |
|---|---|---|
| Replacing a worn gasket with an identical one from stores | Replacement in kind | Same specification and material |
| Replacing a sour service valve with a sweet service valve because it was in stock | Change | Material may crack in H2S |
| Raising a high-pressure alarm because it keeps sounding | Change | Alters a safeguard; root cause unknown |
| Adding a temporary hose to bypass a plugged line | Change | New pressure boundary and failure point |
| Switching to a different corrosion inhibitor | Change | New chemical hazards and compatibility |
| Bringing a new sour well into the battery | Change | May change H2S content, rates and pressures |
| Reducing night-shift staffing at a gas plant | Change | Affects emergency response and workload |
Temporary changes need the same review as permanent ones, plus a firm end date. Temporary hoses, clamps, bypasses and jumpers have a way of becoming permanent. Many companies track them in a register and audit it regularly.
Bypasses, overrides and alarms
Shutdowns and alarms are among the most important safeguards in a facility, and they are also the easiest to defeat. A forced input in the control system, a jumper on a switch, a closed valve on an instrument line or a muted alarm can disable a safeguard in seconds. Bypasses are sometimes necessary, for example during start-up or while an instrument is repaired, but they must be controlled: authorized by the right person, recorded, time-limited, communicated at shift handover and backed by compensating measures such as continuous monitoring by an operator.
Alarm floods are another problem. During an upset, a poorly designed alarm system can present hundreds of alarms in minutes, burying the critical ones. Alarm management programs reduce nuisance alarms and prioritize important ones so that operators can respond. Operators help by reporting nuisance and standing alarms rather than learning to ignore them.
Measuring process safety
Injury rates do not measure process safety well, because major accidents are rare and injuries are dominated by personal safety events. The industry uses process safety event indicators instead. API RP 754, widely used in both countries, classifies loss of primary containment events by severity: Tier 1 for the most serious releases, Tier 2 for lesser releases, Tier 3 for challenges to safeguards such as relief valve lifts and safe operating limit excursions, and Tier 4 for measures of system performance such as overdue inspections. Tiers 3 and 4 are leading indicators that show weaknesses before a major event. The program below classifies a year of invented events at Spruce Ridge using simplified, illustrative thresholds, not the actual tables in the standard.
# Simplified process safety event classification for an invented year at a gas plant.
# Thresholds are illustrative only; the real API RP 754 tables depend on material category.
events = [
    ("Sour gas release from flange", "release", 640, False, False),
    ("Condensate leak at pump seal", "release", 70, False, False),
    ("Small amine leak at sample point", "release", 4, False, False),
    ("Relief valve lift to flare", "safeguard", 0, False, False),
    ("High-level excursion past SOL", "safeguard", 0, False, False),
    ("Fire at compressor lube oil skid", "release", 30, True, False),
    ("Worker hospitalized after H2S exposure", "release", 15, False, True),
]
TIER1_KG, TIER2_KG = 500, 50
hours = 410_000                      # employee and contractor hours, invented

counts = {1: 0, 2: 0, 3: 0}
for name, kind, kg, fire, injury in events:
    if kind == "safeguard":
        tier = 3
    elif kg >= TIER1_KG or injury:
        tier = 1
    elif kg >= TIER2_KG or fire:
        tier = 2
    else:
        tier = 3
    counts[tier] += 1
    print(f"Tier {tier}: {name}")
for t in (1, 2):
    print(f"Tier {t} rate: {counts[t] * 200_000 / hours:.2f} per 200,000 hours")
print(f"Tier 3 events (leading signs): {counts[3]}")Tier 1: Sour gas release from flange Tier 2: Condensate leak at pump seal Tier 3: Small amine leak at sample point Tier 3: Relief valve lift to flare Tier 3: High-level excursion past SOL Tier 2: Fire at compressor lube oil skid Tier 1: Worker hospitalized after H2S exposure Tier 1 rate: 0.98 per 200,000 hours Tier 2 rate: 0.98 per 200,000 hours Tier 3 events (leading signs): 3
The plant's two Tier 1 events, one large release and one release that hospitalized a worker, would be the headline, but the Tier 3 events tell the more useful story: a relief valve lift, an excursion past a safe operating limit and a small leak are all warnings that safeguards are being challenged. Organizations that collect and act on these leading signs, through near-miss reporting and Tier 3 and 4 tracking, can fix weaknesses before they line up into a major accident.
Field workers and PSM
PSM can sound like paperwork done by engineers in offices, but most of it depends on the people in the field. Procedures only work if they match the plant and operators follow them. Hazard analyses are only as good as the field knowledge brought to them. Mechanical integrity depends on technicians who test shutdowns and relief valves properly and record what they find. Management of change depends on someone noticing that a proposed fix is a change. And incident investigation depends on people reporting near misses honestly, without fear of blame. Organizations with strong process safety cultures encourage workers to speak up, stop work and question unusual conditions, and they treat bad news as useful information.
The 2005 Texas City refinery explosion, which killed 15 workers, led to major changes in US process safety practice, including API RP 754's indicators. The 1998 Esso Longford gas plant explosion in Australia, which killed two workers and cut gas supply to the state of Victoria for about two weeks, is especially relevant to gas plants: a loss of warm oil flow let a heat exchanger chill to about −48 °C, and when operators restarted warm flow, the brittle steel failed. Both events show how weak procedures, training, alarm management and management of change can combine, and both are taught in process safety programs across the industry.
Worked problem
A nuisance alarm at Spruce Ridge
The high-level alarm on the Spruce Ridge inlet slug catcher sounds several times a night when slugs arrive from the gathering system. A night operator proposes raising the alarm set point in the control system so that it stops sounding. What should happen?
Show solution
- Recognize that changing an alarm set point is a change, not routine adjustment, because it alters a safeguard.
- Record the recurring alarm and raise it with the supervisor and the process engineer as a problem to solve.
- Investigate the cause: larger slugs from the gathering system, a level instrument fault or changes in pigging practice.
- If a set point change is justified, take it through management of change, with review of the downstream consequences and the trip settings.
- Meanwhile, keep responding to the alarm and do not mute or force it.
Answer: A nuisance alarm is a symptom. Treating it as a change and finding the cause protects the safeguard and may reveal a growing slugging problem upstream.
Common mistakes
MistakeJudging process safety by the injury rate.
InsteadTrack process safety events, excursions and leading indicators as well.
MistakeTreating a different part as a replacement in kind because it fits.
InsteadUse management of change for anything that does not match the original specification.
MistakeRaising alarm set points to stop nuisance alarms.
InsteadFind the cause and take any set point change through management of change.
MistakeLeaving a temporary bypass in place without a record.
InsteadAuthorize, record, time-limit and hand over every bypass with compensating measures.
MistakeKeeping quiet about a procedure that does not match the plant.
InsteadReport it so the procedure or the plant can be corrected.
Summary and key terms
- Process safety prevents fires, explosions and toxic releases that can kill many people; it differs from personal safety.
- OSHA PSM and EPA RMP define the elements for covered processes, and many companies apply them more widely.
- Field workers play a part in every element, especially procedures, safe work, mechanical integrity and management of change.
- Safe operating limits define the envelope; excursions and normalization of deviance erode safety margins.
- Any change other than a replacement in kind, including temporary changes and bypasses, needs management of change.
- Bypasses must be authorized, recorded, time-limited and backed by compensating measures; nuisance alarms should be fixed, not muted.
- Tiered process safety indicators, especially leading Tier 3 and 4 events, reveal weaknesses before major accidents.
- Process safety
- Preventing fires, explosions and toxic releases from loss of containment in hazardous processes.
- Operating envelope
- The range of process conditions within which equipment can run safely.
- Safe operating limit
- A limit beyond which a process may cause equipment damage or a release.
- Management of change
- A process for reviewing and approving changes before they are made.
- Replacement in kind
- A replacement that meets the original specification exactly.
- Normalization of deviance
- The gradual acceptance of abnormal conditions as normal.
- Process safety event
- An unplanned loss of primary containment or challenge to safeguards.
- Leading indicator
- A measure that signals weakness before harm occurs.
Practice problems
Work each problem on paper first, then reveal the answer to check.
How does process safety differ from personal safety?
Show answer
It addresses fires, explosions and toxic releases that can kill many people, not individual injuries.
Name four PSM elements.
Show answer
Any four of the elements in the table, such as procedures, MOC, mechanical integrity and incident investigation.
What is a safe operating limit?
Show answer
A limit beyond which the process may cause damage or a release, often with a trip.
What is normalization of deviance?
Show answer
The gradual acceptance of abnormal conditions, such as recurring alarms, as normal.
Is a sweet service valve a replacement in kind for a sour service valve?
Show answer
No, it is a change, because the material may crack in H2S.
What four things should every bypass have?
Show answer
Authorization, a record, a time limit and compensating measures, and it should be handed over at shift change.
Why are Tier 3 events valuable?
Show answer
They are leading signs that safeguards are being challenged.
Why are temporary changes risky?
Show answer
They often become permanent without proper review.
What happened at Longford?
Show answer
A heat exchanger chilled to about −48 °C and failed by brittle fracture when warm oil was restarted.
What is the first step when a nuisance alarm keeps sounding?
Show answer
Record it and raise it so the cause can be found, rather than muting it.
Lesson quiz · 5 questions
Score 60% or more to complete this lesson.
Create a free account to save your progress, take quizzes and earn a certificate.