
WLD-310 · Lesson 5 of 12 · 16 min
Shielding gas, purging and gas coverage
On carbon steel, a weld that gets a little air leaves some porosity. On stainless steel, the same air leaves a weld that looks like burnt toast on the inside of the pipe, and the chromium that was supposed to stop the line from corroding has gone into a dark oxide scale. On titanium, a little air makes the weld brittle enough to snap. GTAW depends entirely on its shielding gas, and on stainless and other reactive metals it depends on gas on both sides of the joint. This lesson covers the gases, how they change the arc, how the shield is kept intact at the torch, and how the back of a joint is purged.
Argon, helium and mixtures
Argon is the standard GTAW gas. It is heavier than air, so it settles over the work and shields well at modest flow; it ionizes easily, so the arc starts readily and is stable at low current; and it gives a smooth, narrow arc that is easy to control. Argon for welding is supplied at high purity, typically 99.995 % or better. Almost all of Hartwell's GTAW work is done in pure argon.
Helium is lighter than air and ionizes less easily, so a helium arc has a higher voltage, often several volts higher at the same current and arc length. That means more power in the arc and a hotter, wider pool with deeper penetration. Helium and argon-helium mixtures, such as 75 % argon and 25 % helium, are used on thick aluminum and copper, where the heat conducts away fast, and to raise travel speed in automatic welding. Helium needs a much higher flow, often twice as much, because it rises away from the work, and it costs more. A small amount of hydrogen, 2 to 5 %, added to argon raises the heat and gives a cleaner bead on austenitic stainless in automatic welding, but hydrogen must never be used on carbon steel, ferritic or martensitic stainless or aluminum, where it causes cracking or porosity.
| Gas | Arc | Main use at Hartwell |
|---|---|---|
| Argon | Low voltage, stable, easy start | All manual GTAW, and purge gas for stainless |
| Argon with 25 % helium | Hotter, wider pool | Thick aluminum repairs on the transformer machine |
| Argon with 2 to 5 % hydrogen | Hotter, cleaner on austenitic stainless | Not used; austenitic only, automatic welding |
| Nitrogen or forming gas (purge) | Not a shielding gas | Purging some austenitic stainless where the procedure allows |
Keeping the shield over the pool
Lesson 3 set the flow for the cup. The shield also depends on how the torch is held and what is around it. The cup must be close enough to the work for the gas to cover the pool and the hot metal behind it, which with a standard cup means a stickout no longer than the cup's bore. Tilting the torch too far, more than about 20 degrees from vertical, makes the gas flow sideways and draws air in on the trailing side. Drafts from a door, a fan or an air line can blow the shield away, and a wind of a few kilometers per hour is enough. Hartwell's booths have curtains on all sides, and in the field the welder builds a windbreak of welding blankets.
Joint design matters too. An inside corner or a groove holds the gas well. An outside corner or an edge joint lets it spill away on one side, and a fillet on the outside of a pipe has the gas flowing off over a curved surface. On those joints, a larger cup, a gas lens and a slightly higher flow help, and on stainless a trailing shield may be needed.
A trailing shield is a box or cup that clips onto the torch behind the cup and feeds a second flow of argon over the weld as it cools. It is used on titanium, where every part of the weld must stay shielded until it cools to about 800 °F, and on stainless when a bright, untinted outer surface is required. Hartwell rarely uses one on stainless, because the instrument and chemical lines on the skids are cleaned and passivated after welding, but Marta shows Devon the box in the cabinet and explains when he will need it.
Why stainless needs a back purge
When the root of a stainless joint is welded, the inside surface of the root is as hot as the outside, but on an open root there is no gas on the inside. Air reaches the hot root, and the chromium in the metal reacts with the oxygen to form a heavy, dark, flaky oxide. The result is called sugaring, because the inside of the root looks like a lump of brown sugar. A sugared root is rough, porous and loses its corrosion resistance, both because of the oxide and because the metal just beneath it has lost chromium. Sugaring must be ground out and the root rewelded. The cure is to fill the inside of the pipe or tube with argon before and during welding, called back purging.
Purging is needed on stainless, nickel alloys and titanium. On carbon steel, a GTAW root can usually be welded without a purge, although it comes out with some oxide on the inside. Many specifications call for a purge on stainless roots in any wall thickness, and for fillet and socket welds where the weld can burn through to the inside of thin tube. The Coldwater skid's chemical injection lines are 316L stainless and carry a corrosive inhibitor, so every butt weld is purged, and the inside of every weld must meet a tint limit that the client has set.
How a purge is set up
The simplest purge fills the whole line with argon. The ends are capped, one with a fitting for the gas inlet and one with a small vent at the top of the far end, the joint is taped over to keep the gas from escaping through the root opening, and argon flows in until the air has been flushed out. On a long spool this takes a great deal of gas and time, so for larger pipe, purge dams are used to seal a short section on each side of the joint. Dams can be inflatable bladders joined by a hose, soluble paper discs that dissolve when the line is flushed with water, or plugs made for the job. The smaller the volume between the dams, the faster the purge.
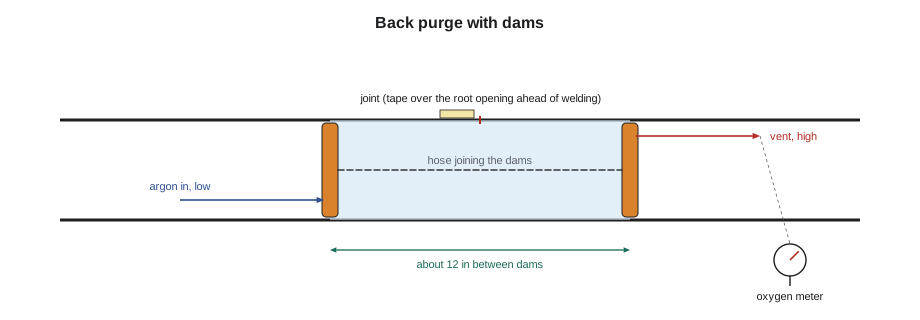
Argon is heavier than air, so it is fed in low and the air vented out high. For a horizontal line, the inlet goes at the bottom of one end and the vent at the top of the other. The vent hole must be about the same size as the inlet or a little larger, so that the purge does not build pressure. Too much pressure inside the line pushes the molten root outward into a convex bulge, or blows it out entirely. Once the root is closing, the purge flow is reduced, and at the very end, as the last of the root opening closes, the vent must still be open so the trapped gas can escape.
How long to purge
The usual rule is to flush the purged volume with at least five times its own volume of argon before welding, and then to check with an oxygen meter. Five volume changes bring the oxygen down from about 21 % in air to a fraction of one percent, if the gas mixes well. The real test is the meter, because how well the gas mixes and whether there are leaks cannot be calculated.
Here t is the purge time, V the purged volume and Q the purge flow rate. For a pipe, the volume is the inside area times the length between dams or caps.
# Purge time for a section of pipe: five volume changes at the purge flow, and the oxygen left (ideal mixing)
import math
ID = 1.097            # inside diameter, in
length = 10       # length purged, ft
flow = 30           # purge flow, cfh
vol = math.pi / 4 * ID ** 2 * length * 12 / 1728        # volume in cu ft
t = 5 * vol / flow
print(f"purged volume {vol:.3f} cu ft, 5 volume changes take {t:.1f} min at {flow} cfh")
for n in (1, 2, 3, 5, 7):
    o2 = 21 * math.exp(-n)            # percent, ideal mixing
print(f"after {n} volume changes: about {o2 * 10000:8.0f} ppm oxygen")purged volume 0.066 cu ft, 5 volume changes take 0.0 min at 30 cfh after 1 volume changes: about 77255 ppm oxygen after 2 volume changes: about 28420 ppm oxygen after 3 volume changes: about 10455 ppm oxygen after 5 volume changes: about 1415 ppm oxygen after 7 volume changes: about 191 ppm oxygen
A 10 ft length of NPS 1 schedule 10S pipe holds less than 0.07 cu ft and purges in under a minute. The same length of NPS 6 pipe holds about 2 cu ft, and a whole spool can hold many times that, which is why dams are used on larger pipe. The ideal-mixing numbers also show why five changes is a minimum, not a target: in practice the gas does not mix perfectly, and the meter often shows higher oxygen than the calculation.
Oxygen targets
Purge quality is measured in parts per million of oxygen. The level required depends on the metal and the service. A common target for general stainless process piping is below about 0.1 %, or 1,000 ppm, at the vent; for corrosive and hygienic service, where the inside of the weld must be nearly free of tint, specifications often call for much lower levels, such as 50 ppm or less, and for titanium lower still. The Coldwater client's specification calls for oxygen below 100 ppm before the root is started and a tint level no worse than a set color on the client's chart, which lesson 8 explains. Lucia Ferreira keeps the shop's oxygen meter, checks its calibration every week, and has Devon read it on every purged weld.
Purging safely
Argon displaces oxygen. Purging a pipe is safe in an open shop, but purging a vessel, a tank or a large pipe that a person might enter creates an atmosphere in which a worker can lose consciousness within seconds without any warning, because argon has no smell. The vent gas from a large purge must be led away from the welder, and any space that has been purged must be ventilated and tested before entry under the confined space rules. Priya has Devon repeat the rule back to her: purge gas is never released into a space where someone is working, and no one enters a purged vessel without a permit.
Purging small tube and fittings
Small tube and short fittings are purged in a slightly different way. A single tube joint can be purged with a small purge fitting pushed into each end, and a fitting such as a tee or an elbow is purged through its open ends with caps or tape. For socket welds on small stainless pipe, the inside of the joint is usually purged as well, because a socket weld on thin pipe can burn through to the inside. Devon's first purged tube joint takes him longer to set up than to weld, which Marta says is normal: on stainless, the purge is part of the joint preparation, and an hour spent on the purge saves a day spent cutting out sugared welds.
The purge gas is the same argon as the shielding gas, from a separate flowmeter so that the torch and the purge can be set independently. On a long line, it is good practice to start the purge well before the welder is ready, and to keep it running until the last pass is complete and the weld has cooled below the temperature at which it oxidizes. Turning the purge off as soon as the root is finished lets air back in while the hot pass reheats the root, and the inside can tint even after a perfect root.
Hartwell's purge record for each weld lists the weld number, the purge method, the oxygen reading at the start of the root and the welder's initials. On the Coldwater lines, Lucia reviews the record with the tint check, so that if a weld shows heavy tint, the record shows whether the purge was the cause.
Common mistakes
MistakePurging with the vent at the bottom of the line.
InsteadFeed argon low and vent high; argon is heavier than air.
MistakeClosing the vent as the root closes.
InsteadKeep the vent open so the purge does not blow out or bulge the root.
MistakeStarting the root after five volume changes without checking.
InsteadCheck the oxygen at the vent with a meter.
MistakeUsing argon with hydrogen on carbon steel or aluminum.
InsteadUse hydrogen mixtures only on austenitic stainless where the procedure allows.
MistakeVenting purge gas into a space where someone is working.
InsteadLead the vent away and treat purged spaces as confined spaces.
Summary and key terms
- Argon is the standard GTAW gas; helium mixtures add heat for thick aluminum and copper.
- The shield depends on flow, cup, torch angle, joint and drafts.
- Stainless roots without a purge oxidize into sugaring, which must be removed.
- Purge low in and high out, through dams or capped ends, with an open vent.
- Purge at least five volume changes and confirm with an oxygen meter.
- Argon displaces oxygen; purged spaces are confined spaces.
- Back purge
- Filling the inside of a pipe or tube with inert gas to protect the root during welding.
- Sugaring
- Heavy oxidation on the back of a stainless root welded without adequate purge.
- Purge dam
- A device that seals a pipe on each side of a joint so that only a short section is purged.
- Trailing shield
- A gas box behind the torch that keeps the cooling weld shielded.
Practice problems
Work each problem on paper first, then reveal the answer to check.
What is the inside volume of a 6 ft length of pipe with a 2.067 in inside diameter?
Show answer
pi/4 x 2.067 squared x 72 = 242 cubic inches, about 0.14 cu ft.
How long does a five-volume purge of 0.14 cu ft take at 20 cfh?
Show answer
5 x 0.14 / 20 = 0.035 h, about 2.1 minutes.
Why must the vent stay open as the root closes?
Show answer
Pressure inside would bulge or blow out the molten root.
Lesson quiz · 5 questions
Score 60% or more to complete this lesson.
Create a free account to save your progress, take quizzes and earn a certificate.