
RAC-410 · Lesson 11 of 12 · 18 min
Chiller maintenance and leak management
In January, with the plant at its lowest load and CH-2 carrying it alone on most days, Northfield took CH-1 down for its annual outage. The work list filled two pages: brush the condenser and evaporator tubes, eddy current test the tubes, change the oil and filters and send an oil sample, check the motor's insulation resistance and the starter, calibrate the sensors, test the safeties, leak test the machine and inspect the relief valves. Raj had planned it in October, ordered the parts in November and booked the eddy current contractor for the second week. "An outage is a project," he said. "If you plan it in the week you do it, you'll forget half of it."
This lesson describes the main maintenance tasks for large chillers: tube cleaning and what fouling costs, eddy current testing, oil analysis, vibration and electrical testing, and refrigerant leak inspection, repair and records under the rules that apply to large systems.
What fouling costs
Lessons 6 and 10 showed how scale and other deposits raise the condenser approach. The cost is in the lift: a warmer condensing temperature makes the compressor work harder for the same cooling. A useful rule of thumb is that each kelvin of extra condensing temperature raises a centrifugal chiller's power by about 2 to 3 %, though the exact figure depends on the machine. Heat transfer engineers describe deposits with a fouling factor, a thermal resistance added to the tube wall. AHRI ratings include a small allowance for it, as lesson 2 said; a badly scaled tube can have several times that.
The script estimates the effect of fouling on CH-1's condenser at full load, using an overall heat transfer coefficient for clean tubes and a simple model of a condensing heat exchanger, for four fouling factors from the rating allowance to heavy scale.
import math
# what condenser fouling costs CH-1 at full load (water-cooled shell-and-tube condenser)
q = 2110 + 360                                   # kW rejected at full load
m_cp = 105.0 * 4.19                              # kW/K: condenser water flow times specific heat
area = 450.0                                     # m2 of tube surface
base = None
for rf in (0.000044, 0.000088, 0.000176, 0.00035):   # fouling resistance, m2 K/W (0.00025 to 0.002 h ft2 F/Btu)
    u = 1 / (1 / 1800 + rf)                      # W/m2 K overall coefficient with fouling added
    ntu = u * area / 1000 / m_cp
    eff = 1 - math.exp(-ntu)                     # condensing side at constant temperature
    t_in = 29.4
    t_sat = t_in + q / (m_cp * eff)
    t_out = t_in + q / m_cp
    base = base or t_sat
    print(f"fouling {rf:.6f}: U {u:,.0f} W/m2K, approach {t_sat - t_out:.1f} K, condensing {t_sat:.1f} C, power about {2.5 * (t_sat - base):+.1f} %")
# tube plugging from an eddy current inspection
tubes, plugged_before, new_calls = 1180, 14, 23
print(f"tubes plugged after this outage: {plugged_before + new_calls} of {tubes} = {(plugged_before + new_calls) / tubes:.1%}")
# annualized leak rate on CH-1 (680 kg of R-134a): the rolling method
charge, added, days = 680.0, 22.0, 140
rate = added / charge * 365 / days
print(f"added {added} kg, {days} days since the last addition: annualized leak rate {rate:.1%}")fouling 0.000044: U 1,668 W/m2K, approach 1.2 K, condensing 36.3 C, power about +0.0 % fouling 0.000088: U 1,554 W/m2K, approach 1.4 K, condensing 36.5 C, power about +0.5 % fouling 0.000176: U 1,367 W/m2K, approach 1.8 K, condensing 36.9 C, power about +1.5 % fouling 0.000350: U 1,104 W/m2K, approach 2.7 K, condensing 37.7 C, power about +3.6 % tubes plugged after this outage: 37 of 1180 = 3.1% added 22.0 kg, 140 days since the last addition: annualized leak rate 8.4%
At the rating allowance, the condenser approach was about 1.2 K. Doubling the fouling raised it to 1.4 K; four times, to 1.8 K; and at about eight times, heavy scale like that from the water treatment failure, it reached 2.7 K, close to the action limit, raising the compressor power by about 3.6 % at full load. That may sound small, but on a 2,110 kW (600-ton) chiller running thousands of hours a year it is real money, and scale also lowers the chiller's capacity on the hottest days and can lead to high-pressure trips. The model is simplified; the manufacturer's selection program can calculate the effect for a specific machine.
Tube cleaning
Condenser tubes on open tower systems are cleaned at least once a year, and more often if the approach rises. The usual method is mechanical: the water boxes are opened, and a rotating brush on a flexible shaft, with water flushing through, is run through each tube, followed by a visual check with a light. Hard scale may need chemical cleaning, circulating an inhibited acid solution under the water treatment company's control, followed by neutralizing and flushing, because acid left in the tubes or used too strongly damages them. Evaporator tubes in closed chilled-water loops foul much less and are cleaned less often, often every few years, or when the evaporator approach or pressure drop shows the need.
Opening a water box is a maintenance task with its own care: isolating and draining the water side, supporting the heavy box covers with a davit or hoist, protecting the gasket surfaces, inspecting the tube sheets and the box coating for corrosion, checking the sacrificial anodes where fitted, and replacing the gaskets with the correct ones and tightening the bolts in the right pattern to the right torque. After closing, the water side is refilled, vented and checked for leaks before the chiller runs.
Eddy current testing
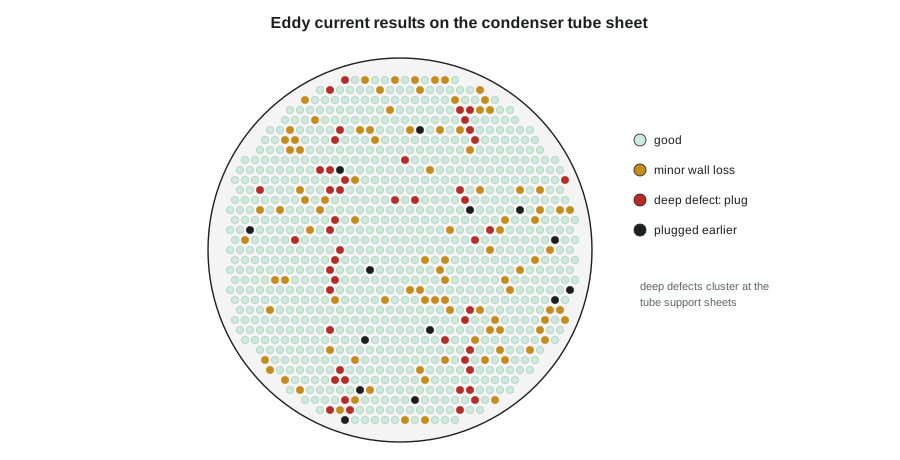
Tubes fail from the inside, where the water erodes and corrodes them, and from the outside, where vibration at the support sheets wears them, or where freezing in the evaporator splits them. A tube leak in a condenser or evaporator lets water into the refrigerant circuit or refrigerant into the water, which can wreck the compressor and the charge. Eddy current testing finds weak tubes before they leak. A probe passed through each tube induces electrical currents in the tube wall, and the instrument detects changes in the wall thickness and defects such as pits, cracks and wear at the supports. The results are given as a map of the tube bundle showing each tube's condition, usually as a percentage of wall loss.
Tubes with deep defects are plugged at both ends, which takes them out of service. Each plugged tube reduces the heat exchanger's surface and raises the water velocity in the others. Manufacturers give a guide to how many tubes can be plugged before performance or velocity limits are reached, often on the order of 10 % of the tubes, and when many tubes are failing the bundle is retubed. CH-1's results showed 23 new tubes with deep defects at the support sheets, which with 14 plugged in earlier years brought the total to about 3 % of the condenser's tubes. The report recommended plugging them and testing again in two years instead of three, because the support wear was progressing.
Oil, vibration and electrical tests
On machines with lubricated bearings, the oil is sampled and sent to a laboratory at least yearly, and the results are trended. The analysis reports the oil's condition, acid, moisture and viscosity, and the metals in it, which come from wearing bearings, gears and seals, so a rising level of one metal can point to a part before it fails. An acid result also warns of moisture or a motor winding problem on a hermetic or semi-hermetic machine, as RAC-210 described for burnouts. The oil filters are changed, and on some machines the oil itself, according to the manufacturer and the analysis.
Vibration readings at the compressor and motor bearings, taken with a portable analyzer on a regular schedule, detect imbalance, misalignment, bearing wear and gear problems, much as on the pumps in lesson 8. Riverbend's service plan took readings every quarter on all three chillers and the large pumps.
The motor and starter or drive get electrical tests: insulation resistance of the motor windings, with the result corrected for temperature and trended, as RAC-130 lesson 5 showed for the chiller compressor; inspection and tightening of power connections, ideally with a thermographic scan under load first to find hot connections; testing of the starter or drive's protective settings; and checks of the control power and safeties. Electrical work on these machines, at 600 V and high currents, follows the electrical safety practices of RAC-130, with lockout and arc flash precautions.
The safeties are tested, not just inspected: low evaporator pressure and temperature, high condenser pressure, flow switches, oil pressure and motor protection, using the manufacturer's procedures. Sensors that feed the chiller panel and the plant controls are checked against calibrated instruments, because, as lesson 9 noted, a wrong sensor can make the whole plant run badly.
Relief devices
Large chillers are protected by relief valves or rupture discs, which release refrigerant if the pressure in the vessel rises dangerously, for example in a fire. Their discharges are piped outdoors, as lesson 3 described. Relief valves are inspected for corrosion, leakage and blockage of the vent line, and replaced on a schedule set by the code and the manufacturer, because they can stick or leak after years in service; rupture discs are inspected and replaced if damaged. Some plants fit a pressure gauge or leak detector between a rupture disc and a relief valve in series, to show if the disc has leaked. In Ontario, the pressure vessels and their relief devices are also under TSSA's boiler and pressure vessel requirements.
Leak inspection, repair and records
A large chiller's charge is valuable, and its loss is regulated. RAC-120 explained the rules in detail; for a technician on a large system the key parts are these.
In Ontario, O. Reg. 463/10 applies to the halocarbon refrigerants in CH-1 and CH-3. The system must be leak tested as the code of practice requires, a leak must be repaired before the system is recharged, a refill is allowed only with a leak test notice showing no leaks, records of service and refrigerant added must be kept, and a discharge of 100 kg or more must be reported. Federally, the Federal Halocarbon Regulations, 2022 apply to systems on federal lands and federal works, and ODSHAR now prohibits the manufacture and import of new chillers using refrigerants with a GWP above 750, though existing chillers like CH-1 may continue to be serviced.
The leak rate calculation, which RAC-120 lesson 11 showed, annualizes the refrigerant added since the last addition. Theo calculated it for CH-1 after a top-up in December. The machine had needed 22 kg of R-134a, 140 days after its previous addition: an annualized rate of about 8.4 %. Under Ontario's rules, the size of the rate did not matter; the leak had to be found and repaired before the machine was recharged, which is why the outage included a full leak test. The leak turned out to be at a flare fitting on a pressure transducer line, a common place, and at a weeping gasket on the oil filter housing.
Leak inspection on a large machine combines methods from RAC-120: an electronic detector around joints, valves, gaskets, sensor fittings and the shaft seal on open-drive machines; bubble solution on suspect points; ultrasonic detectors in noisy rooms; and the refrigerant monitor's low-level history from lesson 3. Low-pressure machines are leak tested by pressurizing them slightly with dry nitrogen or warm water in the tubes, or by a standing vacuum test, as the manufacturer specifies. Every leak inspection, repair, refrigerant addition and recovery is recorded with dates, quantities and the technician's certification, in the chiller's log and the owner's refrigerant records.
Planning the outage and the record
A good maintenance program is planned, recorded and reviewed. Raj's plan for the Riverbend chillers set each task's frequency from the manufacturer's recommendations, the codes and the plant's history, and staggered the outages so that two machines were always available. Each outage ended with a report: what was done, what was found, the test results, readings before and after, parts replaced and recommendations. After CH-1's outage, its condenser approach was back to about 1.1 K (2 °F) at the next full load in spring, the leak checks were clean, the oil analysis was normal, and the eddy current report set the date for the next test. Theo filed the report beside the 2009 start-up report. "Every one of these makes the next diagnosis easier," Raj said.
Common mistakes
MistakeCleaning tubes without fixing the water problem that fouled them.
InsteadFind and correct the cause first, as in lesson 6.
MistakePlugging leaking tubes without testing the rest of the bundle.
InsteadEddy current test to find weak tubes before they fail.
MistakeTopping up a leaking chiller without calculating the leak rate.
InsteadCalculate and record the rate every time refrigerant is added, and follow the rules that apply.
MistakeAssuming a leak below the threshold can be ignored.
InsteadFind and repair it anyway; refrigerant costs money and leaks grow.
MistakeTesting safeties by inspection only.
InsteadOperate each safety and record the result.
Summary and key terms
- Fouling raises condenser approach and lift, costing energy and capacity; tubes on tower systems are cleaned at least yearly.
- Eddy current testing maps tube wall loss so weak tubes can be plugged before they leak; bundles are retubed when too many fail.
- Oil analysis, vibration readings and electrical tests catch wearing parts and failing insulation early.
- Safeties and sensors are tested and calibrated; relief devices are inspected and replaced on schedule.
- Refrigerant leaks are found, repaired and recorded under O. Reg. 463/10 and federal rules, with leak rates calculated at each addition.
- Outages are planned in advance, and each one's report becomes part of the chiller's history.
- Fouling factor
- An added thermal resistance representing deposits on heat transfer surfaces.
- Tube brushing
- Mechanical cleaning of heat exchanger tubes with rotating brushes.
- Eddy current testing
- A non-destructive test that measures tube wall condition with induced electrical currents.
- Plugged tube
- A tube sealed at both ends to remove it from service.
- Retubing
- Replacing the tubes of a heat exchanger bundle.
- Oil analysis
- Laboratory testing of oil for condition, contaminants and wear metals.
- Rupture disc
- A pressure relief device that bursts at a set pressure.
- Annualized leak rate
- Refrigerant added, as a fraction of the charge, scaled to a one-year period.
Practice problems
Work each problem on paper first, then reveal the answer to check.
A chiller's condensing temperature is 2 K (4 °F) higher than its baseline at the same conditions. Roughly how much more power does it use?
Show answer
About 4 to 6 %.
A condenser has 900 tubes and 54 are plugged. What percentage is that?
Show answer
6 %.
A 400 kg chiller needs 10 kg of refrigerant 120 days after its last addition. What is the annualized leak rate?
Show answer
About 7.6 %.
Why are oil samples trended instead of judged one at a time?
Show answer
Rising wear metals or acid over time point to developing problems.
Lesson quiz · 5 questions
Score 60% or more to complete this lesson.
Create a free account to save your progress, take quizzes and earn a certificate.