
CHE-480 · Lesson 1 of 12 · 27 min
Environmental engineering in the process industries and regulation
The board of Kingfisher Bioenergy approved the expansion of the Cedar Rapids plant in September, with one condition attached. The plant makes about 200 million liters (about 53 million gallons) of fuel ethanol a year today, and the expansion will lift that to about 240 million liters (63 million gallons) a year: a new 2,600 m³ fermenter and a second yeast propagator, a larger distillation and evaporation train, a third DDGS dryer section, the new fermentation vent scrubber that Theo Laurent designed in CHE-314, and the bio-based ethyl acetate line studied in CHE-446. The condition was a single document. Before the money is released, the board wants an environmental compliance and carbon reduction plan that shows how the expanded plant will meet every permit limit, what it will cost to do so, and how far the plant can cut the carbon intensity of its ethanol over the next ten years.
The plan belongs to Wren Halvorsen, the plant's environmental compliance lead. Wren has looked after the plant's permits for six years. She runs the stack tests, signs the monthly discharge reports to the city, files the annual inventory reports and answers the calls from the regulator when a neighbor complains about the smell of the dryers on a humid evening. Malik Osei, the plant manager, has given her Theo for the next nine months; he is now an engineer-in-training back from his secondment to the refinery. Ingrid Solheim, the engineering manager and a licensed PE who will seal the technical work, will review each part. Nadia Brandt (process safety), Priya Venkat (industrial hygiene) and Dev Raman, who runs the laboratory, will be pulled in when their areas come up.
This course follows that plan from start to finish. It covers how environmental law applies to a process plant, how air pollutants are released and disperse, how particulate and gaseous emissions are controlled, how combustion produces nitrogen and sulfur oxides, how industrial wastewater is characterized, pretreated and treated biologically, how water can be reused, how solid and hazardous wastes are classified and managed, how a life-cycle assessment is done, and how a plant accounts for and reduces its carbon. It ends with the plan itself. The course builds on the mass and energy balances of CHE-200, mass transfer in CHE-314 and the design and economics methods of CHE-446.
What environmental engineering means in a process plant
A chemical or biochemical plant converts raw materials into products, and almost never with a 100 % yield. Every unit operation also produces something that is not sold: a vent gas, a purge, a wash water, a filter cake, a spent catalyst, waste heat, carbon dioxide. Environmental process engineering is the discipline that deals with those streams. It has four tasks. The first is to know them: to measure or estimate every release to air, water and land, with its composition and its variability. The second is to prevent or reduce them at the source by changing the process. The third is to treat what remains so that it meets the limits set by law and by the plant's own commitments. The fourth is to show, with records and reports, that the plant has done all of this.
Wren's first lesson to Theo is that environmental engineering is process engineering. The same mass balance that sizes a distillation column also tells you how much ethanol leaves in the fermentation vent. The same energy balance that sizes a boiler tells you how much carbon dioxide and nitrogen oxide it releases. A pollutant is simply a component of a stream that happens to leave the plant boundary, and it obeys the same conservation laws as the product. An environmental engineer who cannot close a mass balance cannot defend an emission estimate to a regulator.
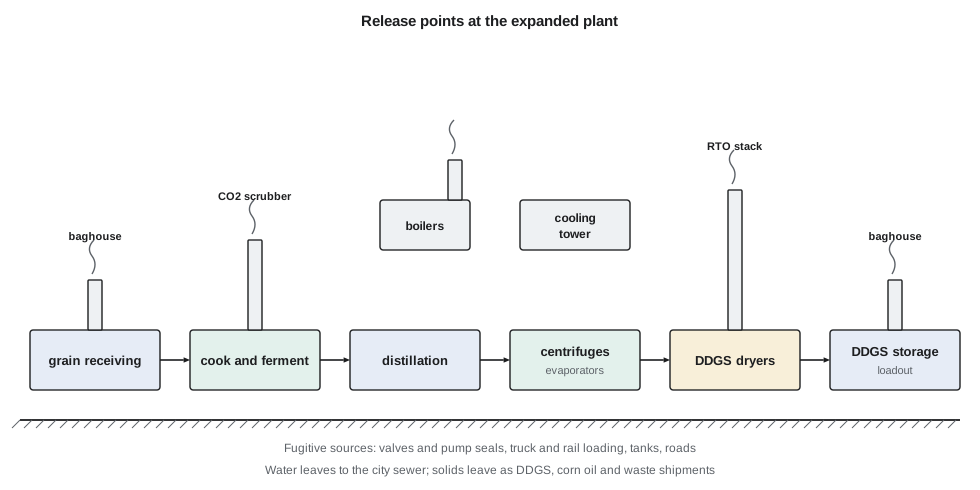
The release points of a dry-grind ethanol plant
The Cedar Rapids plant is a dry-grind corn ethanol plant, and its releases are typical of the industry. Corn arrives by truck and rail and is unloaded into pits; the dust is collected by baghouses. The corn is ground, cooked with enzymes and fermented by yeast, which turns starch into ethanol and an almost equal mass of carbon dioxide. That carbon dioxide leaves the fermenters saturated with water and carrying about 1.5 mol % ethanol, together with small amounts of acetaldehyde and other organics; the vent scrubber recovers the ethanol and sends the cleaned gas up a stack. The beer is distilled, the stillage is centrifuged, the thin stillage is evaporated to syrup, and the wet cake and syrup are dried in natural-gas-fired dryers to make distillers dried grains with solubles (DDGS). The dryers are the largest single source of particulate matter, volatile organic compounds (VOC), carbon monoxide and nitrogen oxides at the plant; their exhaust goes through cyclones and a regenerative thermal oxidizer (RTO) before its stack. Package boilers make the steam. A cooling tower rejects heat and releases a little particulate as drift. Tanks, loading racks, valves and pump seals release small amounts of ethanol vapor.
Water leaves the plant in fewer places than one might expect. A dry-grind plant recycles most of its process water: thin stillage returns to the cook as backset, and evaporator condensate is reused. What reaches the sewer is mostly cooling tower blowdown, boiler blowdown, reject from the water treatment system and the wash water from cleaning-in-place (CIP). Solid streams are the DDGS and corn oil, which are products, plus a list of wastes from the laboratory, maintenance and the control equipment itself. Lesson 9 takes up that list.
The regulatory framework
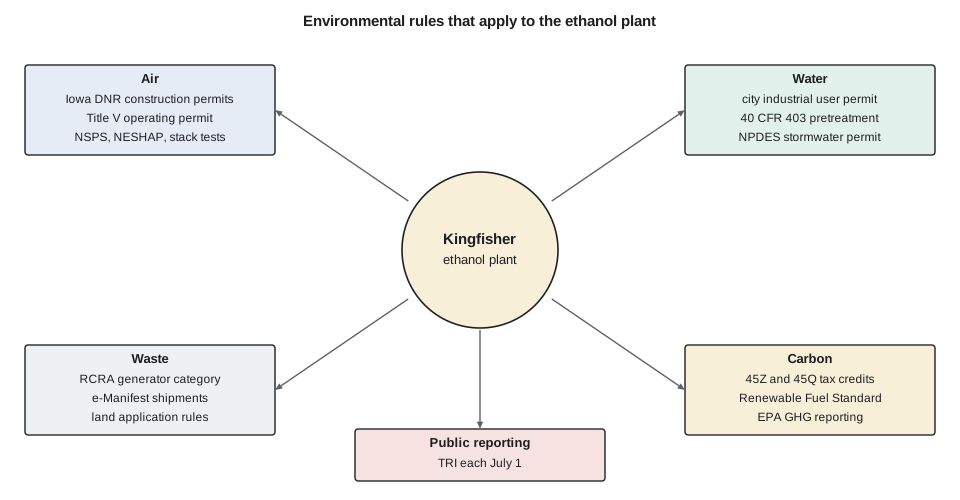
Environmental law in the US works through a small number of instruments that every process engineer should recognize. Air emissions at the Cedar Rapids plant are governed by the federal Clean Air Act, which Iowa DNR carries out through its construction permit and Title V programs. Water is governed by the federal Clean Water Act, which governs direct discharges through NPDES permits and indirect discharges to a city sewer through the general pretreatment regulations in 40 CFR 403, together with the city's sewer use ordinance. Waste is governed by Subtitle C of the Resource Conservation and Recovery Act (RCRA), which defines hazardous waste by listing and by characteristic and sets rules by generator category. Workplace exposure, which overlaps with environmental work at every vent and drain, falls under the OSH Act and OSHA rules. The plant reports its releases to the public through EPA's Toxics Release Inventory (TRI), and its greenhouse gases through EPA's Greenhouse Gas Reporting Program, which has applied to facilities emitting 25,000 t CO₂e or more a year; EPA proposed in 2025 to end the program for most source categories, and the plant keeps its records either way. Its carbon emissions are priced, or rewarded, through no carbon price; instead, federal tax credits reward low carbon intensity (the section 45Z clean fuel production credit) and stored carbon dioxide (section 45Q). Its ethanol is sold into markets shaped by the federal Renewable Fuel Standard and the section 45Z clean fuel production credit.
The most important instrument for an existing plant is its permit. At Cedar Rapids, air emissions are authorized by an Iowa DNR air construction permit for each emission unit, with the conditions carried into the plant's Title V operating permit. The permit lists every emission unit, its control equipment, its limits, how compliance is shown (by stack tests, continuous monitors, parametric monitoring such as RTO chamber temperature, or record-keeping), and what must be reported. Any change that alters emissions, which includes almost every part of the expansion, needs an amendment before construction starts. Wren's experience is that the permit amendment sets the critical path of the whole project, because the regulator's review can take many months and cannot begin until the design is far enough along to estimate emissions with confidence.
Command and control, and market instruments
Most environmental rules are of the type called command and control: a limit on concentration or mass rate, or a required technology, written into a permit and enforced by inspection and penalties. They work well for pollutants with local effects, such as particulate near a fence line or ammonia in a receiving stream, because the limit can be set to protect the people and the water nearby. For pollutants with diffuse effects, especially greenhouse gases, governments increasingly use market instruments that put a price on the pollutant and leave each plant to find the cheapest way to cut it. A carbon price, a tradable credit system for fuel carbon intensity and a tax credit for stored carbon dioxide are all market instruments. Lessons 10 to 12 deal with them in depth. Here it is enough to see that a plant's environmental performance now has two faces: compliance, which is binary and is checked against a permit, and carbon, which is continuous and shows up in the profit and loss account.
Potential to emit and the emission inventory
The quantity that drives most air permitting decisions is the potential to emit (PTE): the maximum a unit could release at its full design capacity, operating every hour of the year, with its control equipment counted only if the control is legally required by an enforceable permit condition. Actual emissions are usually much lower, but the permit category is set by potential, not by what the plant happens to do. Wren's first job is therefore an emission inventory of the expanded plant: a table of every emission unit with its PTE for each pollutant. The rates come from the vendor guarantees for new equipment, stack tests on existing units, emission factors for small or fugitive sources, and mass balances where nothing better exists.
# Potential-to-emit inventory for the expanded plant against the Clean Air Act major-source thresholds
HOURS = 8760                       # potential to emit assumes continuous operation
TON = 907.185                      # kg per short ton; US permit thresholds are in tons per year (tpy)
src = {
 'DDGS dryers via RTO':  {'PM10': 3.2, 'PM2.5': 2.6, 'VOC': 3.5, 'CO': 6.0, 'NOx': 7.5, 'SO2': 4.9},
 'Fermentation scrubber': {'VOC': 1.2},
 'Steam boilers':        {'PM10': 0.4, 'PM2.5': 0.4, 'VOC': 0.4, 'CO': 4.4, 'NOx': 4.4, 'SO2': 0.04},
 'Grain and DDGS dust':  {'PM10': 0.9, 'PM2.5': 0.2},
 'Cooling tower':        {'PM10': 0.3, 'PM2.5': 0.01},
 'Loadout, leaks, tanks': {'VOC': 1.6},
}
pols = ['VOC', 'NOx', 'CO', 'SO2', 'PM10', 'PM2.5']
tot = {p: sum(d.get(p, 0) for d in src.values()) * HOURS / TON for p in pols}
print(f"{'pollutant':10s}{'tpy':>8s}  Title V (100)  PSD (250)")
for p in pols:
    print(f"{p:10s}{tot[p]:8.1f}  {'major' if tot[p] >= 100 else 'below':13s}  {'major' if tot[p] >= 250 else 'below'}")
haps = {'acetaldehyde': 0.45, 'formaldehyde': 0.15, 'methanol': 0.25, 'acrolein': 0.05}
hap = {k: v * HOURS / TON for k, v in haps.items()}
print(f"largest single HAP {max(hap, key=hap.get)} {max(hap.values()):.1f} tpy (major at 10)")
print(f"total HAPs {sum(hap.values()):.1f} tpy (major at 25)")pollutant tpy Title V (100) PSD (250) VOC 64.7 below below NOx 114.9 major below CO 100.4 major below SO2 47.7 below below PM10 46.3 below below PM2.5 31.0 below below largest single HAP acetaldehyde 4.3 tpy (major at 10) total HAPs 8.7 tpy (major at 25)
The expanded plant is above 100 tons per year (tpy) of nitrogen oxides and carbon monoxide, so it is a major source under Title V, as the existing plant already is. It stays below 250 tpy for every pollutant. That number matters because of a 2007 EPA rule that moved fuel ethanol plants out of the list of 28 source categories with a 100 tpy threshold for Prevention of Significant Deterioration (PSD); since then, an ethanol plant is a PSD major source only at 250 tpy. Staying below that line avoids a PSD review with its best available control technology analysis and its air quality modeling of increments, which can add a year to a project. The plant is also an area source for hazardous air pollutants (HAP), below 10 tpy of any single HAP and 25 tpy in total, so the major-source NESHAP rules do not apply to it.
Theo notices that carbon monoxide sits at 100.4 tpy, just over the line. Wren explains that this is exactly the kind of number a permit engineer looks at twice. If the plant took an enforceable limit on dryer and boiler carbon monoxide that kept the total below 100 tpy, it would not change its Title V status, because nitrogen oxides are already over, but for PSD the same idea, called a synthetic minor limit, is often used to keep a plant below 250 tpy. The plant then has to monitor and report against that limit, and a breach becomes a permit violation rather than just a high number.
Worked problem
Converting a rate to an annual potential
The new third dryer section will add 1.1 kg/h of VOC after the RTO. What is its potential to emit in metric tons per year?
Show solution
- Potential to emit assumes 8,760 h/yr of operation at the permitted rate.
- \(1.1 \times 8\,760 / 1\,000 = 9.6\) t/yr.
- On the US basis this is \(9.6 / 0.907 = 10.6\) short tons per year.
Answer: About 9.6 t/yr (10.6 tons per year).
The pollution prevention hierarchy
Environmental agencies and engineers rank the options for dealing with a release in a hierarchy. The first choice is to prevent the release at the source: change the chemistry, the equipment or the operating practice so the pollutant is never formed or never leaves the process. The second is to recover and reuse it inside the plant. The third is to recycle it off site. The fourth is to treat it, destroying it or converting it to something harmless. The last is to dispose of it, by release within permitted limits or by landfill. The hierarchy is a guide, not a law of nature: sometimes treatment is cheaper and better than a doubtful process change. But it is a strong guide, because prevention removes the cost of treatment, the risk of the treatment failing and the waste the treatment itself creates.
The vent scrubber is a good example of the higher steps. Without it, about 286 kg/h of ethanol would leave the fermentation vent: a large VOC source and a loss of product. With it, about 285 kg/h is recovered and returned to the process, and about 1 kg/h reaches the stack. The scrubber is classed as control equipment in the permit, but in the hierarchy it is recovery and reuse, and it pays for itself in recovered ethanol. The RTO on the dryers, by contrast, is treatment: it destroys VOC by burning it and uses natural gas to do so. Lessons 3 and 4 will ask whether any of the dryer VOC can be prevented instead.
| Step | Example at the plant | What it costs |
|---|---|---|
| Prevent at source | Lower dryer temperature cuts VOC formation | Process change, possible capacity loss |
| Recover and reuse | Vent scrubber returns ethanol to the process | Capital; earns product back |
| Recycle off site | Used oil and scrap metal sent to recyclers | Small handling cost |
| Treat | RTO burns dryer VOC; anaerobic reactor treats wastewater | Capital, fuel, operating labor |
| Dispose | Spent RTO media to landfill; treated water to sewer | Fees, long-term liability |
Monitoring, records and the compliance cycle
A permit is only as good as the evidence that the plant meets it. Compliance at Cedar Rapids rests on four kinds of evidence. Stack tests measure emissions directly under defined conditions, usually at the start of operation and every few years after. Continuous or parametric monitoring shows that the control equipment is working between tests: the RTO chamber temperature, the scrubber water flow and pH, the baghouse pressure drop. Records show what the plant processed and when equipment was down. Reports, monthly to the city for wastewater and annually for the inventories and the permit, bring the evidence together. Wren keeps a compliance calendar with more than two hundred dated obligations a year, and she treats a missed report with the same seriousness as an exceedance, because regulators do.
When something goes wrong, the plant must know what to do. A spill to the ground or a sewer, a bypass of the RTO, or a discharge outside its limits must be reported to the regulator within the time the rules require, contained, cleaned up and investigated. Wren's spill response procedure is drilled twice a year with the operators, and Nadia Brandt's process safety program shares the same incident system. An environmental incident is usually a process incident that happened to leave the site.
Professional responsibility
Environmental work carries professional duties. Emission estimates and modeling submitted to a regulator are engineering documents and are prepared or reviewed by a licensed PE registered with the Iowa Engineering and Land Surveying Examining Board. Falsifying a record or knowingly submitting a wrong estimate is an offense, and in serious cases the individual who signed can be prosecuted, not only the company. Wren tells Theo that the most valuable habit he can build is to write down the basis for every number he produces: the source, the assumption, the date. Six years from now, when a stack test disagrees with the estimate, someone will need to know where the estimate came from.
Common mistakes
MistakeUsing actual emissions to decide the permit category.
InsteadPermit categories are set by potential to emit: full capacity, 8,760 h/yr, with only enforceable controls counted.
MistakeTreating environmental work as separate from process engineering.
InsteadEmission estimates are mass and energy balances; the process design decides most of the releases.
MistakeAssuming a reporting threshold is an emission limit.
InsteadInventory thresholds trigger reporting only; limits come from permits and ambient standards.
MistakeJumping straight to end-of-pipe treatment.
InsteadCheck prevention and recovery first; they avoid treatment cost and the wastes treatment creates.
MistakeLeaving the permit amendment until the design is finished.
InsteadThe regulator's review is often on the critical path; start early with conservative estimates.
Summary and key terms
- Environmental process engineering identifies, prevents, treats and documents every release to air, water and land.
- A dry-grind ethanol plant's main air sources are the DDGS dryers, the fermentation vent, the boilers and fugitive sources; its main water discharge is utility blowdown and CIP water.
- Air, water and waste each have their own laws and permits; greenhouse gases are handled by reporting and by market instruments.
- Potential to emit at full capacity and 8,760 h/yr sets the permit category.
- The hierarchy runs prevent, recover and reuse, recycle, treat, dispose.
- Compliance rests on stack tests, monitoring, records and reports, signed by accountable professionals.
- Emission unit
- A piece of equipment or activity with its own emissions and permit conditions.
- Potential to emit (PTE)
- The maximum emissions at full design capacity and continuous operation, counting only enforceable controls.
- Emission inventory
- A table of releases of each pollutant from each source at a facility.
- Command and control
- Regulation by fixed limits or required technology written into permits.
- Market instrument
- Regulation that prices a pollutant or creates tradable credits.
- Parametric monitoring
- Monitoring an operating variable, such as oxidizer temperature, that shows a control device is working.
Practice problems
Work each problem on paper first, then reveal the answer to check.
Why does the permit category depend on potential rather than actual emissions?
Show answer
The permit must cover what the plant could legally do at full capacity, not what it happened to do last year.
A unit emits 0.5 kg/h of PM10. What is its PTE?
Show answer
\(0.5 \times 8\,760 / 1\,000 = 4.4\) t/yr.
Where in the hierarchy does the vent scrubber sit?
Show answer
Recovery and reuse: it returns ethanol to the process.
Name three kinds of compliance evidence.
Show answer
Stack tests, continuous or parametric monitoring, and records and reports.
Which plant unit dominates VOC and combustion pollutants?
Show answer
The DDGS dryers, with their RTO.
Why is the permit amendment often on the critical path?
Show answer
Review takes months and cannot start until emissions can be estimated from the design.
Lesson quiz · 5 questions
Score 60% or more to complete this lesson.
Create a free account to save your progress, take quizzes and earn a certificate.