
BLR-310 · Lesson 9 of 12 · 20 min
Heads: types, layout and fitting
V-414's heads arrive from the head maker in late January, two 2:1 ellipsoidal heads strapped to a pallet with their straight flanges up. Harjit's receiving inspection is the first job: check the paperwork, the markings, the shape and the dimensions before anyone marks a nozzle or offers a head to the shell. Joanne uses the morning to teach Kiera about heads in general. "You'll never lay out a head the way you lay out a cone," she says. "But you'll order them, check them, cut holes in them and fit them to every vessel you build. You need to know the shapes, what the head maker needs from you, and how to find any point on the surface." This lesson covers the common head types and their proportions, what a head order specifies, how a head maker sizes a blank, how heads are inspected on arrival, and how points and nozzle positions are found on a formed head.
Why heads are bought, not developed
Lesson 1 explained that a head curves in two directions at once, so it cannot be made from flat plate without stretching. Head makers form heads by pressing a heated or cold blank between dies, by spinning it on a large lathe-like machine while rollers force it over a form, or, for very large heads, by pressing segments, called petals, and welding them together with a crown piece. The forming thins the plate in some places, especially in the knuckle of a torispherical head and the crown of a deep head, so the head maker starts with plate thicker than the finished minimum and certifies the minimum thickness after forming. That certified minimum, not the nominal plate thickness, is what the vessel's design relies on.
Head types and their proportions
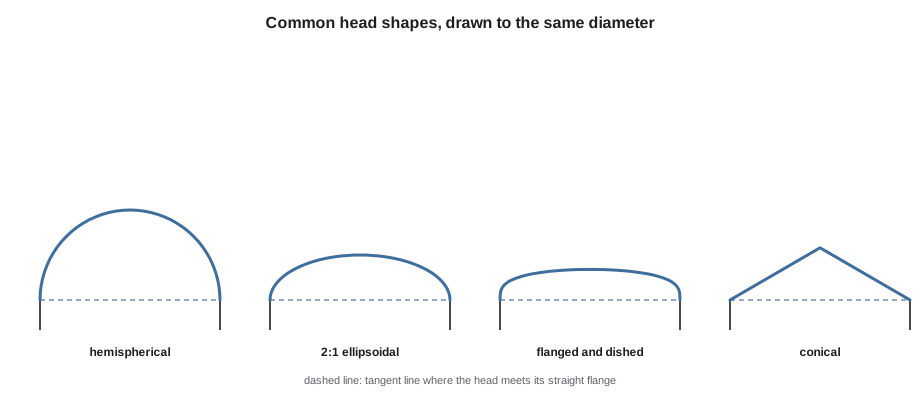
Four head shapes cover most boilermaker work. A hemispherical head is half a sphere, with a depth equal to its radius. It is the strongest shape for its thickness and the deepest, used on high-pressure vessels and large spheres, where the thinner plate it allows pays for the forming. A 2:1 ellipsoidal head has a cross-section that is half an ellipse whose major axis is twice its minor axis, so its inside depth is a quarter of its inside diameter. It is the most common head on pressure vessels in the middle range of pressure and size. A torispherical, or flanged and dished, head has a spherical crown of large radius joined to its straight flange by a tight knuckle, a toroidal band of small radius; it is shallower than an ellipsoidal head and cheaper to form, and it is used on lower-pressure vessels and tanks. A conical head is a cone, with or without a knuckle at its base, used where solids must drain.
ASME Section VIII, Division 1 gives design rules for all of these in its rules for formed heads, UG-32, and for cones in UG-33 and its mandatory appendix on cone-to-cylinder junctions. For a standard ASME flanged and dished head, the crown radius equals the head's outside diameter and the knuckle radius is 6 percent of it, the smallest knuckle the code allows for that crown. Other common torispherical proportions include the 10 percent knuckle head and the 80-10 head, with a crown radius of 80 percent and a knuckle of 10 percent of the diameter. A 2:1 ellipsoidal head behaves, for design purposes, much like a torispherical head with a crown radius of about nine-tenths of its diameter and a knuckle of about one-sixth, which is why some drawings show it that way.
| Head | Inside depth (approximate) | Typical use |
|---|---|---|
| Hemispherical | ½ × inside diameter | High pressure, spheres, large thin vessels |
| 2:1 ellipsoidal | ¼ × inside diameter | Most pressure vessels |
| ASME flanged and dished (6 % knuckle) | About 0.17 × inside diameter | Low and moderate pressure |
| Conical (30 degree half apex) | Depends on the angle | Hoppers, drains, solids handling |
What a head order says
A head is ordered by its type, its diameter, its minimum thickness after forming, its material and its straight flange. The diameter is given as inside or outside, and the difference matters: a head ordered to the shell's inside diameter will have an outside diameter of the inside diameter plus twice the head's actual thickness, which may not match the shell's outside diameter if the head is thicker than the shell. Most shops order heads to the inside diameter when the vessel's design is on the inside diameter, as V-414's is.
The straight flange is the short cylindrical band on the head's edge, between the tangent line, where the curved surface ends, and the edge. It moves the head-to-shell weld away from the knuckle, where stresses from the change in shape are highest. V-414's heads have a 50 mm (2 in) straight flange. The order also gives the edge preparation, a bevel for the head-to-shell weld or a square edge to be bevelled in the shop; any nozzle openings the head maker is to cut; and the inspection and certification required, including the minimum thickness report, the material certificates and, for an ASME code vessel, the head maker's partial data report.
The blank
Head makers size the flat blank so that the formed head has enough material for its surface and its straight flange, plus a trim allowance. The blank size is a head maker's figure, but a boilermaker sometimes needs to estimate it, to check a quotation or to order plate for a head the shop will have formed elsewhere from its own material. A simple estimate equates the area of the blank to the area of the head's mean surface plus its straight flange, which gives a blank diameter about 1.2 times the head's diameter for a 2:1 ellipsoidal head and about 1.4 times for a hemispherical head, before trim. Forming does not preserve area exactly, which is why the head maker's figure, from experience with their own dies, always governs.
Kiera's numbers for V-414's heads
Kiera runs the shop code on V-414's head: inside diameter 1,800 mm (72 in), thickness 16 mm (5/8 in), straight flange 50 mm (2 in). It gives the depth of three head types for comparison, the blank estimates for two of them, and the height and slope of the 2:1 head's surface at 500 mm (20 in) from its centre, where the top head's vapour outlet goes on V-414.
# Heads: depth and an estimate of the blank diameter (metric)
import math
from math import gcd
MODE = "mm"

def frac(x, den=16):
    sign = "-" if x < 0 else ""
    n = round(abs(x) * den); whole, rem = divmod(n, den)
    if rem == 0:
        return f"{sign}{whole} in"
    g = gcd(rem, den)
    return f"{sign}{whole} {rem // g}/{den // g} in" if whole else f"{sign}{rem // g}/{den // g} in"

def show(x):
    x = 0.0 if abs(x) < 1e-6 else x
    return f"{x:,.0f} mm" if MODE == "mm" else frac(x)
D, t, sf = 1800, 16, 50      # inside diameter, thickness, straight flange
Dm = D + t                     # work on the mean surface
a = Dm / 2
def spheroid_half(a, c):       # surface area of half an oblate spheroid (c < a)
    e = math.sqrt(1 - (c / a) ** 2)
    return math.pi * a * a * (1 + (1 - e * e) / e * math.atanh(e))
heads = {}
heads["2:1 ellipsoidal"] = (D / 4, spheroid_half(a, a / 2))
heads["hemispherical"] = (D / 2, 2 * math.pi * a * a)
# torispherical (ASME F&D): crown radius L = outside diameter, knuckle r = 6 % of it
L, rk = D + 2 * t, 0.06 * (D + 2 * t)
dep = L - math.sqrt((L - rk) ** 2 - (D / 2 - rk) ** 2)
heads["F&D (6 % knuckle)"] = (dep, None)
for name, (depth, area) in heads.items():
    line = f"{name:18} inside depth {show(depth)}"
    if area:
        blank = math.sqrt(4 * (area + math.pi * Dm * sf) / math.pi)
        line += f"  blank about {show(blank)} before trim"
    print(line)
# a nozzle at radius x on the 2:1 head: height of the head surface there, and its slope
x = 500
z = (D / 4) * math.sqrt(1 - (x / (D / 2)) ** 2)
slope = math.degrees(math.atan((D / 4) * x / ((D / 2) ** 2 * math.sqrt(1 - (x / (D / 2)) ** 2))))
print(f"at {show(x)} from the centre the head is {show(z)} above the tangent line, sloping {slope:.1f} deg")2:1 ellipsoidal inside depth 450 mm blank about 2,217 mm before trim hemispherical inside depth 900 mm blank about 2,638 mm before trim F&D (6 % knuckle) inside depth 302 mm at 500 mm from the centre the head is 374 mm above the tangent line, sloping 18.5 deg
The ellipsoidal head's inside depth is exactly a quarter of the diameter, and the flanged and dished head would be about two-thirds of that. The blank estimate for the 2:1 head is about 1.2 times the head's outside diameter, close to the figure the head maker quoted. The last line gives Kiera what she needs for the vapour outlet: at 500 mm (20 in) out, the head surface is 374 mm (14 15/16 in) above the tangent line and slopes about 18.5 degrees, so a nozzle parallel to the vessel's axis there will need a neck cut on an 18.5 degree slope, longer on the side toward the centre.
Worked problem
Height of a 2:1 head at a given radius
On a 2:1 ellipsoidal head with an inside diameter of 1,800 mm (72 in), how high is the inside surface above the tangent line at 700 mm (28 in) from the centre?
Show solution
- The ellipse's semi-axes are 900 mm (36 in) across and 450 mm (18 in) deep.
- Height = depth × √(1 − (radius ÷ semi-axis)²) = 450 × √(1 − (700 ÷ 900)²) (18 × √(1 − (28 ÷ 36)²)).
- = 450 × 0.629 = 283 mm (18 × 0.629 = 11 5/16 in).
Answer: The surface is 283 mm (11 5/16 in) above the tangent line at that radius.
Receiving inspection
Harjit and Kiera check V-414's heads before they are accepted. The marking on each head must match its paperwork: material, heat number, head maker's serial number and, for a code head, the head maker's stamp. The minimum thickness report must show every reading at or above the design minimum. Then the shape and size. The head's circumference at the edge is measured with a tape and compared with the shell's; the diameter is measured in several directions to check roundness; the straight flange is checked for length and for being square to the tangent plane; and the knuckle and crown are checked with a template cut to the head's profile, which shows any flat spots or bulges. The depth is measured with a straightedge across the edge and a rule to the inside of the crown.
Code rules limit how far a formed head may depart from its specified shape, measured with templates, and require the inside surface to stay within a tolerance of the design shape. Joanne keeps a set of profile templates for the shop's most common head sizes; for a new size, she draws one from the head maker's drawing and cuts it from thin sheet metal.
| Check | Method | What it catches |
|---|---|---|
| Markings and paperwork | Compare stamping with certificates and report | Wrong material or head |
| Minimum thickness | Head maker's report; spot readings with an ultrasonic gauge | Thinning in the knuckle or crown |
| Edge circumference and roundness | Tape around the edge; diameters in several directions | A head that will not match the shell |
| Straight flange | Rule and square | Short or flared flange |
| Profile | Template to the design shape | Flat spots, bulges, wrong shape |
| Depth | Straightedge and rule | Wrong head type or proportion |
Finding points on a formed head
Marking a head is done on the formed head, upright on a level table. The centre is found with a centre finder, or by measuring diameters across the edge and marking where they cross. The orientation lines are scribed from the centre to the edge, matched to the shell's 0 degree line. A point at a given radius is found in plan, by measuring horizontally from the centre with a level and a square, or along the surface, which is longer; the drawing says which, and on most vessel drawings a head nozzle's position is given in plan, as a horizontal distance from the vessel's axis.
For a nozzle at a given radius, the head's height and slope at that radius, from the formulas behind Kiera's code, tell her how to cut the neck: the neck lines on the side toward the centre are longer, those toward the edge shorter, and the difference across the nozzle is about its diameter times the tangent of the slope. On the vapour outlet, an NPS 8 nozzle at an 18.5 degree slope, that difference is about 73 mm (2 7/8 in). She develops the neck pattern by the parallel-line method, with each line's length to the head surface found from the head's height at that line's radius.
Common mistakes
MistakeTreating the nominal plate thickness as the head's thickness.
InsteadUse the head maker's certified minimum thickness after forming.
MistakeOrdering a head to the inside diameter without checking the outside fit.
InsteadCompare the head's expected outside diameter with the shell's, especially if their thicknesses differ.
MistakeAccepting a head on its paperwork alone.
InsteadCheck markings, thickness, circumference, roundness, straight flange and profile on arrival.
MistakeMeasuring a head nozzle's position along the surface when the drawing gives it in plan.
InsteadCheck how the drawing dimensions it; most give plan distances from the axis.
MistakeCutting an off-centre head nozzle's neck square.
InsteadCut it to the head's slope at that radius.
Summary and key terms
- Heads curve in two directions and are formed by head makers by pressing, spinning or segments.
- A 2:1 ellipsoidal head is a quarter of its diameter deep; a hemispherical head half; an ASME flanged and dished head about 0.17.
- A head order gives type, diameter basis, minimum formed thickness, material, straight flange, edge preparation and certification.
- Blank size is the head maker's figure; an area estimate gives about 1.2 times the diameter for a 2:1 head.
- Heads are inspected on arrival for markings, thickness, circumference, roundness, straight flange and profile.
- Points and nozzles are marked on the formed head; the head's height and slope set the neck cut.
- Straight flange
- The short cylindrical band at a head's edge, between the tangent line and the edge.
- Tangent line
- The line where a head's curved surface meets its straight flange.
- Knuckle
- The tightly curved band joining a torispherical head's crown to its straight flange.
- Crown radius
- The radius of the spherical centre part of a torispherical head.
- Blank
- The flat plate a head maker forms into a head.
- Minimum thickness after forming
- The thinnest point of a formed head, certified by the head maker.
Practice problems
Work each problem on paper first, then reveal the answer to check.
What is the inside depth of a 2:1 ellipsoidal head with an inside diameter of 2,400 mm (96 in)?
Show answer
A quarter of the diameter: 600 mm.
Why do heads have a straight flange?
Show answer
To move the head-to-shell weld away from the knuckle, where stresses from the change of shape are highest.
For a standard ASME flanged and dished head, what are the crown and knuckle radii?
Show answer
The crown radius equals the outside diameter; the knuckle radius is 6 percent of it.
Why must an off-centre head nozzle's neck be cut on a slope?
Show answer
The head surface slopes at that radius, so the neck lines on the side toward the centre are longer.
Lesson quiz · 5 questions
Score 60% or more to complete this lesson.
Create a free account to save your progress, take quizzes and earn a certificate.