
WLD-210 · Lesson 3 of 12 · 17 min
Wire electrodes and classifications
Every spool of wire on Hartwell's rack carries a label with a string of letters and numbers. Like the classification on a stick electrode box, that string is a promise: if the wire is used with the stated gas and polarity, the weld metal will meet stated strength, toughness, chemistry and usability requirements. Lucia Ferreira will not let a spool into the structural bay unless its classification matches the welding procedure for the job, and Devon learns why when he picks up a spool of self-shielded wire by mistake for a gas-shielded procedure on the Riverside girders. This lesson explains the three kinds of steel wire, what is in them, how they are classified in Canada and the United States, and how to store and handle them so that the label stays true.
Three kinds of wire
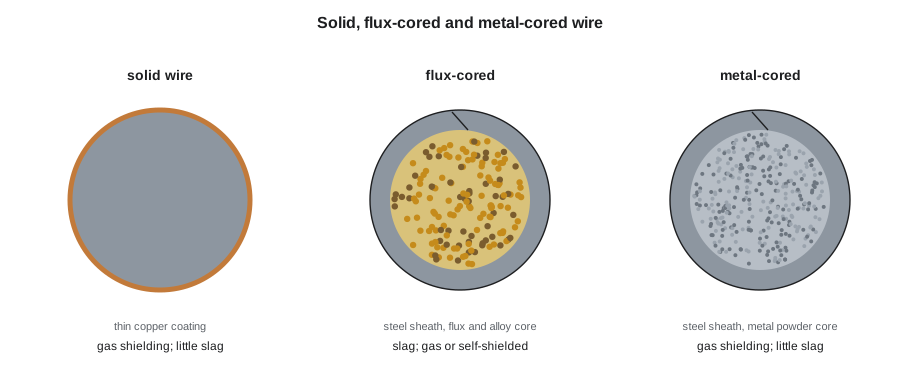
Solid wire is drawn steel, usually with a thin copper coating that improves electrical contact in the tip, slows rusting and lubricates feeding. Its chemistry is simple: carbon steel with controlled manganese and silicon, the deoxidizers that tie up oxygen from the shielding gas and from rust and mill scale so that the weld is sound. Wires with more deoxidizer, such as the common grade 6 wires, tolerate dirty and scaled steel better and give a more fluid pool; wires with less, such as grade 3, give a slightly stiffer pool and are used on clean steel.
Flux-cored wire is a tube. A strip of steel is formed into a U, filled with a measured powder of flux minerals, alloys and deoxidizers, closed into a tube and drawn down to size. The core makes up roughly 15 to 30 percent of the wire's mass. Rutile-based cores, in the common all-position gas-shielded wires, make a fast-freezing slag that holds the pool up in vertical and overhead welding and peels off easily. Basic cores, with fluorides and lime, make tougher, lower-hydrogen weld metal at the cost of a less pleasant arc. Self-shielded cores add gas formers and strong deoxidizers and nitride formers such as aluminum, which protect the weld from the nitrogen in the air.
Metal-cored wire is also a tube, but its core is mainly iron powder with alloys and deoxidizers and only a small amount of arc stabilizers. With shielding gas, it gives a broad, deep arc, high deposition and only small silicate islands on the bead, like solid wire.
Strength, position and usability
Whatever the system, a carbon steel wire classification tells the welder four things: the minimum tensile strength of the weld metal, the positions the wire is designed for, its usability (the type of core or the shielding and polarity it runs with), and its toughness and chemistry. Optional designators add a diffusible hydrogen limit and sometimes improved toughness. The usability numbers for flux-cored wires mean the same thing in both countries, because the Canadian and American systems share their roots:
| Usability | Shielding | Polarity | Typical use |
|---|---|---|---|
| T1 | Gas (carbon dioxide or argon mix) | DCEP | All-position rutile wires, structural work |
| T5 | Gas | DCEP | Basic slag, low hydrogen, tough; mostly flat and horizontal |
| T4 | None (self-shielded) | DCEP | High deposition, shallow; flat and horizontal |
| T7 | None | DCEN | High deposition, flat and horizontal |
| T8 | None | DCEN | All-position, good toughness; structural field work |
| T11 | None | DCEN | General purpose; often limited in plate thickness |
| T15 (or C) | Gas | DCEP | Metal-cored |
Classifications in your country
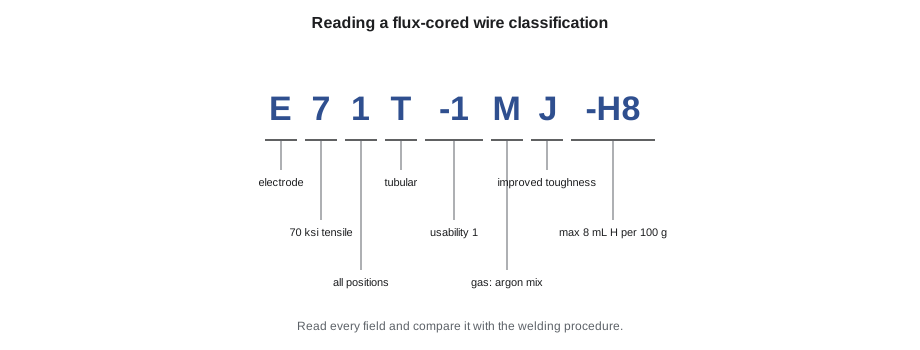
In the United States, carbon steel solid and metal-cored wires are classified to AWS A5.18 and carbon steel flux-cored wires to AWS A5.20; low-alloy wires are covered by A5.28 and A5.29. A solid wire is named like ER70S-6: ER for a wire that can be an electrode or a rod; 70 for a minimum tensile strength of 70 ksi; S for solid; 6 for the composition group, here the high-silicon, high-manganese wire that tolerates mill scale. A metal-cored wire is named like E70C-6M, with C for composite (metal-cored) and M for an argon mix. A flux-cored wire is named like E71T-1C-H8: E for electrode; 7 for 70 ksi tensile; 1 for all positions (0 means flat and horizontal only); T for tubular; 1 for the usability; C for carbon dioxide shielding (M means argon with 75 to 80 percent argon and the balance carbon dioxide); and H8 for no more than 8 mL of diffusible hydrogen per 100 g of weld metal. A J after the gas letter marks improved low-temperature toughness. For some years AWS also published an open classification, A5.36, which spelled every property out in a long code such as E71T1-M21A2-CS1-H8. AWS has since withdrawn A5.36, and the 2025 edition of the structural code, D1.1, refers to the A5.18, A5.20, A5.28 and A5.29 classifications instead; the long A5.36 names still appear on older procedures and some labels.
# Decode AWS wire classifications (A5.18 solid and metal-cored, A5.20 flux-cored)
import re
def decode(c):
    m = re.match(r"ER(\d\d)S-(\d+)\Z", c)
    if m:
        return f"{c}: solid wire, {m.group(1)} ksi minimum tensile, deoxidizer group {m.group(2)}"
    m = re.match(r"E(\d\d)C-(\d+)([CM]?)\Z", c)
    if m:
        gas = {"C": "carbon dioxide", "M": "argon mix", "": "as stated by maker"}[m.group(3)]
        return f"{c}: metal-cored wire, {m.group(1)} ksi tensile, composition {m.group(2)}, gas {gas}"
    m = re.match(r"E(\d)(\d)T-(\d+)([CM]?)(J?)(?:-H(\d+))?\Z", c)
    if m:
        ts, pos, use, gas, j, h = m.groups()
        g = {"C": "carbon dioxide", "M": "argon-carbon dioxide mix", "": "none (self-shielded) or as stated"}[gas]
        out = (f"{c}: flux-cored, {int(ts) * 10} ksi tensile, "
               f"{'all positions' if pos == '1' else 'flat and horizontal'}, usability {use}, gas: {g}")
        if j:
            out += ", improved toughness (J)"
        if h:
            out += f", diffusible hydrogen H{h}"
        return out
    return f"{c}: not recognized"
for c in ["ER70S-6", "E70C-6M", "E71T-1C-H8", "E71T-1MJ-H8", "E71T-8", "E70T-4"]:
print(decode(c))ER70S-6: solid wire, 70 ksi minimum tensile, deoxidizer group 6 E70C-6M: metal-cored wire, 70 ksi tensile, composition 6, gas argon mix E71T-1C-H8: flux-cored, 70 ksi tensile, all positions, usability 1, gas: carbon dioxide, diffusible hydrogen H8 E71T-1MJ-H8: flux-cored, 70 ksi tensile, all positions, usability 1, gas: argon-carbon dioxide mix, improved toughness (J), diffusible hydrogen H8 E71T-8: flux-cored, 70 ksi tensile, all positions, usability 8, gas: none (self-shielded) or as stated E70T-4: flux-cored, 70 ksi tensile, flat and horizontal, usability 4, gas: none (self-shielded) or as stated
The decoder is a simplified illustration; the full classification rules have more groups, and the specification and the label always govern. The important habit is to read every field and compare it with the procedure, not just the first few characters. Two wires that both start with the same strength and position numbers can need different gases and polarities.
What the procedure controls
A welding procedure specification names the filler metal by its classification, and for some codes and jobs by brand and trade name as well. On prequalified structural work, the code lists which classifications match which base metals. On the Riverside girders, the bridge specification adds requirements: weld metal toughness at a stated low temperature, a diffusible hydrogen limit, and in some cases testing of each wire lot. Changing to a wire with a different classification, a different gas, or even a different brand on some procedures, can mean requalifying. Lucia's rule for the floor is simple: the label on the spool, the gas on the cylinder and the WPS on the wall must agree before the trigger is pulled.
Wire diameter is part of the procedure too. Common diameters for structural steel are 0.035 in for sheet, 0.045 in for most plate work, 0.052 in and 1/16 in for heavy flat and horizontal welding, and larger self-shielded wires for high-deposition field welding. A larger wire carries more current and deposits more metal, but needs more current to run in the right transfer mode and is harder to control out of position.
Stainless, aluminum and other wires
The same equipment welds other metals with different wires. Stainless steel solid wires such as ER308LSi and ER316LSi, with extra silicon for better wetting, are used in the pressure bay with argon-rich gases, and stainless flux-cored wires such as E308LT1 are popular for out-of-position stainless work. Aluminum wires such as ER4043 and ER5356 are soft and need U-groove rolls, plastic liners and push-pull or spool guns. Hard-facing wires, nickel alloy wires and low-alloy wires for weathering steel and chromium-molybdenum steel all have their own classifications. The gas tungsten arc welding and pipe welding courses deal with stainless and aluminum in more detail; in this course, the wires are carbon steel unless stated.
Weathering steel and matching wire
The Riverside girders are weathering steel, which forms a tight rust layer that protects it and is left unpainted. For welds that will be exposed, the weld metal must weather the same way, which needs small amounts of nickel, copper or chromium. Bridge specifications allow ordinary carbon steel wire for small single-pass welds, where dilution with the base metal brings in enough alloy, but call for a low-alloy wire with a nickel or similar chemistry suffix for multipass exposed welds. Lucia's weld map for the girders marks which welds need which wire.
Storing and handling wire
Wire that is perfect on the label can still make bad welds if it is mishandled:
- Keep spools in their sealed bags and boxes until they are used, and store them in a dry, heated area. Wire that is colder than the shop air sweats when it is brought out, and water on the wire becomes hydrogen and porosity in the weld.
- Flux-cored wire can pick up moisture through the seam of the tube. Wires with a low hydrogen designator are made to resist moisture pick-up, but they are still kept sealed, and partly used spools are put back in a bag or a heated cabinet at the end of the shift.
- Rust on solid wire causes porosity and poor feeding; rusty wire is scrapped, not wiped.
- Do not drop spools; a dented spool flange catches the wire and a kinked wire jams the liner.
- Keep stainless and aluminum wire away from carbon steel to avoid contamination, and keep each one with its own liner and rolls.
- Label partly used spools with the classification if the original label is lost. An unlabeled spool goes to the scrap bin, not the welding booth.
Bulk drums holding hundreds of kilograms or pounds of wire feed carriages and robots with fewer changeovers. They need a drum hood and conduit to the feeder, and the drum is kept covered and dry like a spool.
# How long does a spool last? Wire use per hour at a given wire speed
import math
diameter = 0.045             # wire diameter, in
density = 0.284            # lb/in3
fill = 1.0                 # solid wire; tubular wires weigh less per length
wfs = 315                # wire feed speed, in/min
spool = 33               # spool mass, lb
area = math.pi * diameter ** 2 / 4
mass_per_length = area * density * fill * 1     # lb per in
use_per_hour = mass_per_length * wfs * 60
print(f"wire mass: {mass_per_length:.4f} lb per in")
print(f"at {wfs} in/min the arc uses {use_per_hour:.1f} lb per arc hour")
print(f"a {spool} lb spool lasts about {spool / use_per_hour:.1f} arc hours")wire mass: 0.0005 lb per in at 315 in/min the arc uses 8.5 lb per arc hour a 33 lb spool lasts about 3.9 arc hours
A tubular wire weighs less per length than a solid wire of the same diameter, because its core is less dense than solid steel, so the spool goes further in length but deposits less per meter or foot. The next lessons use these numbers to compare deposition rates.
Certificates and traceability
Every lot of wire comes with documents. The manufacturer's certificate of conformance states that the wire meets its classification, and for code work many specifications call for a test report showing the actual results of the chemical analysis and the weld metal tests for that lot or for the product type. On the Riverside girders, the specification requires lot traceability for the flux-cored wire: each spool's lot number is recorded on the weld map against the welds it was used for, and the matching certificate is kept in the quality file. Devon learns to copy the lot number from the spool label into his log when he loads a new spool, before the label gets dirty or torn. If a test later shows a problem with a lot, the shop can find every weld made with it. A spool with no lot number, or one that does not match a certificate on file, is set aside until Lucia has checked it.
Common mistakes
MistakeReading only the first part of the classification.
InsteadRead every field: gas, polarity, toughness and hydrogen all matter.
MistakeUsing an argon-mix wire with carbon dioxide because the cylinder was handy.
InsteadThe classification states the gas; changing it changes the weld metal.
MistakeLeaving flux-cored wire on the feeder in an unheated shop over the weekend.
InsteadBag partly used spools or store them in a cabinet.
MistakeWiping rust off a solid wire and using it.
InsteadScrap rusty wire; it causes porosity and feeding problems.
MistakeAssuming a wire that matches strength also matches weathering steel.
InsteadExposed multipass welds may need a low-alloy weathering wire.
Summary and key terms
- Steel wires are solid, flux-cored or metal-cored.
- Deoxidizers such as manganese and silicon make welds sound on scaled or dirty steel.
- Flux-cored cores make slag and alloy the weld; self-shielded cores also make gas and tie up nitrogen.
- A classification states strength, position, usability, shielding, toughness, chemistry and hydrogen.
- The wire, gas and polarity must all match the welding procedure.
- Wire must be stored dry and sealed, and partly used flux-cored spools protected from moisture.
- Deoxidizer
- An element such as manganese or silicon added to remove oxygen from the weld pool.
- Flux-cored wire
- A tubular wire with a core of flux minerals, alloys and deoxidizers.
- Metal-cored wire
- A tubular wire with a core that is mainly metal powder.
- Usability
- The part of a classification that describes the wire type, shielding, polarity and operating behavior.
- Diffusible hydrogen designator
- An optional designator such as H8 that limits hydrogen in the weld metal.
- Weathering steel
- A low-alloy steel that forms a protective rust layer and is used unpainted.
Practice problems
Work each problem on paper first, then reveal the answer to check.
What does the C mean in E71T-1C-H8?
Show answer
Carbon dioxide shielding gas.
What does the 0 mean in E70T-4?
Show answer
Flat and horizontal positions only.
A 0.045 in solid wire feeds at 315 in/min. About how much wire is used per arc hour?
Show answer
About 0.00045 lb per inch × 315 × 60 ≈ 8.5 lb.
Lesson quiz · 5 questions
Score 60% or more to complete this lesson.
Create a free account to save your progress, take quizzes and earn a certificate.